
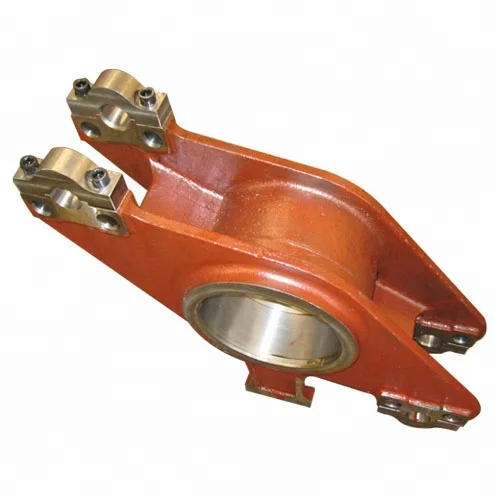
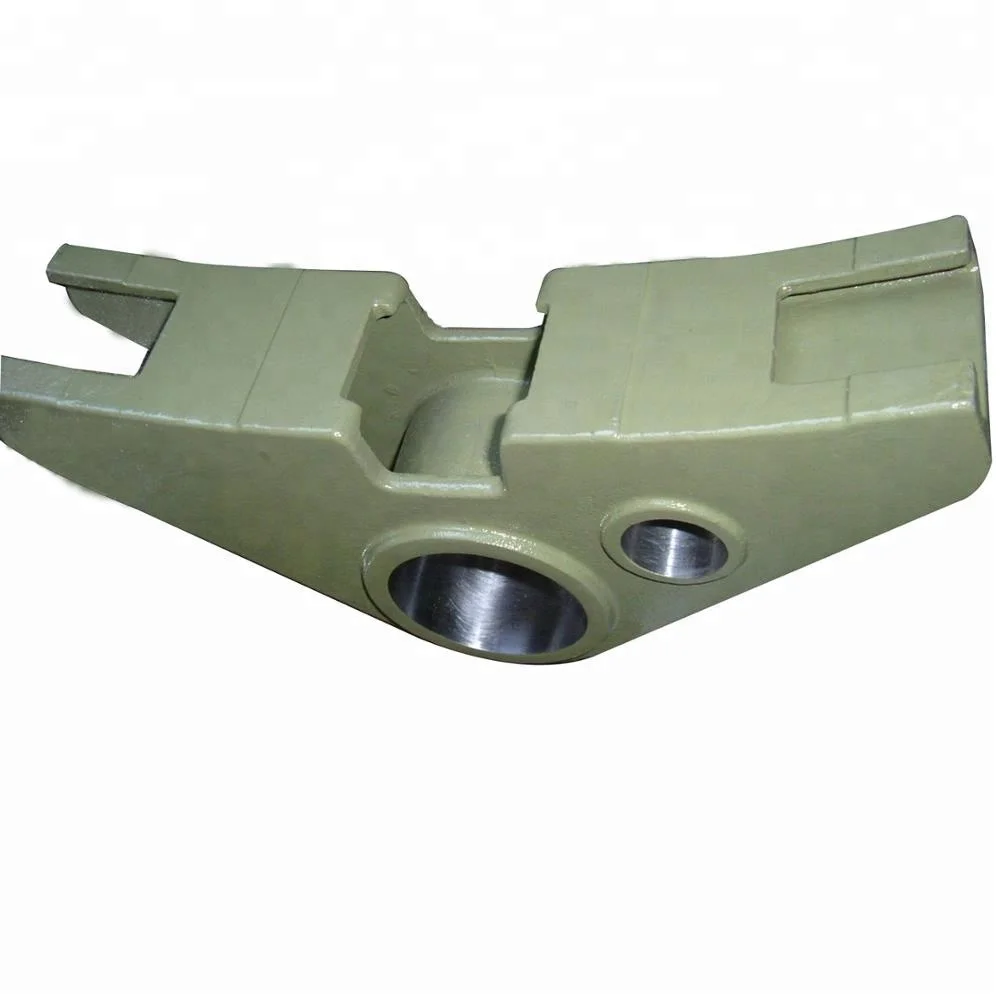
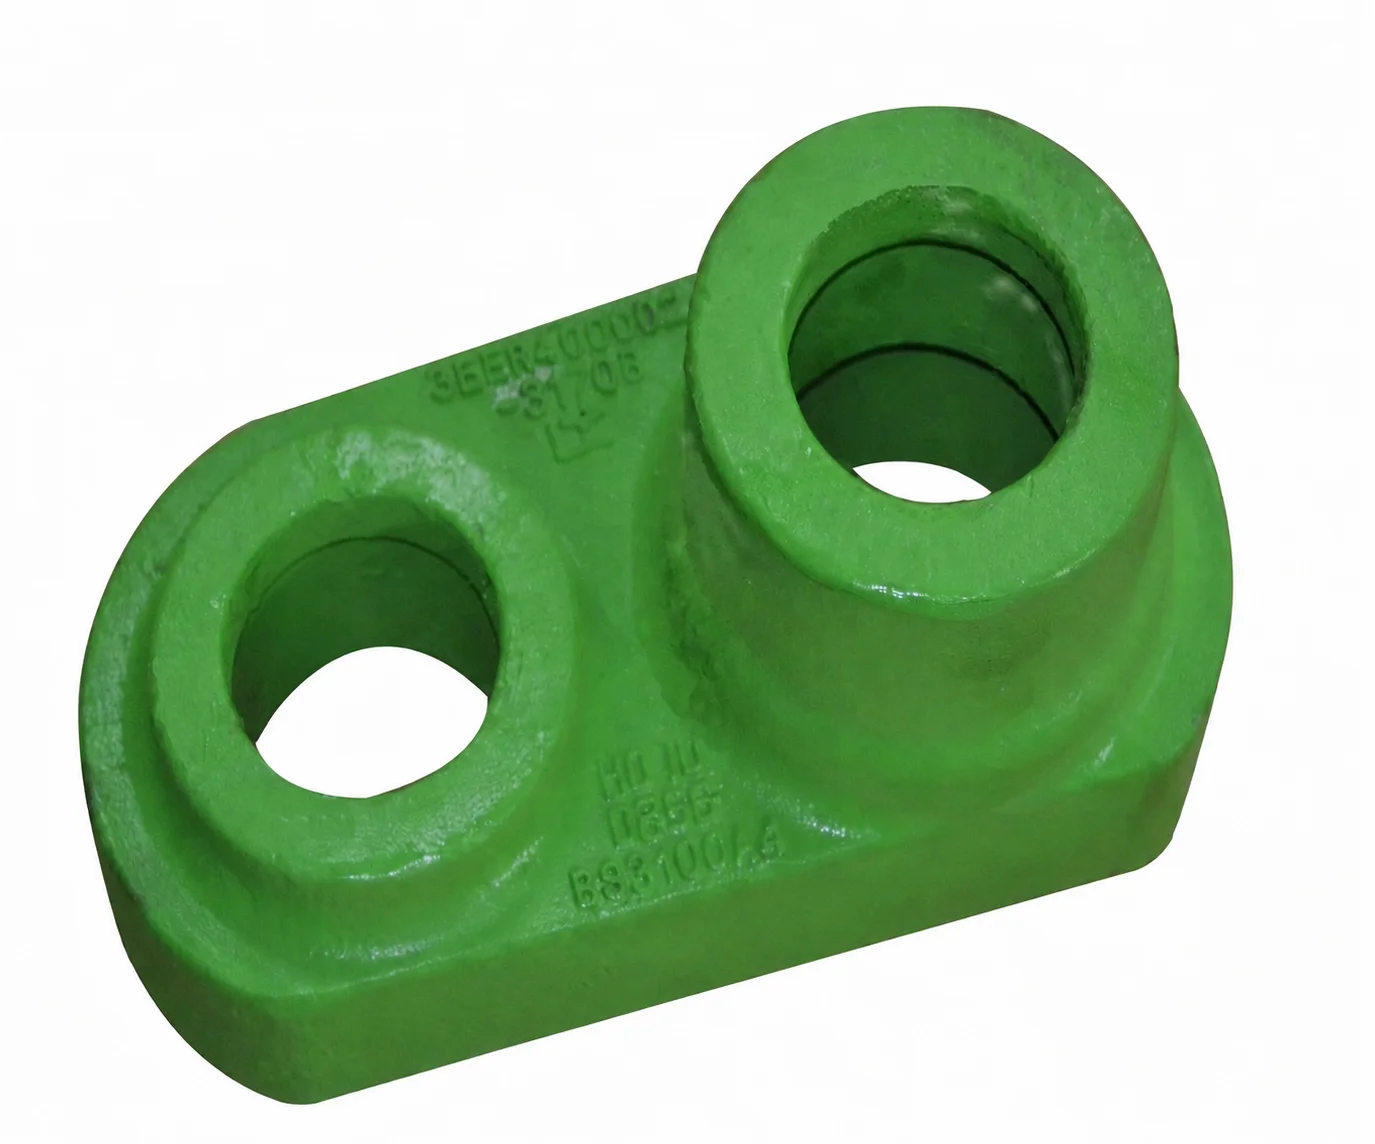
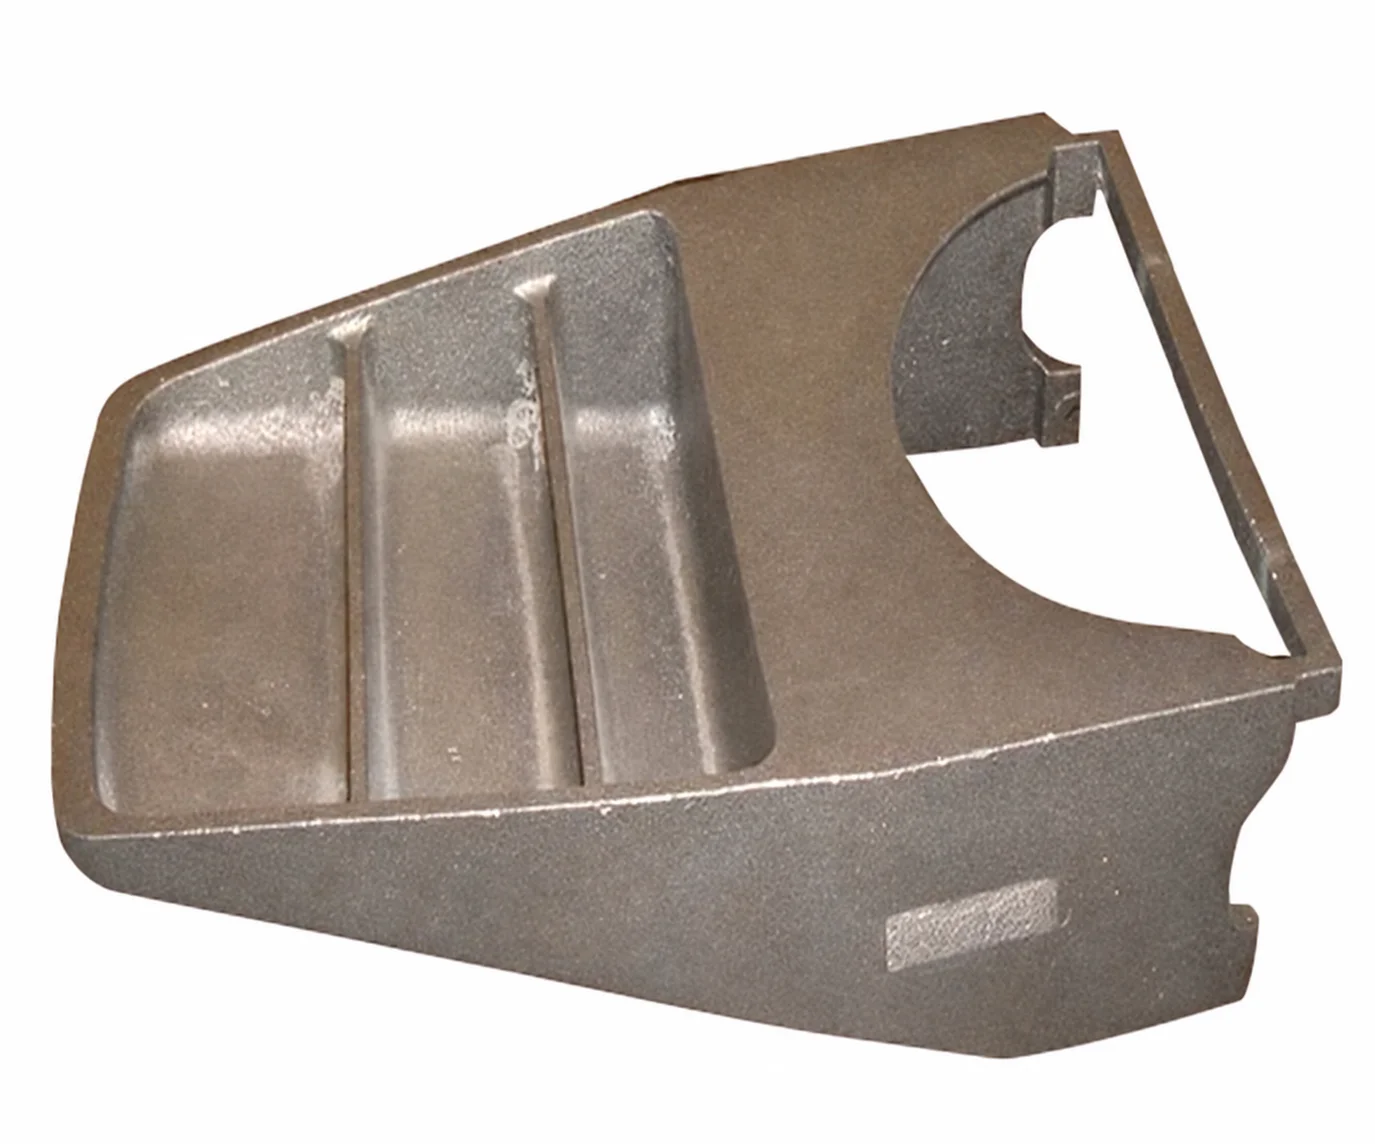
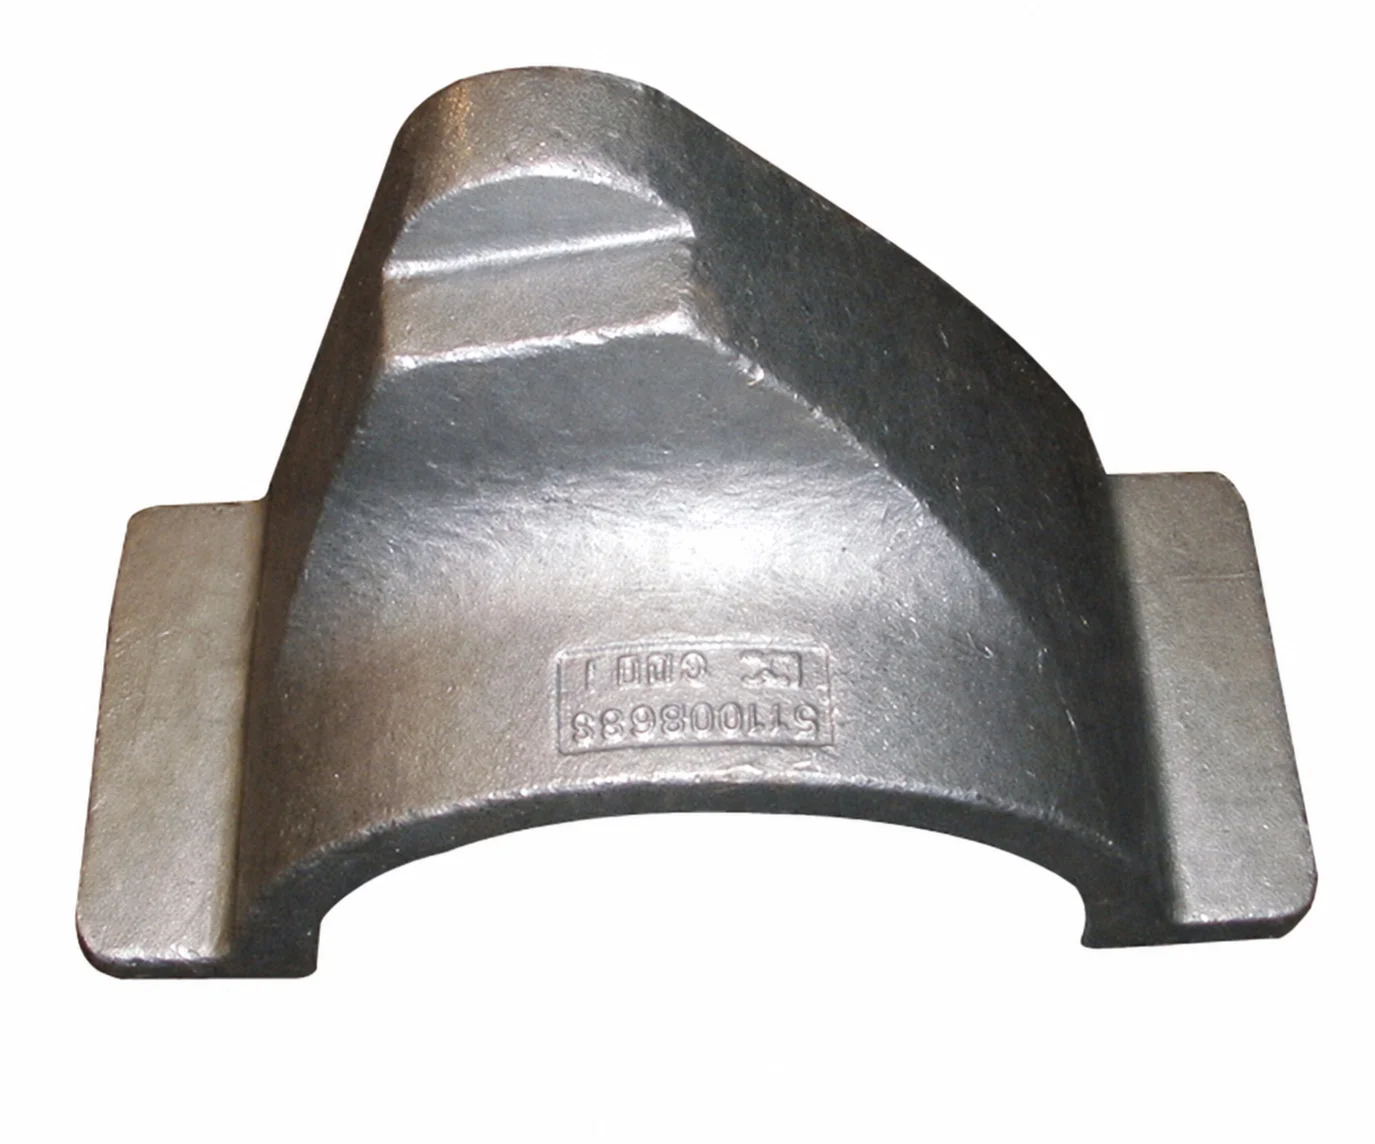
Steel Lost Wax Investment CNC Castings, Quench and Temper, Shot Blasting/Assembly, 100% Visual/Gage Inspection
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishShot Blasted
-
MaterialSteel
-
NameProfessional lost wax metal steel casting foundryKeywordsCasting foundry
-
ProcessLost wax investment casting+CNC machinedHeat TreatmentQuench and temper by 2 set mesh belt furnaces
-
Surface TreatmentShot blasting+AssemblingMachining Facility60+ Machining centers,70+ CNC machines
-
InspectionMT/UT/RT/100% visual+100%gage/CMMStandardASTM. AISI. DIN. BS. JIS. NF. AS.
-
CertificationIATF16949/ISO14001
Steel lost wax investment castings combine CNC machining with quench-and-temper treatment, shot blasting and assembly. Inspection includes 100% visual and 100% gage inspection, alongside MT, UT, RT and CMM methods whose actual coverage is agreed for the job. Select the steel specification and component geometry before allocating these operations.
Heat condition and machining requirements
The heat-treatment direction is quench and temper using two mesh-belt furnaces. Machining references are 60+ machining centers and 70+ CNC machines, with actual facility and job allocation to confirm. Define the required heat-treated result and the cast or CNC-machined dimensions for the selected steel component.
Shot blasting and assembly scope
Establish the shot-blasted surface condition needed on the supplied part. Identify what is assembled, its mating arrangement and the acceptance criteria for the completed work. Keep those requirements connected to the drawing and final component condition.
Visual, gage and selected test coverage
Full visual and gage inspection are distinct from the MT, UT, RT and CMM method choices. Specify the actual characteristics and coverage for each selected method, together with accepted procedures and records. That allocation defines how the chosen steel job is evaluated without treating every method as a full-coverage requirement.
Seven engineering families and management references
Engineering references cover ASTM, AISI, DIN, BS, JIS, NF and AS; agree the applicable documents, editions and material requirements. IATF16949 and ISO14001 are management-system references whose actual document, organization/site and current applicability need confirmation where required. Set quantity and manufacturing/assembly responsibilities around the accepted drawing, heat condition and inspection plan.








