
CUSTOM MANUFACTURING · PROJECT REVIEW
Die-Cast Aluminum Motor End Covers and Mounting Flanges
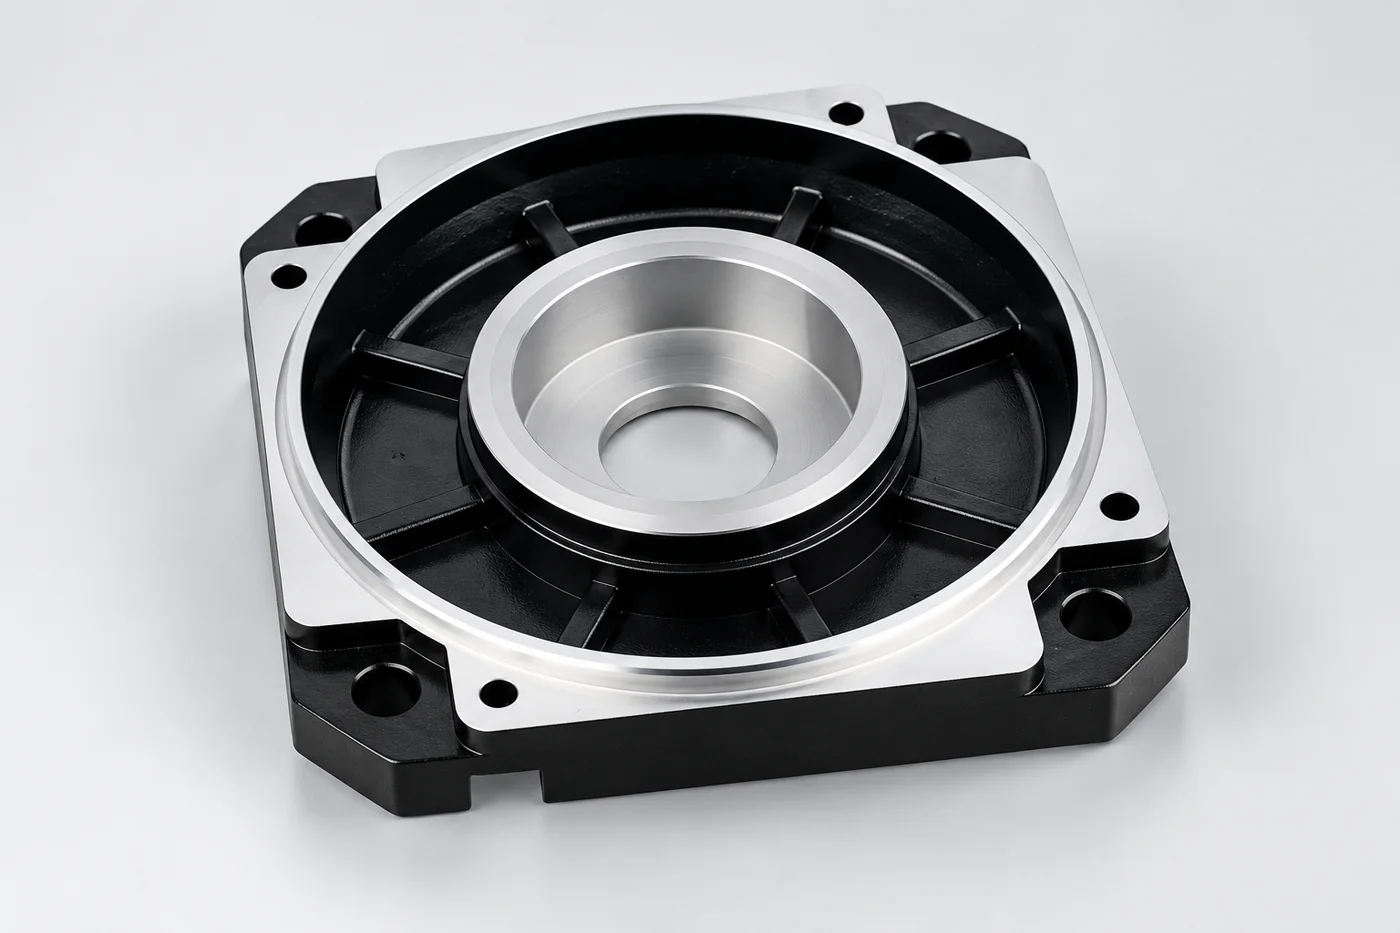
A motor end cover needs the correct bearing location, register and mounting pattern. Relia reviews the aluminium casting and finished interfaces with the adjoining housing, keeping coating and component identity in the same supply definition.
RELIA · PRODUCT AND MANUFACTURING SUPPORT
State the cover and flange scope clearly
Relia's end-cover reference lists aluminium alloy, customized dimensions, casting, deburring, drilling and threading. Relia's review links the cover to the mating housing and bearing arrangement. That keeps the mounting flange, register and shaft-clearance features connected as a functional part rather than a collection of unrelated hole sizes.
| Your requirement | Relia product and service scope |
|---|---|
| Material | Aluminium alloy |
| Listed route | Casting, deburring, drilling and threading |
| Functional features | Bearing pocket, pilot/register and mounting flange |
| Packing reference | Poly bag, inner box and carton |
02 · ALIGNMENT
Use the adjoining housing as an interface reference
- Housing reference
- Provide the mating register and mounting drawing.
- Finished cover
- Relate the pilot, face and holes to that interface.
The register, locating face and fastening holes need to correspond with the housing definition. Provide the relevant mating drawing and keep the revisions consistent. We can then review how the finished cover is positioned and checked, with the assembly relationship retained as the common technical reference.
Technical notes
Keep machining datums consistent between the bearing pocket and the mounting face. Review the cast bosses for drilling depth and tool access. Specify whether paint or another finish must be excluded from the register, bearing seat and electrical contact areas.
MANUFACTURING ROUTE · FEATURES AND CONTROL
Finish the Bearing Pocket and Register as One Interface
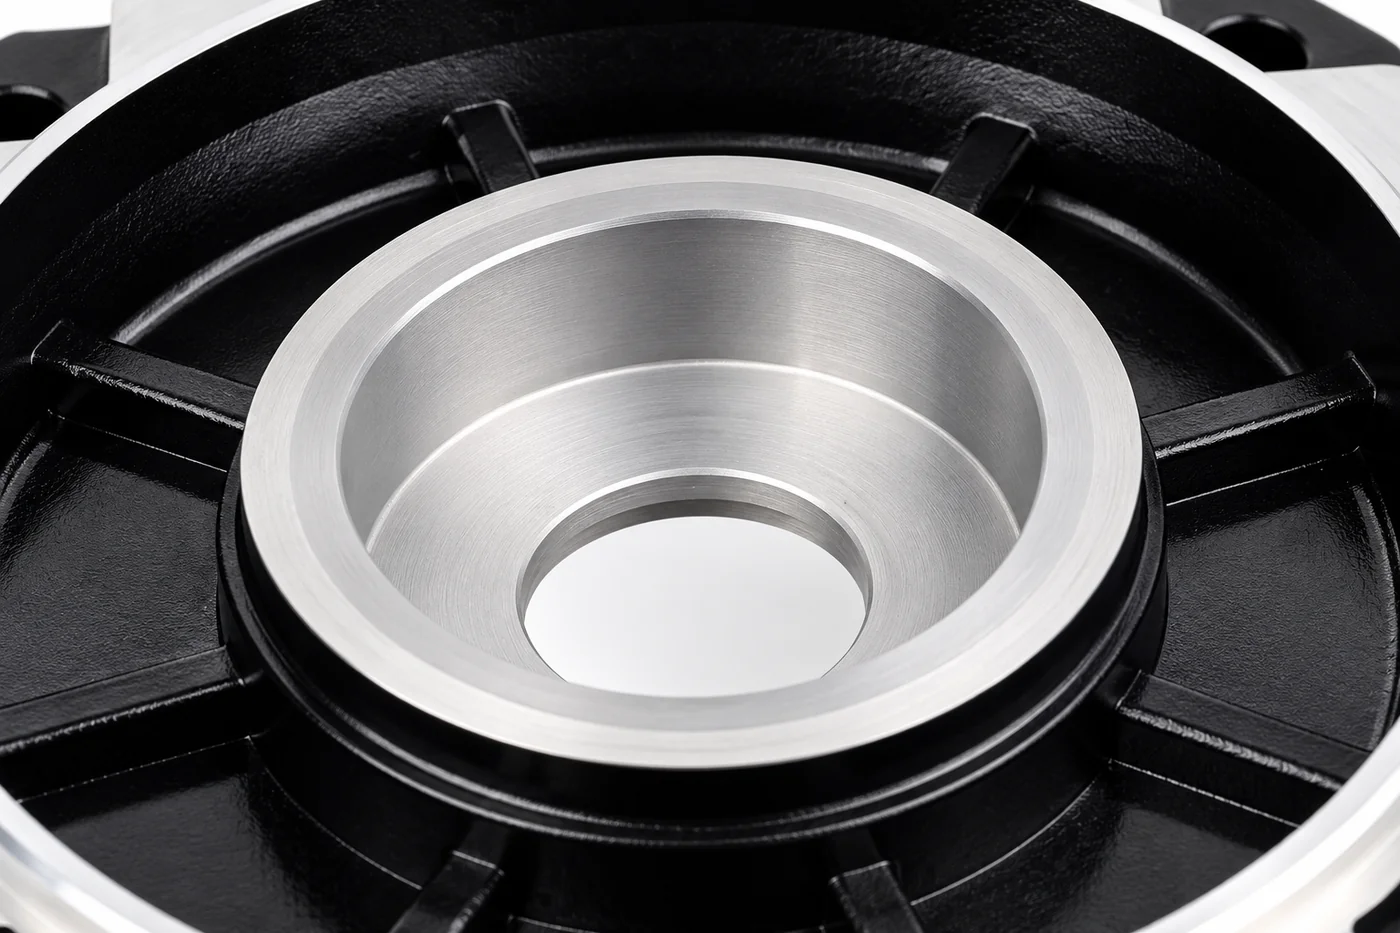
The casting provides the cover shape and fastening bosses. After trimming and deburring, machining establishes the pilot/register, bearing pocket, locating shoulder and mounting face where specified. Relia's datum review considers the relationship between these features, including the face and bore geometry needed by the assembly. Threads are cut with the required depth and access, and the finish plan preserves the controlled surfaces. The useful sample check combines dimensional results with the nominated bearing and mating housing.
- Cast the coverBody, flange and fastening bosses
- Machine locating featuresBearing pocket, shoulder and pilot
- Drill, thread and finishFastener interfaces and masked contact areas
- Review the assemblyBearing fit and housing/cover alignment
04 · SURFACE DEFINITION
Keep finish away from interfaces that need control
- Appearance reference
- Agree colour and visible surface condition.
- Controlled fit
- Define masking or coating allowance at mating features.
Agree the visible finish and any masking or coating allowance at the mating features. A colour reference does not define the final size of a register or bore. We review appearance and fit together, with the selected treatment and accepted visual reference tied to the component drawing.
05 · INSPECTION
Check the features used to locate and fasten the part
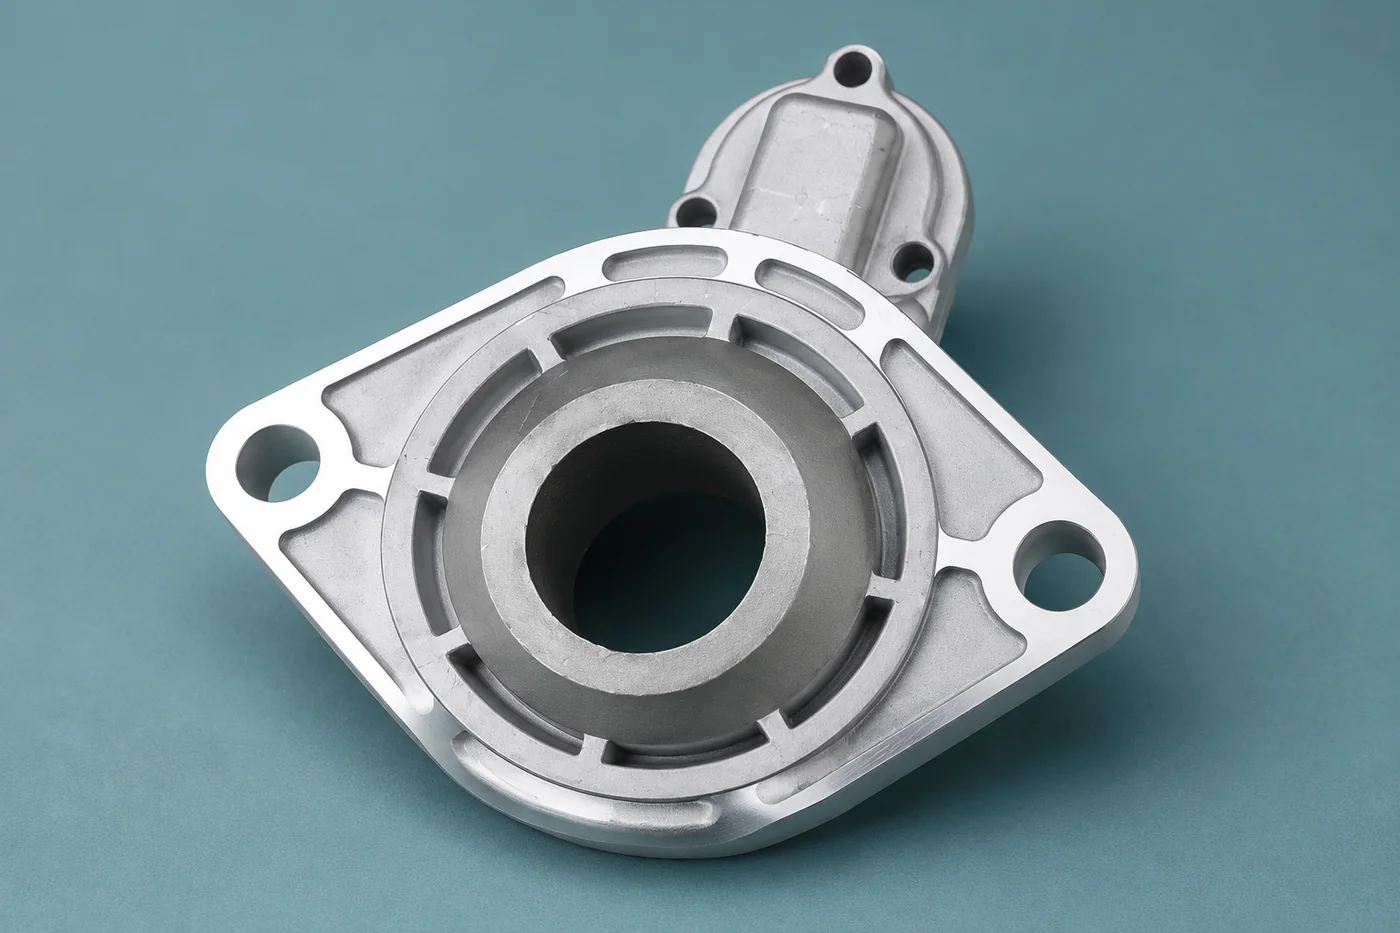
Inspect the bearing-seat size, axial shoulder position and face relationship after the relevant finishing operations. Use trial fit for the intended bearing and housing where required. Our end-cover description offers customized dimensions; it does not assign a motor power rating or a universal bearing fit.
| Feature | Useful acceptance basis |
|---|---|
| Register or bore | Specified fit and finished condition |
| End face | Datum and positional relationship |
| Fastening pattern | Hole, thread and location requirements |
| Trial fit | Accepted relationship to the mating housing |
06 · REPEAT PURCHASING
Retain identity across a supplied group
- Part identity
- Identify each cover or flange in the supplied set.
- Repeat consistency
- Keep drawing revisions and accepted finish references.
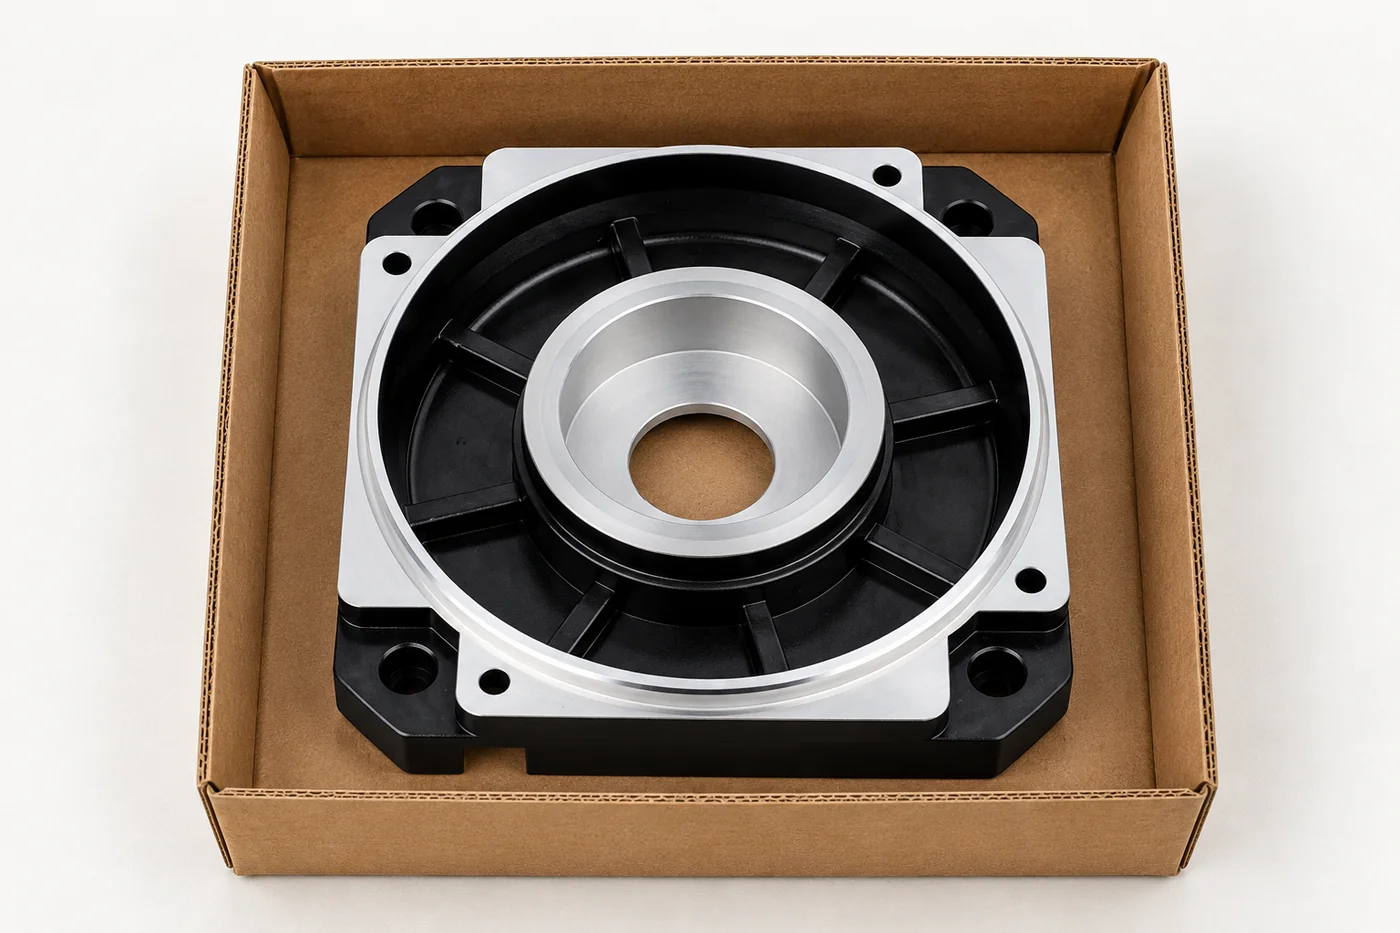
Where covers or flanges are supplied together, identify the part number and revision for each item. Keep the accepted appearance reference and any deviations with those records. This helps both teams request and receive the intended components again without relying on a shared product photograph alone.
07 · QUOTATION AND APPROVAL
Release the cover against a defined package
Bring the selected alloy, cast shape, machined interfaces and finish into one quotation scope. Keep required records and unresolved inputs visible. We can review the finished component with your purchasing and engineering teams before its manufacturing definition is released for the order.
Technical notes
Identify the bearing arrangement, locating shoulder, pilot diameter and mating housing. Add shaft-clearance and fastener requirements. A correct outside diameter does not establish rotor alignment when the bearing seat or mounting register is displaced.
RELIA · YOUR NEXT PROJECT
Send the cover drawing with its mating requirements
Share the part model, housing-interface drawing, material and quantities. State whether the enquiry is for a single cover or a defined component set, and include the finishing and acceptance records needed. We can review the cast and machined supply scope with you.
Start with these project details
- Cover model and housing interface
- Single item or component set
- Material, finish and quantities
- Required fit and acceptance records
Shuyuan Road, Qingdao, Shandong, China
