
CUSTOM MANUFACTURING · PROJECT REVIEW
Auxiliary Equipment for Defined Investment-Foundry Operations
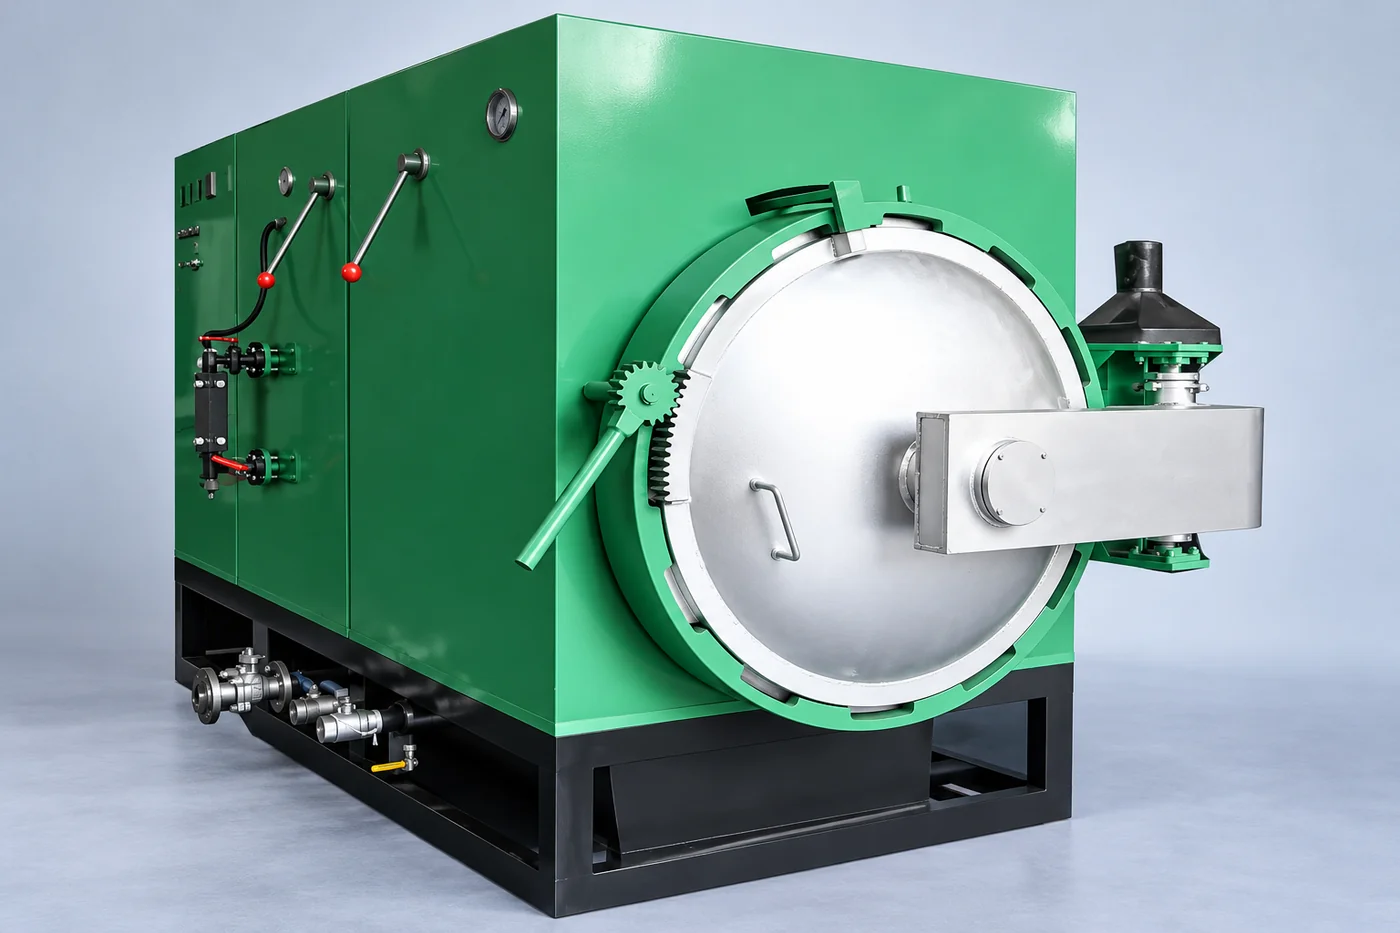
Foundry auxiliaries should be selected for a defined operation. Relia reviews dewaxing, shell-removal and mixing enquiries individually, using the pattern, workpiece or batch and available utilities to establish each unit's role in your workflow.
RELIA · PRODUCT AND MANUFACTURING SUPPORT
Identify the operation that needs equipment
Relia's auxiliary references include a 165°C dewaxing unit, pneumatic vibrating-shell equipment and a 7.5 kW mixing enquiry. Relia's configuration review keeps those functions distinct. The proposal connects the selected machine to shell-tree size, casting envelope or batch duty, instead of combining broad catalogue labels into an undefined foundry line.
| Your requirement | Relia product and service scope |
|---|---|
| Dewaxing reference | 165°C; 800–1,000 mm internal diameter options |
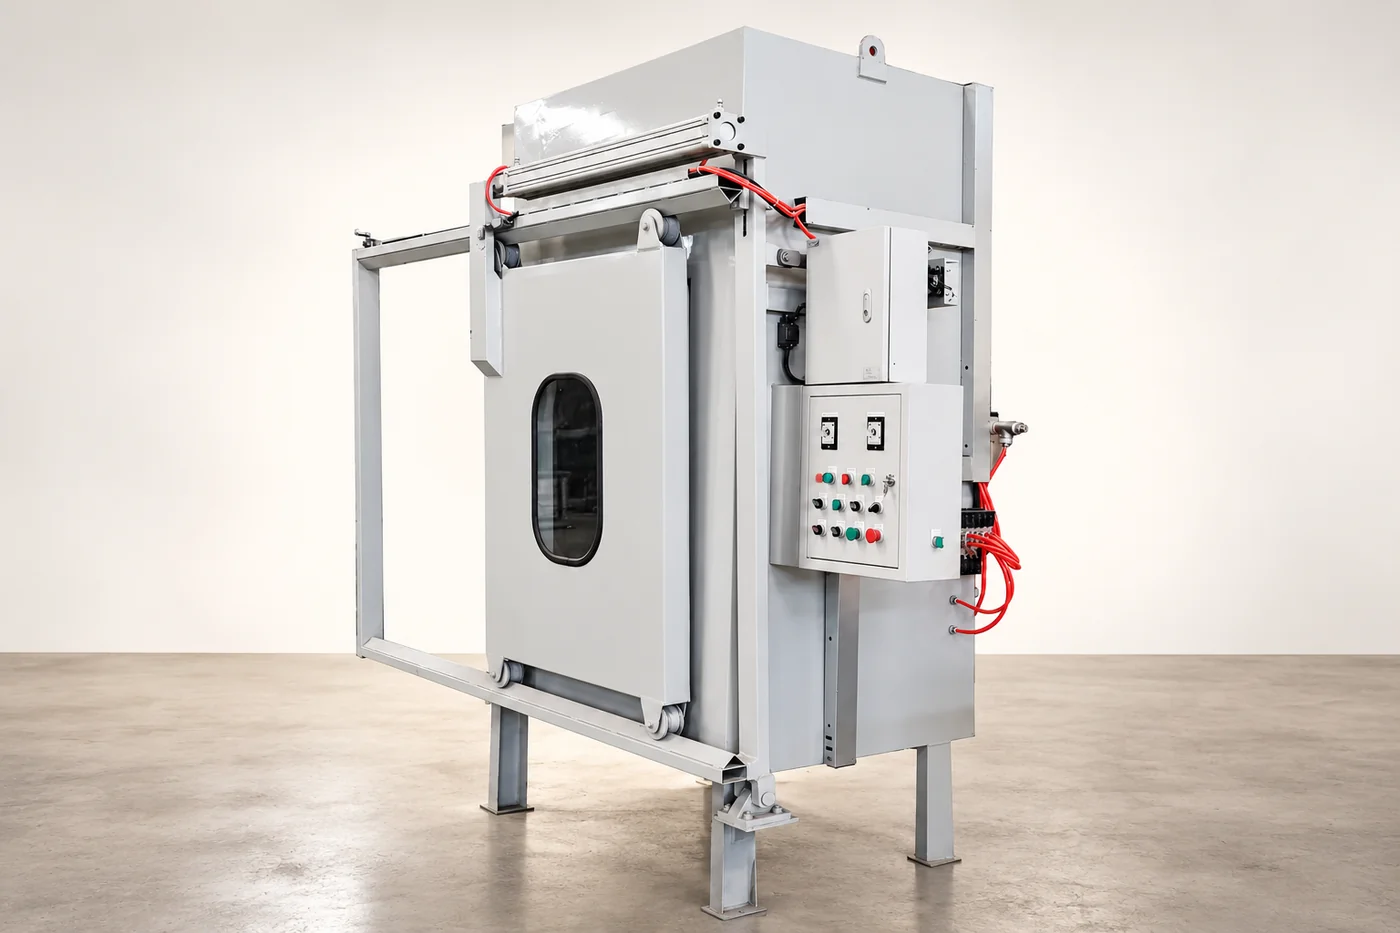
| Shell-removal reference | Pneumatic impact; 100 J and 1,050/min listed |
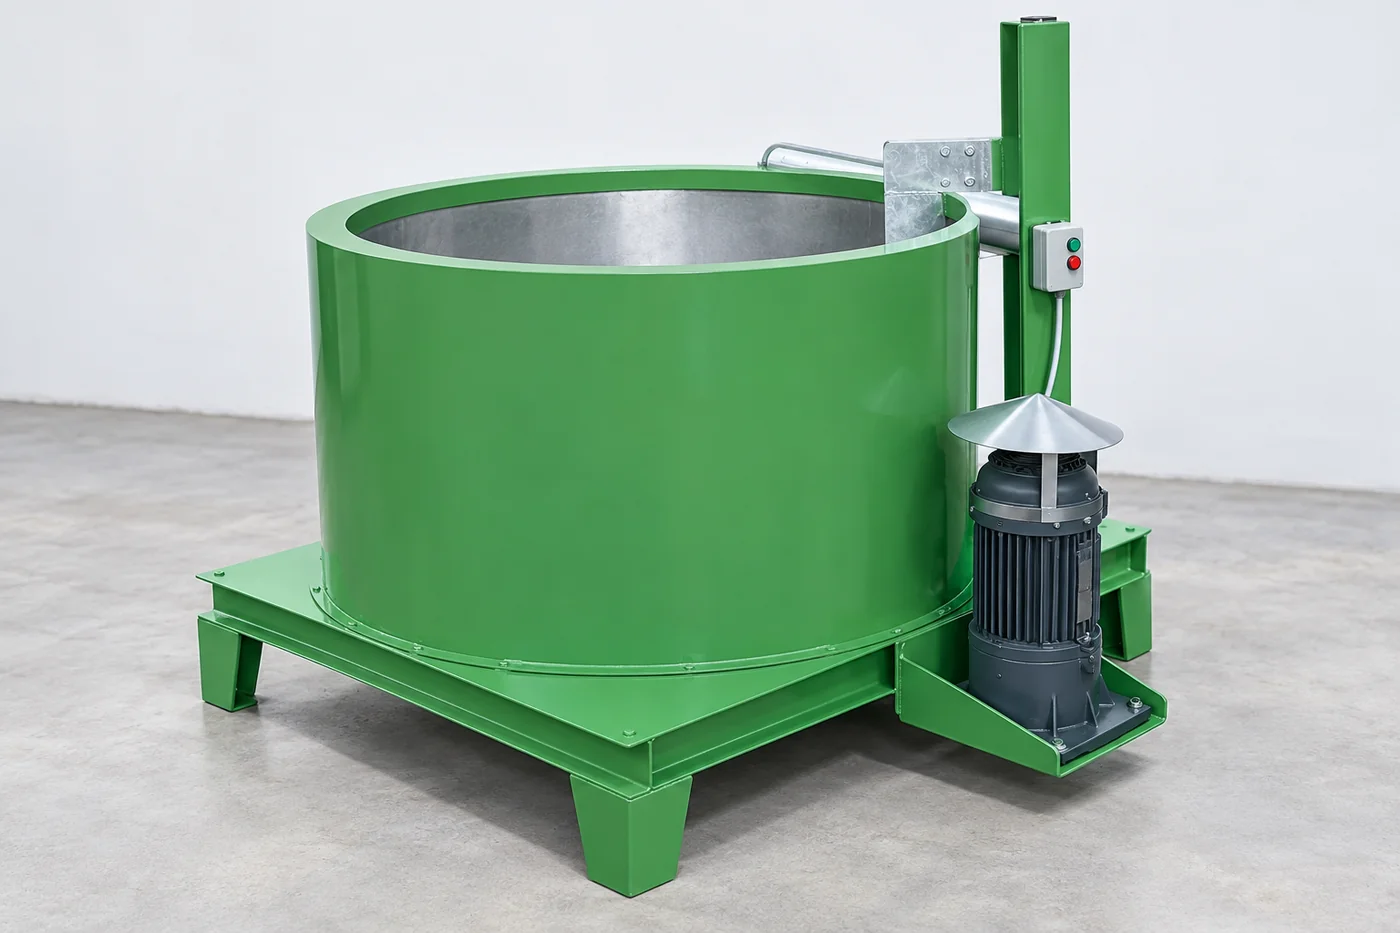
| Mixing reference | 7.5 kW; 380 V three-phase enquiry |
| Selection rule | Define the operation before selecting the equipment |
02 · DEWAXING
Review the dewaxing unit in its process context
- Dewaxing task
- Provide pattern arrangement, working space and process conditions.
- Selected vessel
- Confirm controls and services for that wax/shell system.
Share the pattern arrangement, required working space and applicable process conditions. Confirm the selected vessel, controls and services instead of transferring a catalogue cycle to a different shell or wax system.
Technical notes
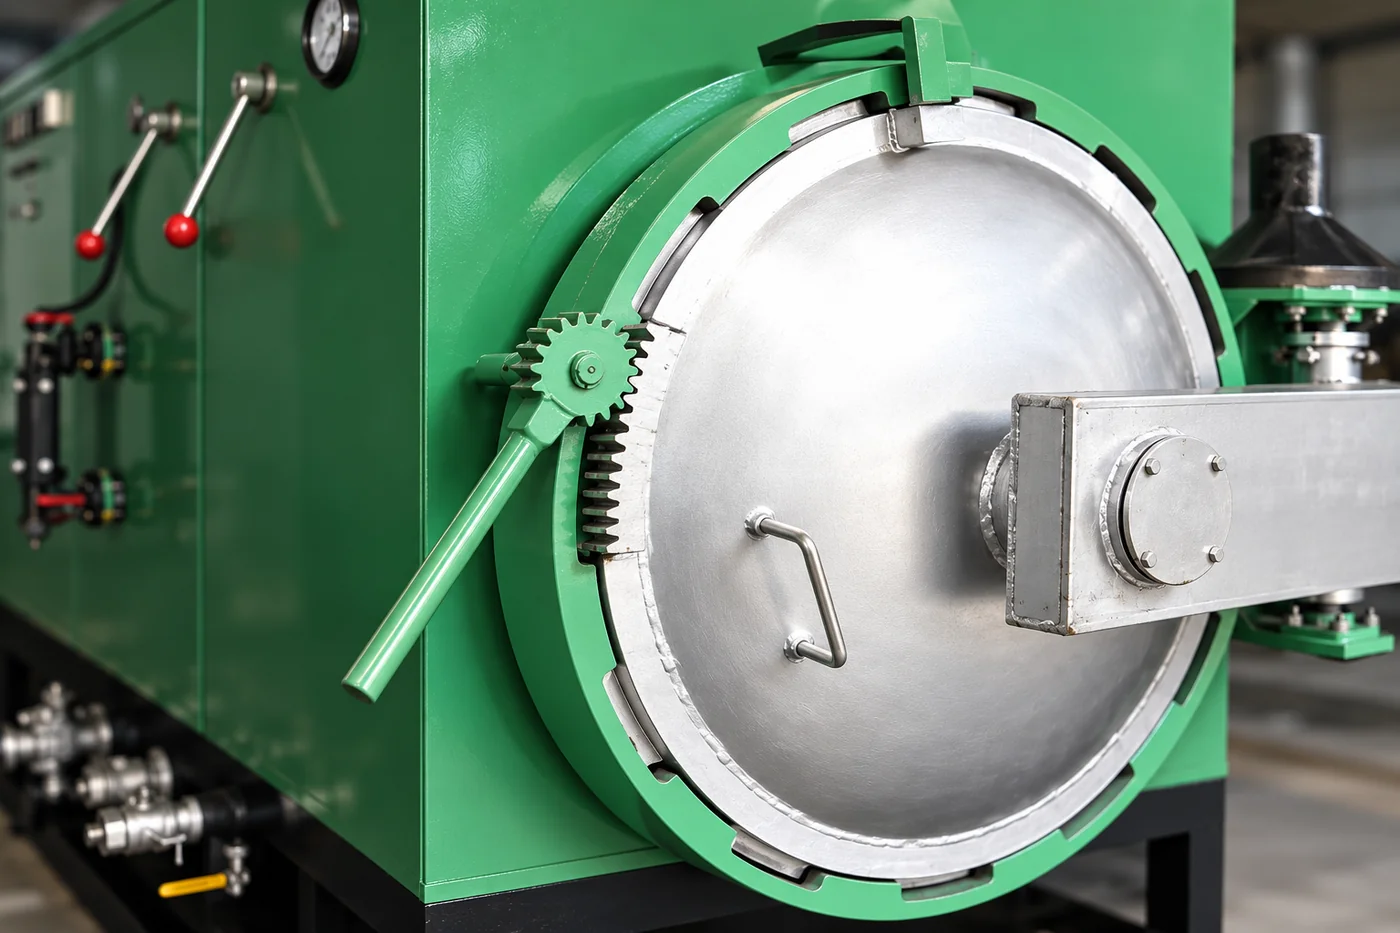
The dewaxing reference lists an 800–1,000 mm internal diameter and 1,000–1,200 mm depth; confirm the selected chamber and pressure-system requirements. The shell-removal reference lists 100 J impact energy and 1,050 impacts/minute, which are not specifications for making a ceramic shell.
MANUFACTURING ROUTE · FEATURES AND CONTROL
Place Each Auxiliary at Its Correct Foundry Stage
Dewaxing removes the pattern from the prepared shell using the selected unit's defined conditions. Shell removal happens after metal casting and must clear ceramic material without unnecessarily damaging the part. Mixing serves its own specified material and batch operation. Relia's review ties each task to its actual work envelope and interfaces: chamber/loading for dewaxing, impact and workpiece handling for shell removal, and material/charge for mixing. Acceptance is defined for that operation with the necessary utilities and documentation.
- Choose the operationDewax, remove shell or mix a defined material
- Match the work envelopeTree, casting or batch dimensions
- Specify the configurationControls, utilities, handling and supplied items
- Agree acceptanceRelevant trial and required machine records
04 · SHELL WORKFLOW
Connect shell-related equipment to the workpiece
- Workpiece envelope
- Define shell size, handling and the required operation.
- Workflow interface
- Connect the selected unit to adjacent stations.
Provide the shell or workpiece envelope, handling needs and intended operation. The selected equipment needs a defined place in that workflow and an agreed relationship to the adjacent stations.
05 · INSTALLATION
Plan utilities and interfaces by machine
List the electrical, connection, placement and handling requirements for each actual unit. Keep installation, commissioning and training scope visible when several machines are quoted together.
06 · MATERIAL HANDLING
Size mixing equipment from the actual task
- Mixing requirement
- State the material, working batch and intended operation.
- Usable configuration
- Confirm vessel, drive and included functions.
Share the material, working batch and required mixing operation. Confirm vessel, drive and other included functions for the selected unit before comparing nominal machine sizes.
07 · PURCHASING
Retain separate acceptance for separate operations
Agree installation services, operating conditions and operation-specific acceptance tests. The dewaxing listing's 6–12-minute field is a cycle reference, not complete plant throughput. Pressure-system documentation and local installation requirements need review for the selected destination and configuration.
Technical notes
For dewaxing, provide shell-tree envelope, loading method and cycle requirements. For shell removal, define casting size and the retained features that must be protected. For mixing, identify the actual material and batch duty rather than choosing from a generic machine-type label.
| Package record | Retain |
|---|---|
| Function | Operation and working medium for each unit |
| Installation | Selected utilities and interfaces |
| Acceptance | Unit-specific documents and checks |
CONNECTED BUYING GUIDES
Continue with the next project decision
Follow the related component and purchasing guides, or open the catalogue reference to carry this requirement into a specific project enquiry.
RELIA · YOUR NEXT PROJECT
Describe the foundry step and the required output
Send the current workflow, material, workpiece or batch, and available utilities. Identify the operation each unit must perform. We can review the equipment schedule with individual functions and handover requirements clear.
Start with these project details
- Current foundry workflow
- Operation for each selected unit
- Workpiece or working batch
- Utilities and handover requirements
Shuyuan Road, Qingdao, Shandong, China
