
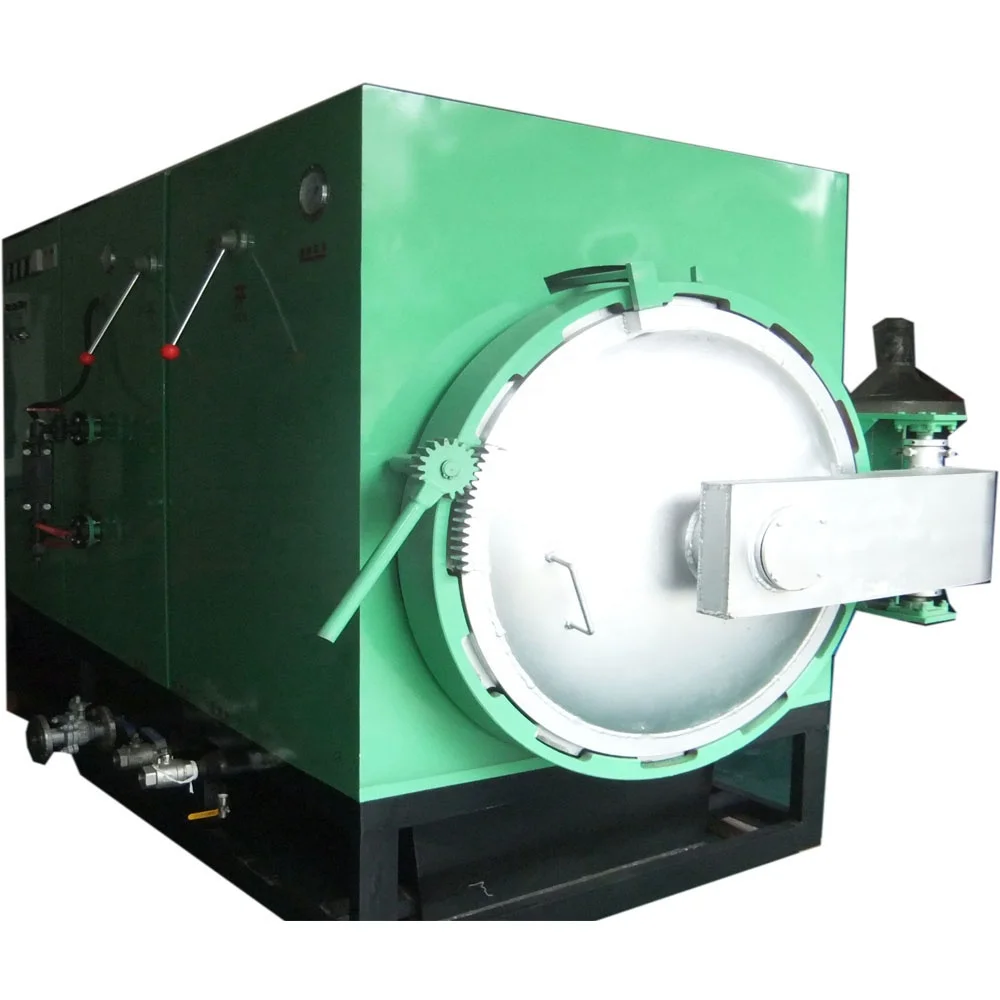
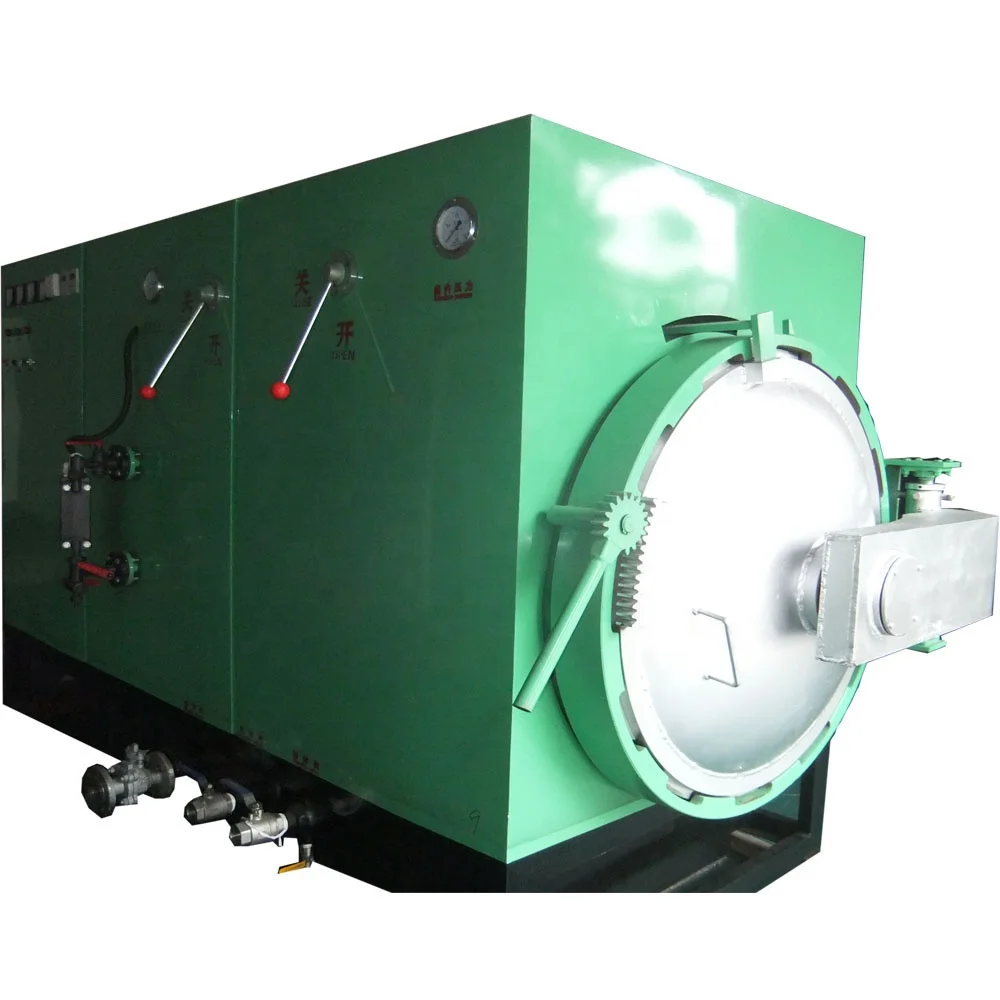
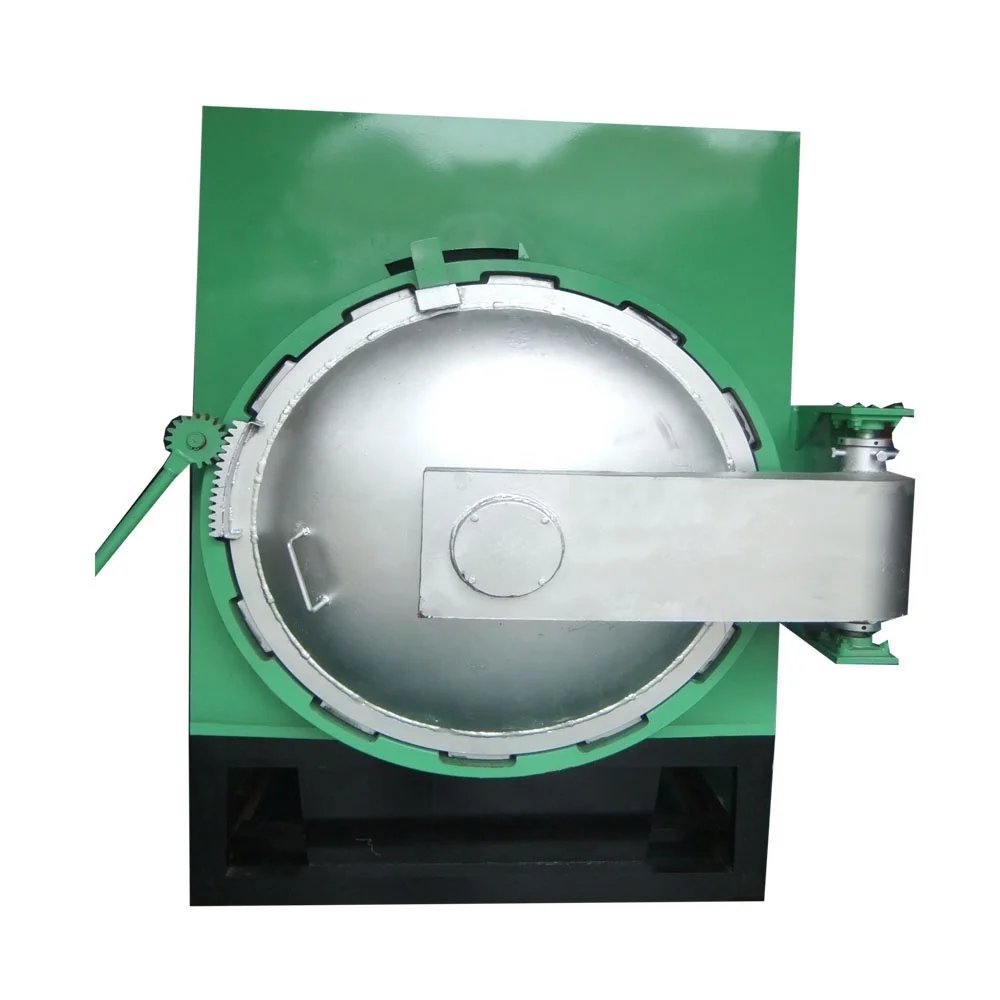
Automatic Precision Lost-Wax Investment Casting Dewax Machine with PLC | 165°C
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
machine typeDewaxing machinevideo outgoing-inspectionProvided
-
machinery test reportProvidedcore componentsPLC, Motor
-
voltagecustomizablepower(w)Customized
-
dimension(l*w*h)Customizedwarranty1 Year
-
key selling pointsAutomaticweight (kg)1
-
Item namelost wax stainless steel castingWaterpump power3KW
-
Heating tube quantity4-5 piecesHeating tube power24KW
-
Pressure controlling quantity2 piecesInner diameter800-1000mm
-
Depth1000-1200mmSeal ring size800-1000mm
-
Working temperature165℃Dewaxing time6~12 Min
-
ConditionNewWarranty of core components1 Year
-
Applicable IndustriesManufacturing Plant
-
Marketing TypeHot Product 2024
Automatic dewaxing-machine inquiries support lost-wax investment casting and manufacturing-plant work, with PLC and motor core components. Working references are 165°C and a dewaxing time of 6–12 minutes, with voltage, power and overall dimensions customized for the selected machine.
Internal dimensions and the workpiece arrangement
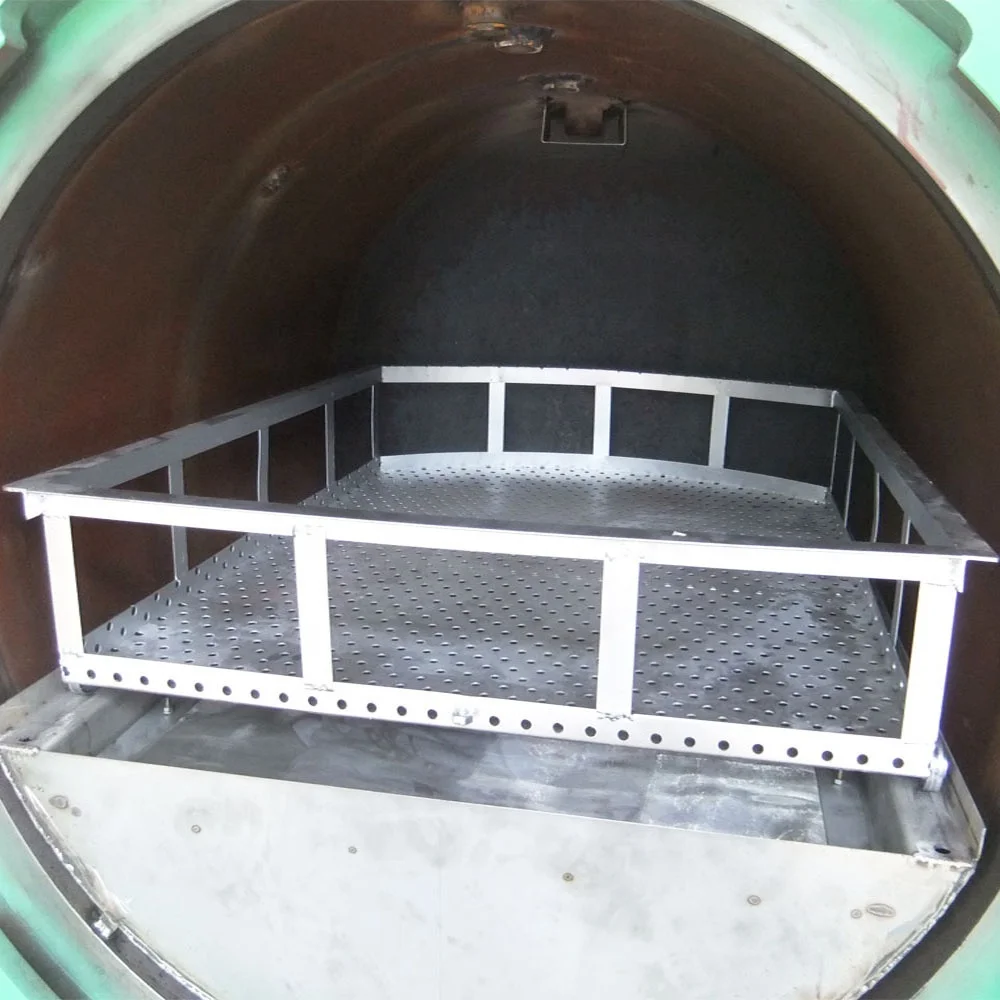
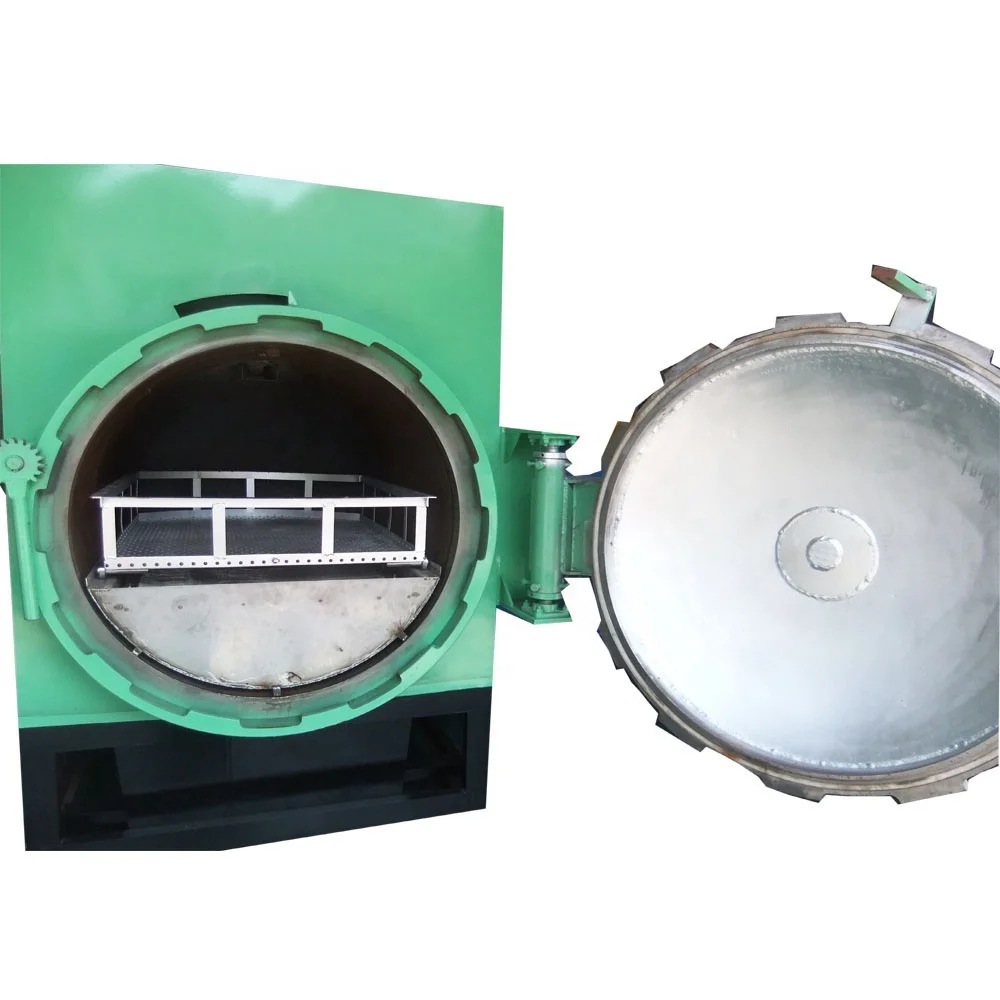
The inner-diameter reference is 800–1000 mm, depth is 1000–1200 mm and seal-ring size is 800–1000 mm. Select the dimensions for the actual wax/workpiece arrangement and required fit. Relate those internal references to the configured overall dimensions before agreeing the equipment and installation scope.
Water-pump and heating-tube references
The water-pump power reference is 3 kW, with 4–5 heating tubes and a 24 kW heating-tube-power reference. Agree whether the heating figure applies per tube or to the configured heating system. Define the actual electrical and power requirement for the selected machine so the pump, tube quantity and heating basis are clearly assigned.
165°C, cycle time and pressure controls
Connect the temperature and 6–12 minute dewaxing-time references to the intended wax/workpiece process. Two pressure-control items form part of the technical scope, with actual pressure and control acceptance to be agreed. Establish the operating cycle and inspection criteria for the selected arrangement so that timing and controls address the work being processed.
Configuration evidence for the dewaxing inquiry
An outgoing-inspection video and machinery test report can be provided for the selected dewaxing-machine inquiry. Review the applicable evidence against the configured dimensions, electrical/heating scope and operating acceptance. The automatic control, workpiece fit and agreed process conditions can then be considered together when selecting the actual machine.








