
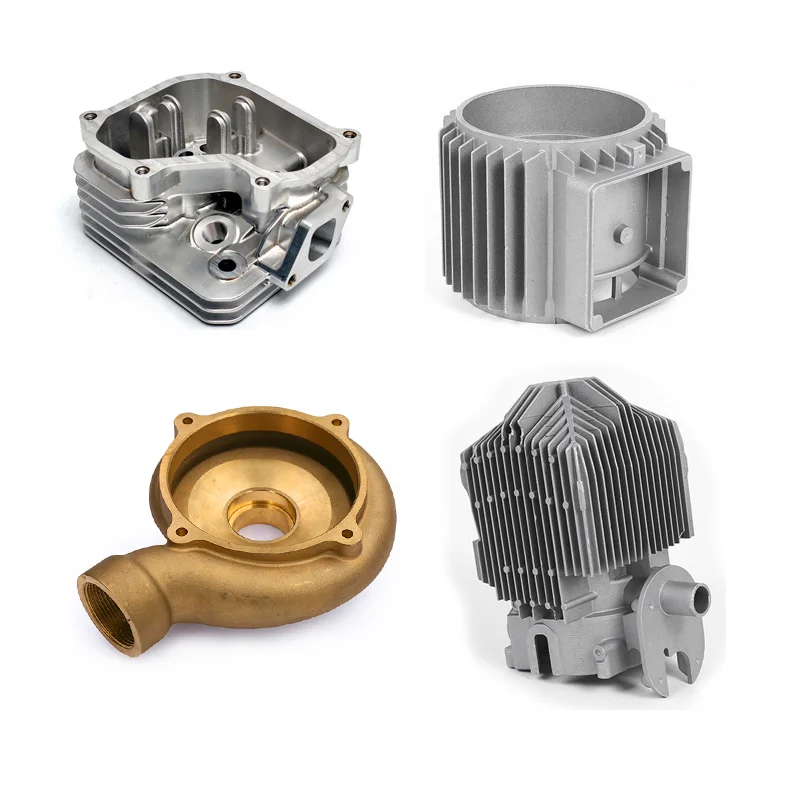
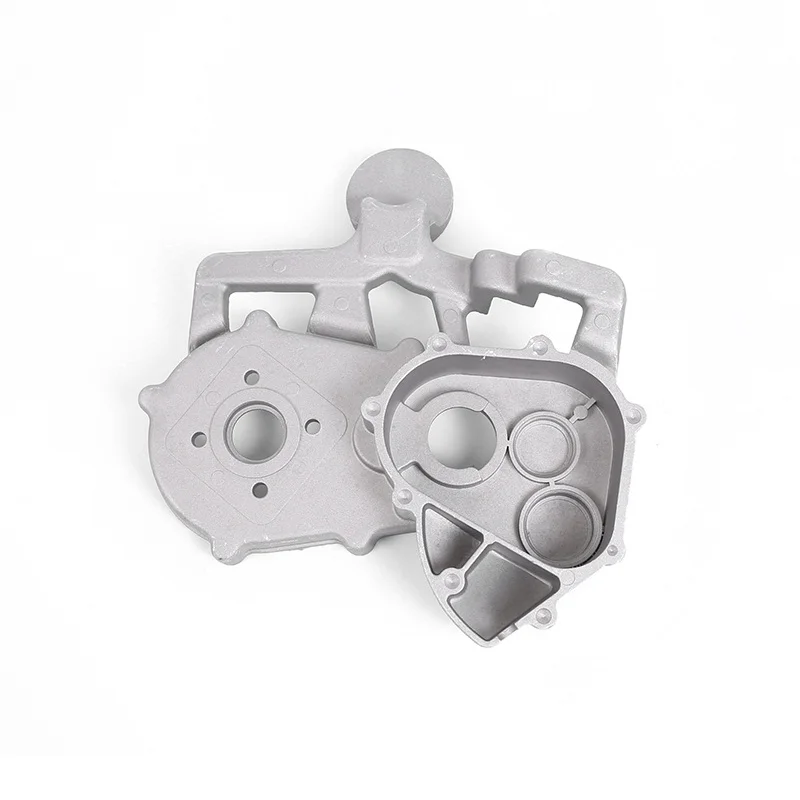
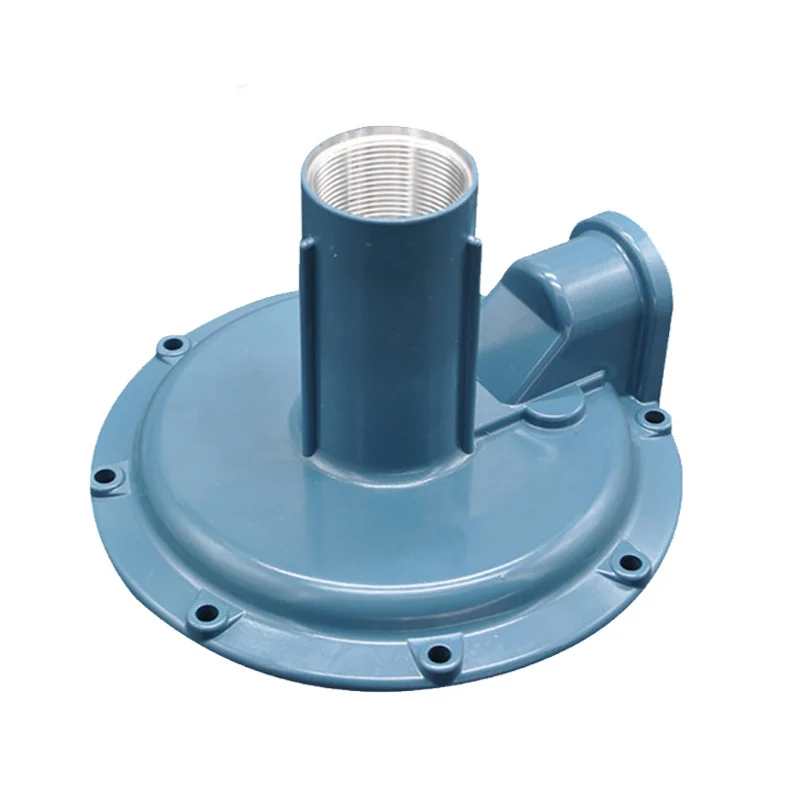
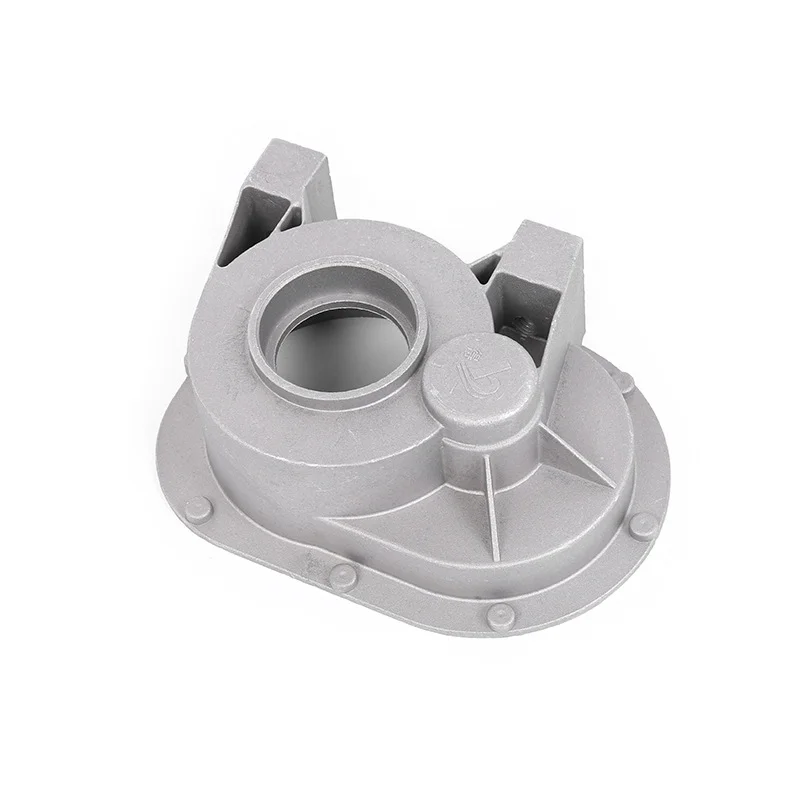
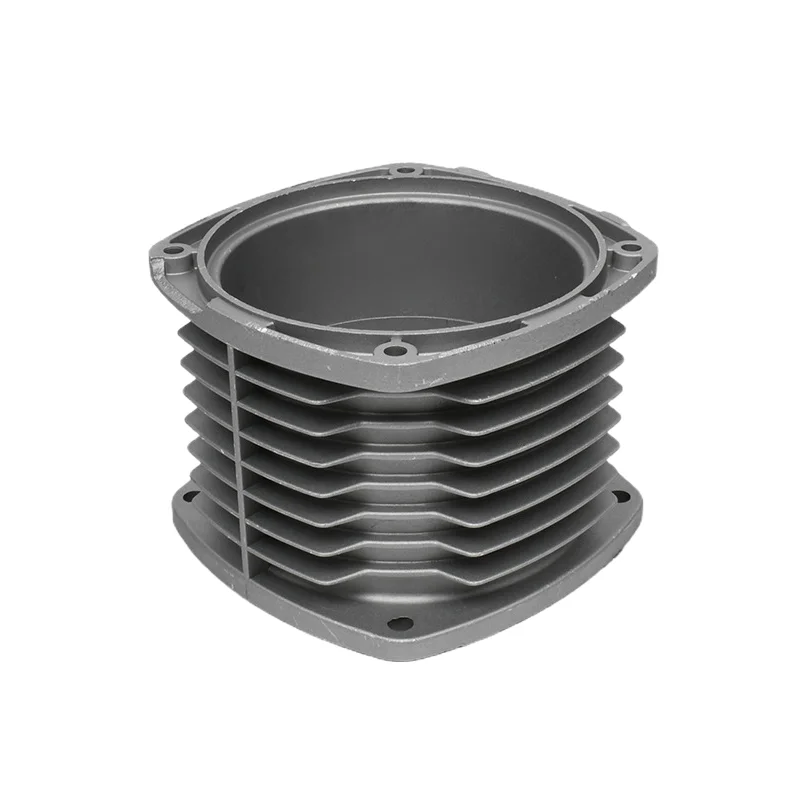
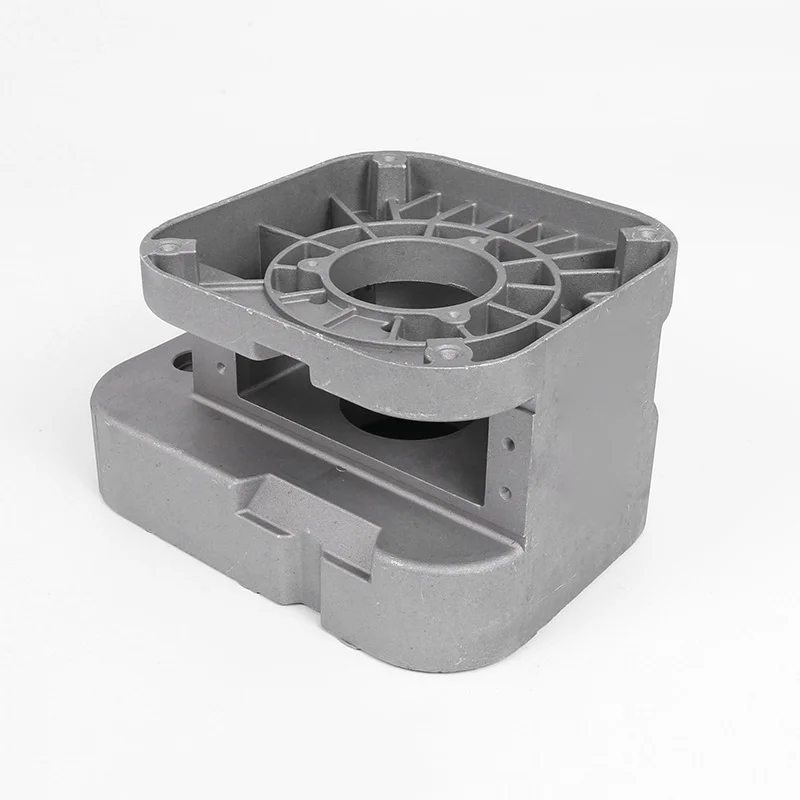
Precision ADC-12 Aluminum and Zinc Die Casting for Custom OEM Auto Parts
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
NameDie casting Services
-
MaterialAluminum,Zinc,MagnesiumSurface treatmentDeburr
-
ProcessCasting +Machining(if Need)+surface TreatmentQualityStrictly 100% Inspection
-
ServiceOEM ServiceCertificationISO 9001
-
PackingStandard PackingApplicationAuto parts
Precision die-casting enquiries serve custom OEM auto parts in aluminum, zinc and magnesium material directions. ADC-12 is an aluminum grade direction for the requested work. Select the actual alloy and component drawing so that the casting and any subsequent operations meet the intended finished-part requirements.
Alloy and auto-part geometry
Define the material grade and the working geometry for the selected component. The drawing should identify the interfaces and dimensions to be accepted for its use in the auto application. An aluminum, zinc or magnesium selection needs those component requirements alongside the chosen manufacturing scope. Agree the actual part definition rather than relying on a general auto-parts label to establish fit.
Casting with optional machining and deburring
The offered process direction is casting with machining if needed and surface treatment. Deburring is the stated surface operation for the die-cast part. Identify any dimensions or working details requiring further machining, then agree those operations. Define the required edge and surface condition for deburring so that the accepted result matches the component drawing.
Inspection and OEM acceptance criteria
Quality control states strict 100% inspection, with ISO9001 as the certification reference. Agree the inspection criteria and applicable quality documents for the actual auto part. Confirm the selected alloy, drawing revision, dimensional requirements and deburring scope together. These details establish the requested precision and finished condition without assigning an unsupported numerical tolerance or additional coating to the service.








