
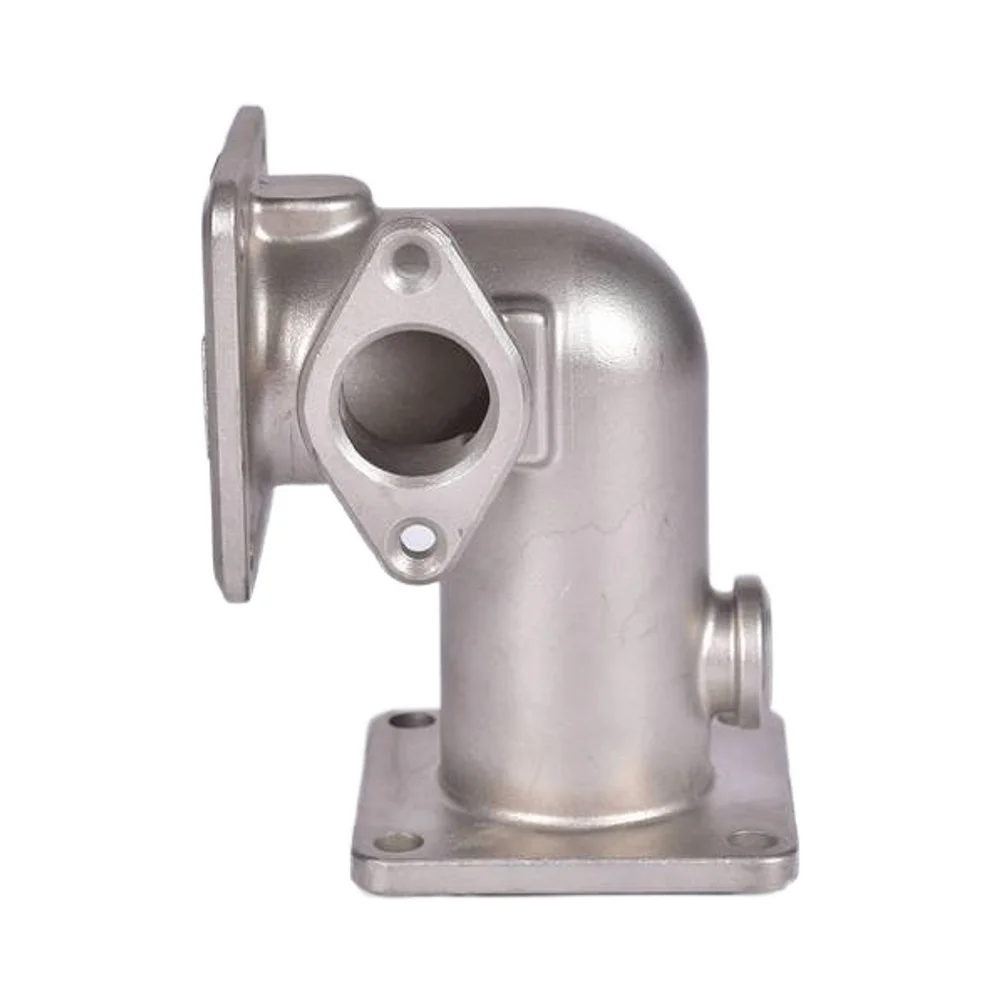
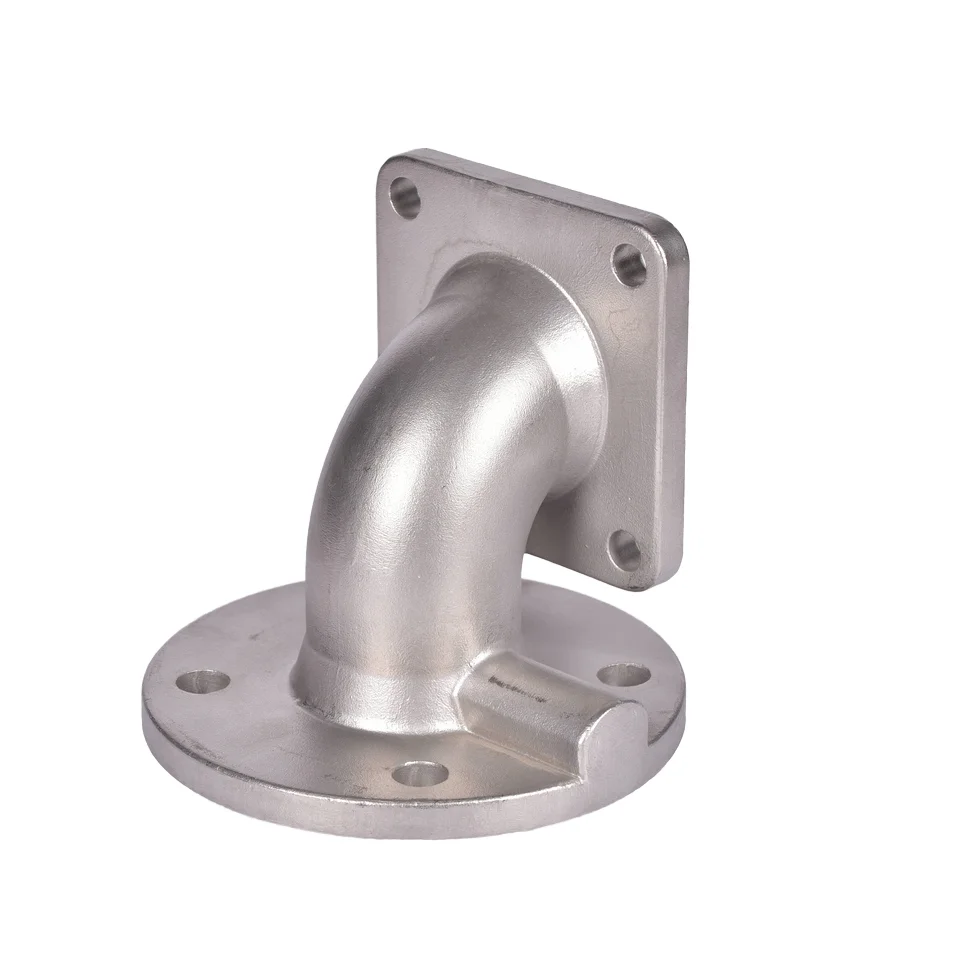
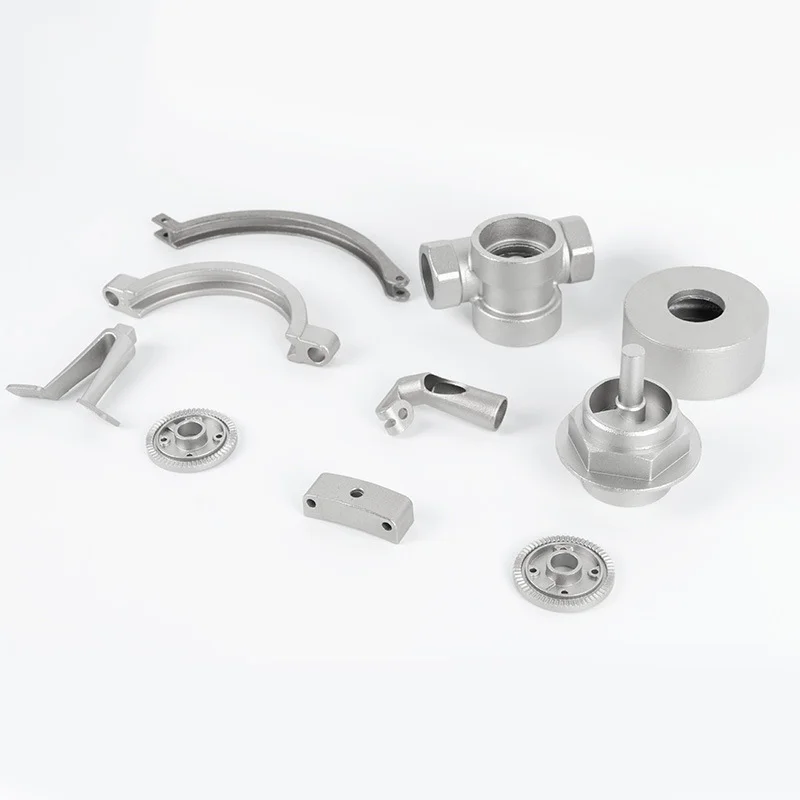
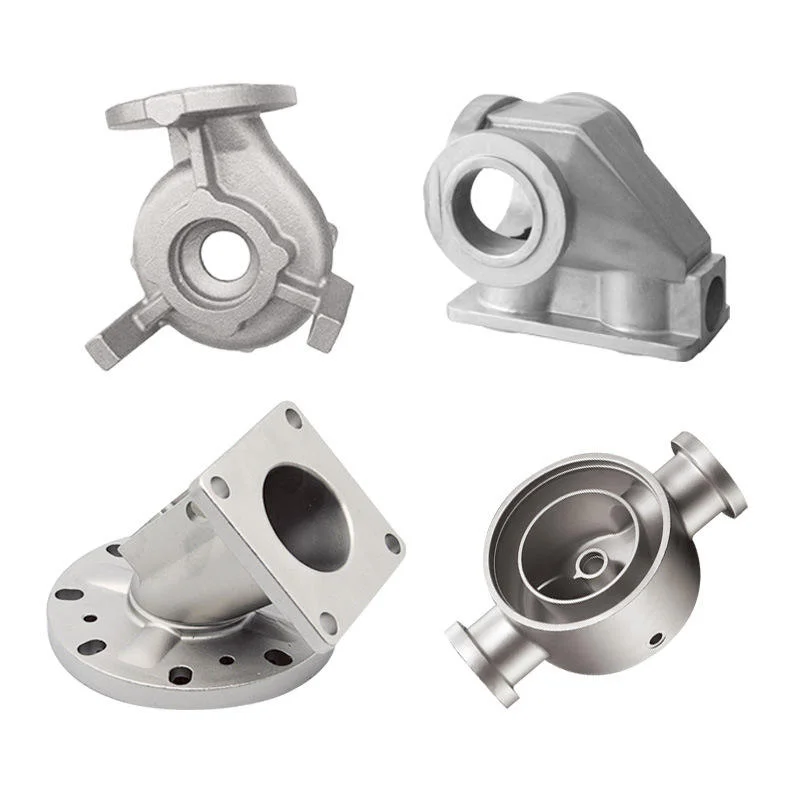
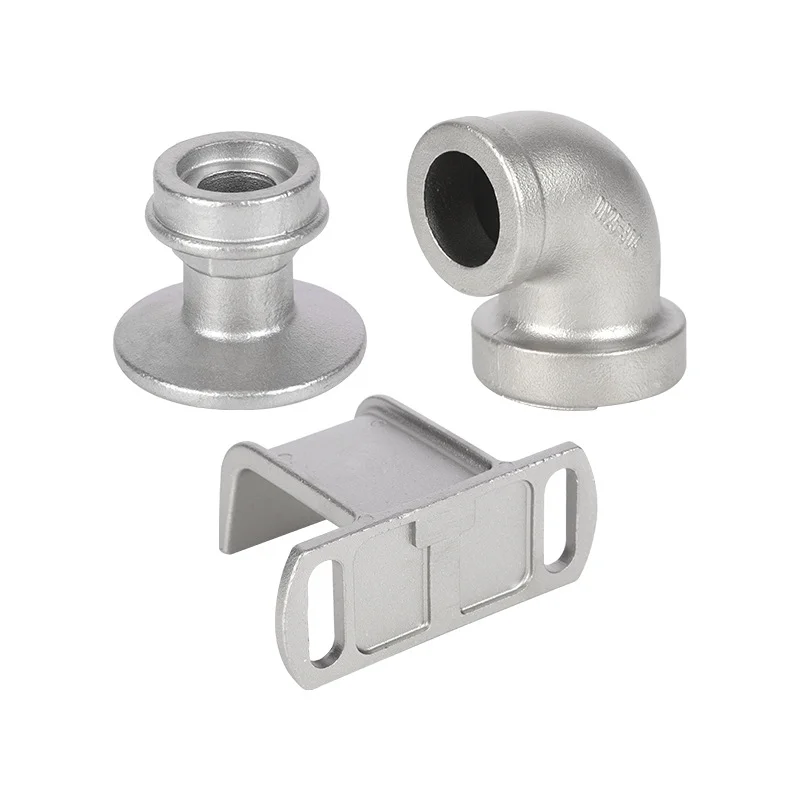
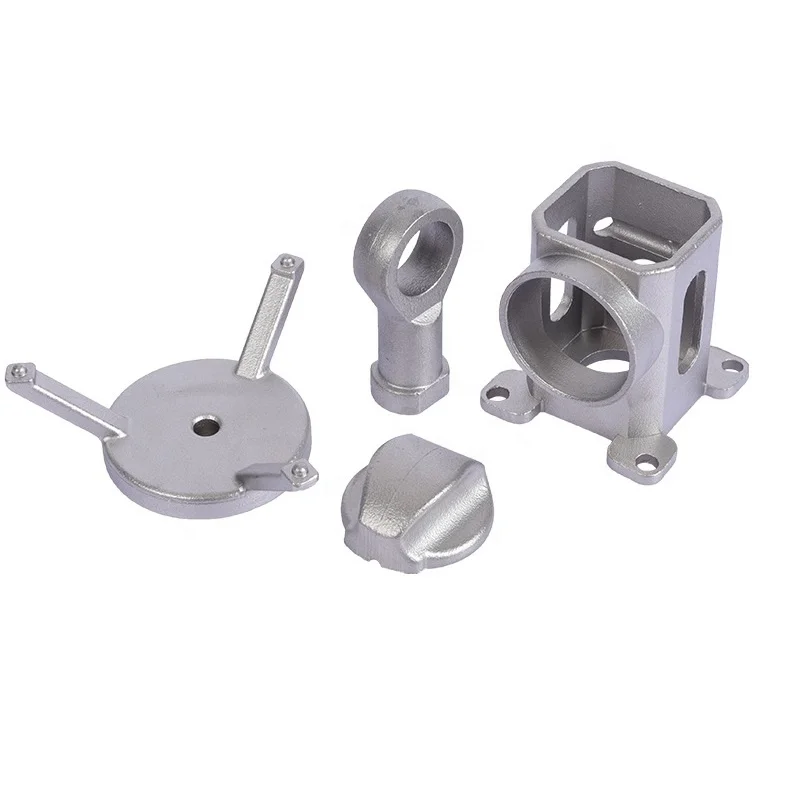
OEM Lost Wax Cast Utensil Joints and Fittings for Food Equipment Projects
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Component FormFitting / JointSurface FinishAs Cast , Polished
-
Casting ProcessLost Wax Investment Casting, Silica Sol, Medium Temperature Wax
-
Precision GradeCT5--CT12, ±0.05--0.5 mm (By Size)CertificationISO9001, Material Traceability (COC), PPAP Supported
-
Surface FinishRa 1.6 - 3.2 Micro (As Cast), Electro-polishing ServiceHeat TreatmentQuenching & Tempering, Normalizing, Annealing
-
Testing ServiceCMM Inspection, Material Spectral Report, PT/MT/NDTSecondary ProcessCNC Machining In-House, Polishing, Assembly
-
Sample Lead TimeDFM Review 72 Hours, Samples 5--10 DaysTypical ApplicationPump Impeller, Valve Body, Marine Hardware, Food/Medical Parts
-
Supplier TypeOEM/ODM Custom Manufacturing Factory with Design Support
OEM utensil joints and fittings can be developed through silica sol lost wax investment casting using medium-temperature wax. Design support, in-house CNC machining, polishing and assembly can form the manufacturing scope, with the selected material and food-contact requirements established for the intended utensil component.
Start with the contact material and conditions
Identify the material, intended contact conditions and finished surface needed for the food-equipment joint or fitting. Agree the applicable conformity evidence and acceptance criteria for the supplied part. These requirements should accompany the component drawing so material and surface decisions address the actual use.
Apply the precision range by component size
The precision scope is CT5–CT12 and ±0.05–0.5 mm by size. Mark the relevant dimensions and acceptance basis for each feature, including the interfaces requiring CNC machining. Keep those requirements tied to the approved drawing so the casting and secondary operations can be reviewed against the intended joint or fitting geometry.
Define the surface and material condition
As-cast finish is Ra 1.6–3.2 Micro, with the unit and measurement basis to be confirmed for the part. Polishing and electropolishing services can be discussed for the required finished surface. Quenching and tempering, normalizing or annealing should be selected against the specified material and the condition required by the component.
Agree testing and traceability for approval
CMM inspection, material spectral reports and PT/MT/NDT are testing services to specify by feature and acceptance requirement. Material traceability, COC and PPAP support should be defined as order deliverables, with current ISO9001 certificate scope reviewed where required. Use DFM and design support to agree the drawing, manufacturing operations and verification plan before approving the custom part for its intended food-equipment application.








