
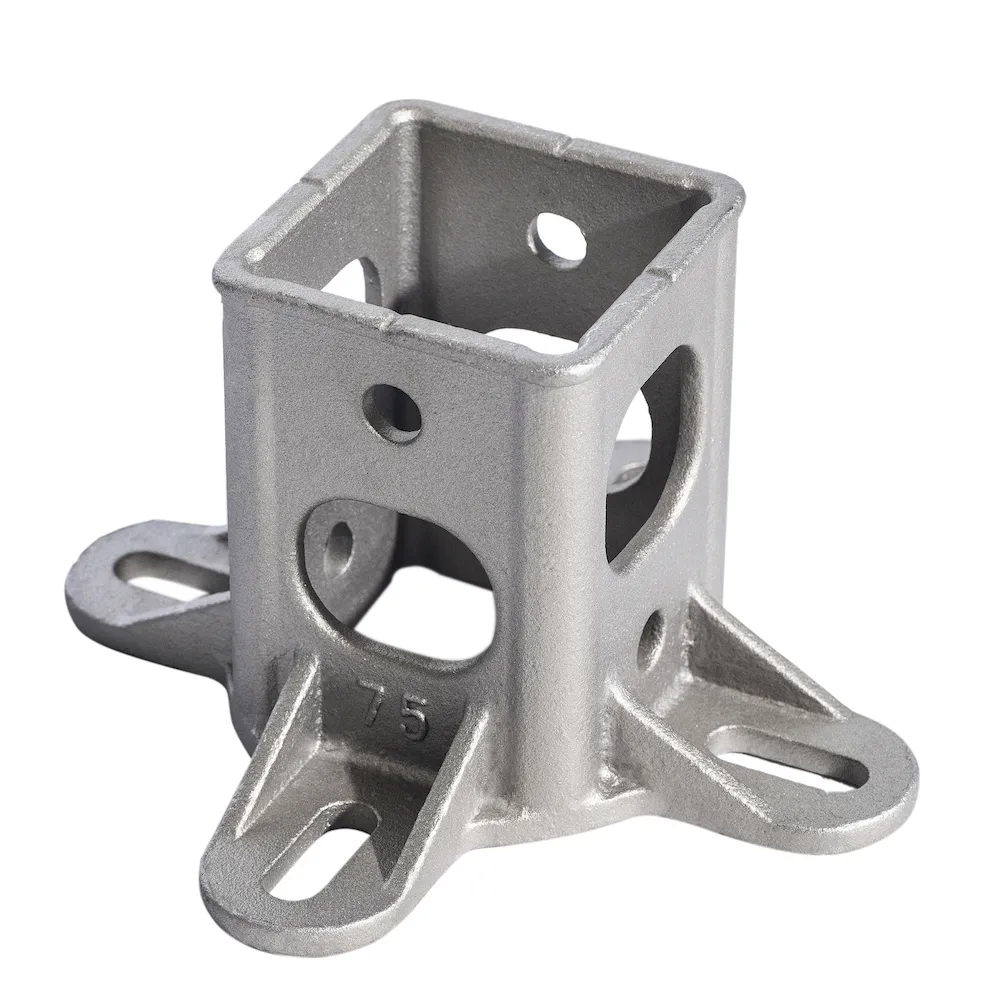
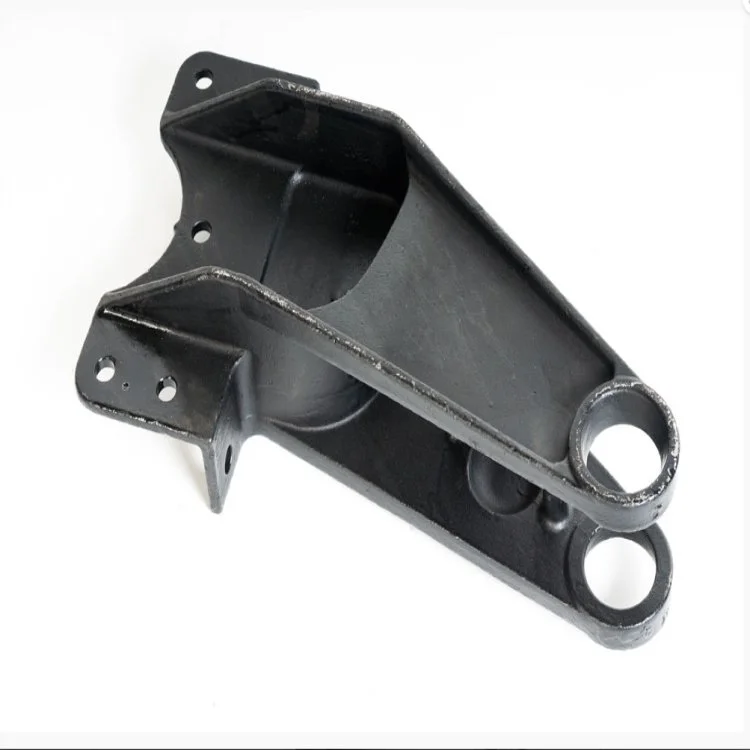
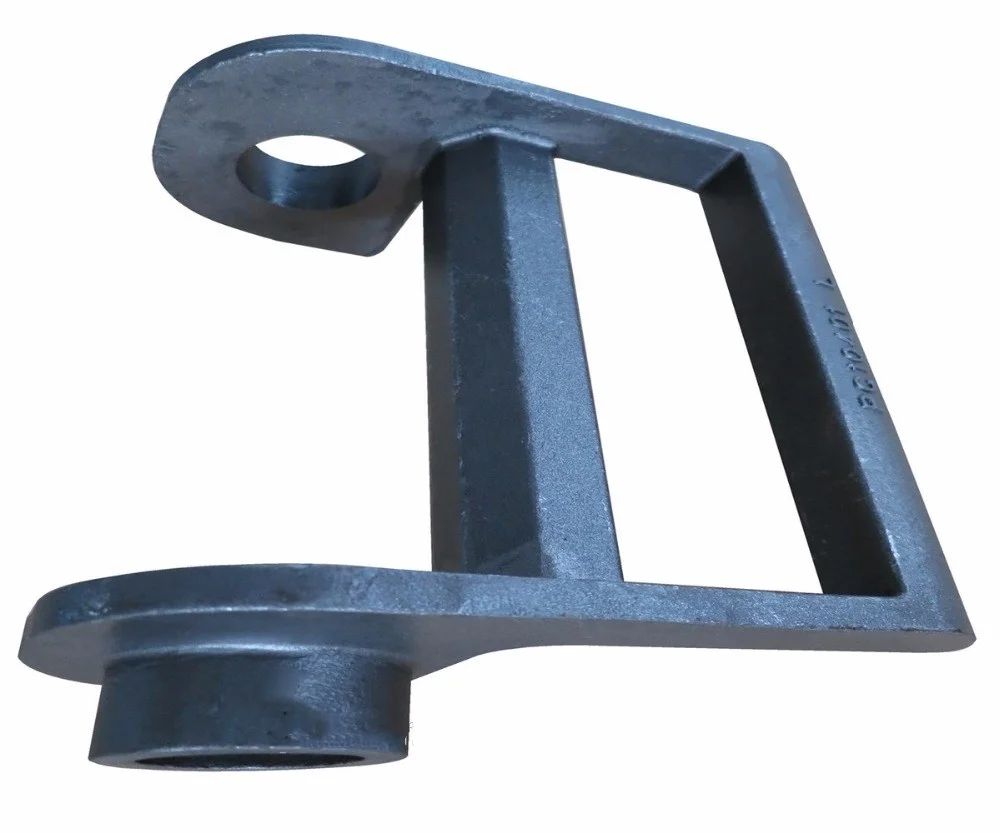
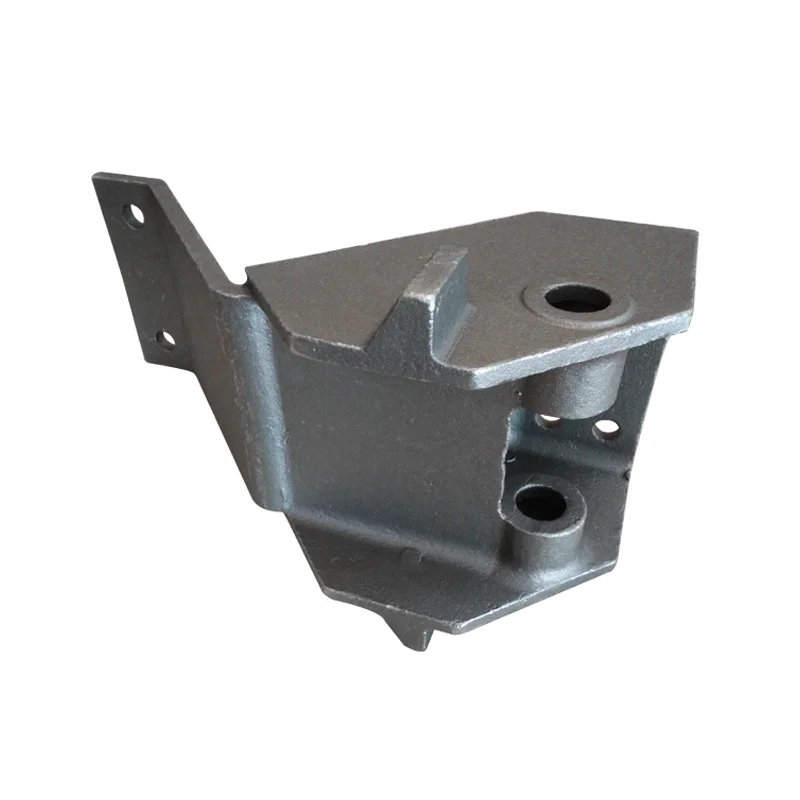
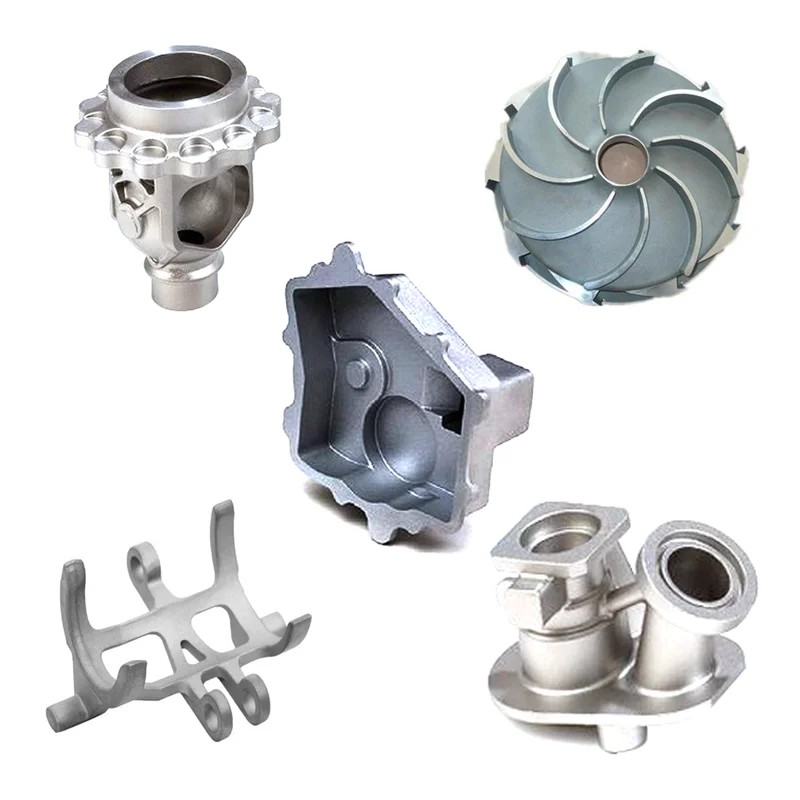
Custom Steel Cylinder Head Lost Wax Investment Casting and CNC Machining Foundry Services
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishPassivated , PolishedAlloy GradeWCB
-
ItemCylinder Head Steel Casting Foundry Lost Wax Investment Casting Parts
-
MaterialG35, G45, WCB, WCA, WCC, ISO 340-550, etc. As customer requestManufacturing ProcessInvestment casting, option Lost wax casting
-
Casting ToleranceCT4-8 for investment casting partsMachining ProcessCNC Machining/ Lathing/ Milling/ Turning/ Boring/ Drilling etc.
-
Machining TolearnceUp to IT7, Ra 0.8~3.2 , according to customer requirementSurface TreatmentSurface Passivatin, Polish. As customer requests.
-
PackageMultilayer wood box with big plastic bag inside.Lead Timeabout 55 days for investment casting parts
-
ServiceSupply investment casting parts
Custom steel foundry enquiries include cylinder-head parts made through investment and lost wax casting directions. CNC machining is available for selected working details. Define the actual steel grade and cylinder-head drawing before agreeing the cast geometry, finished dimensions and surface requirements for the component.
Steel designation and cylinder-head geometry
Material directions include G35, G45, WCB, WCA and WCC, with ISO 340-550 as another stated reference. Confirm the selected grade and applicable document for the requested part. Identify the interfaces and service conditions relevant to the cylinder head, together with the dimensions to be accepted. The material labels do not establish interchangeability or a particular engine fit.
Cast dimensions and machined working details
The casting and machining references apply to different stages. Define their selected dimensions and acceptance on the current drawing.
- Investment-cast geometry
- CT4-8 is the casting tolerance reference for the part.
- Machined features
- CNC machining, lathing, milling, turning, boring and drilling are offered directions. Up to IT7 and Ra 0.8~3.2 are machining references according to the customer requirement; confirm the applicable features and roughness unit.
Selected surface and accepted component
Surface passivation and polishing are finish directions according to the requested result. Choose the treatment for the actual steel and identify the areas to receive it. Agree the drawing revision, material requirements and dimensional and surface inspection criteria together. These details define the accepted cylinder-head casting and machining scope for the foundry enquiry.








