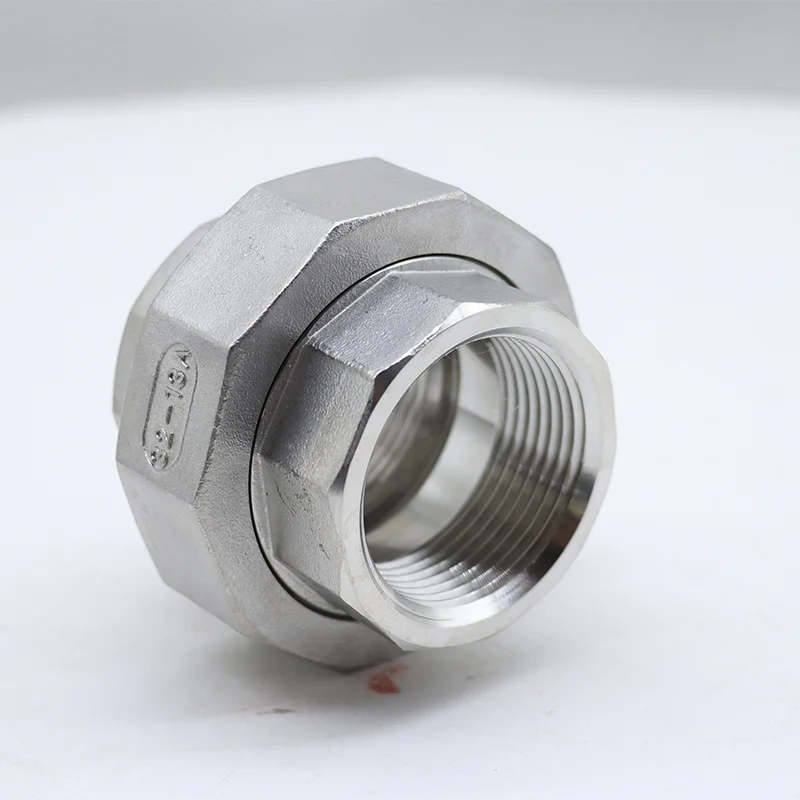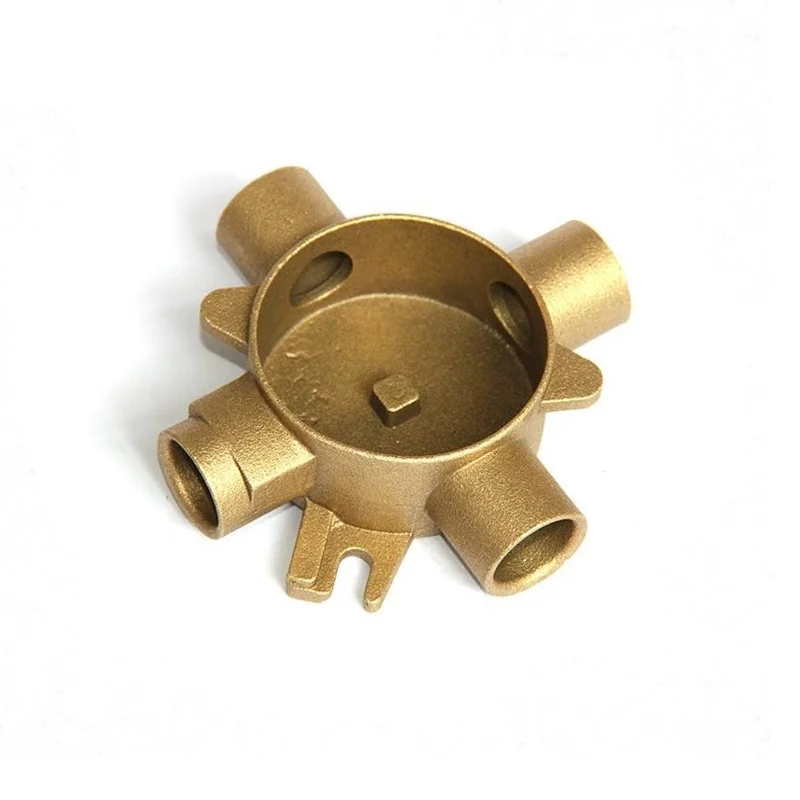
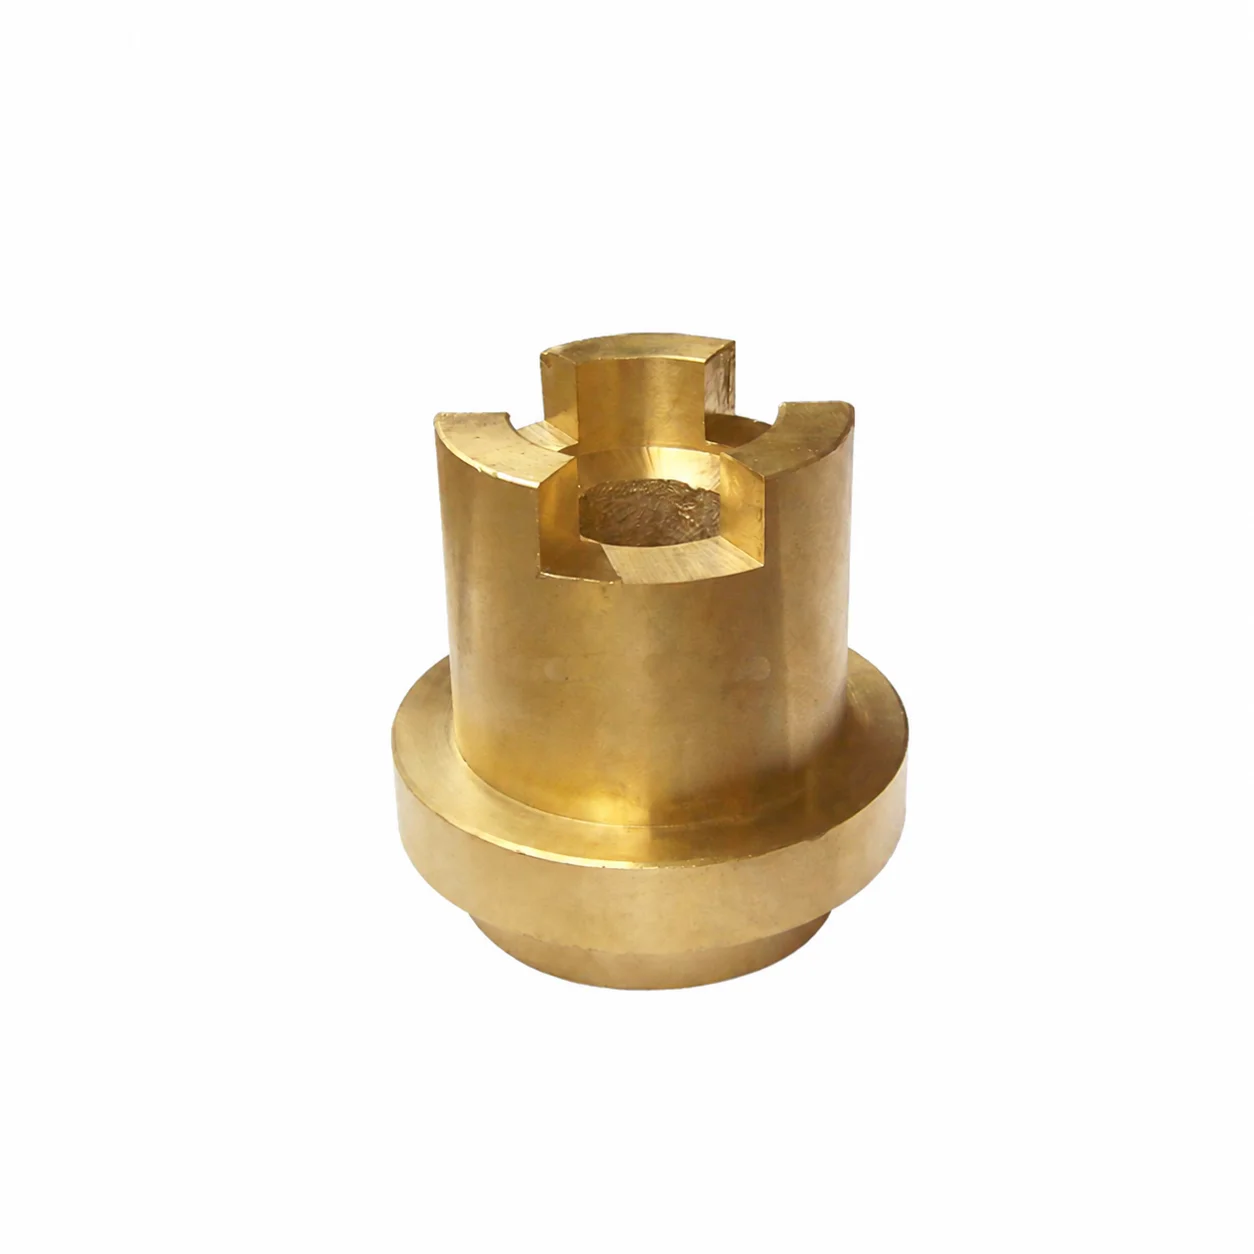
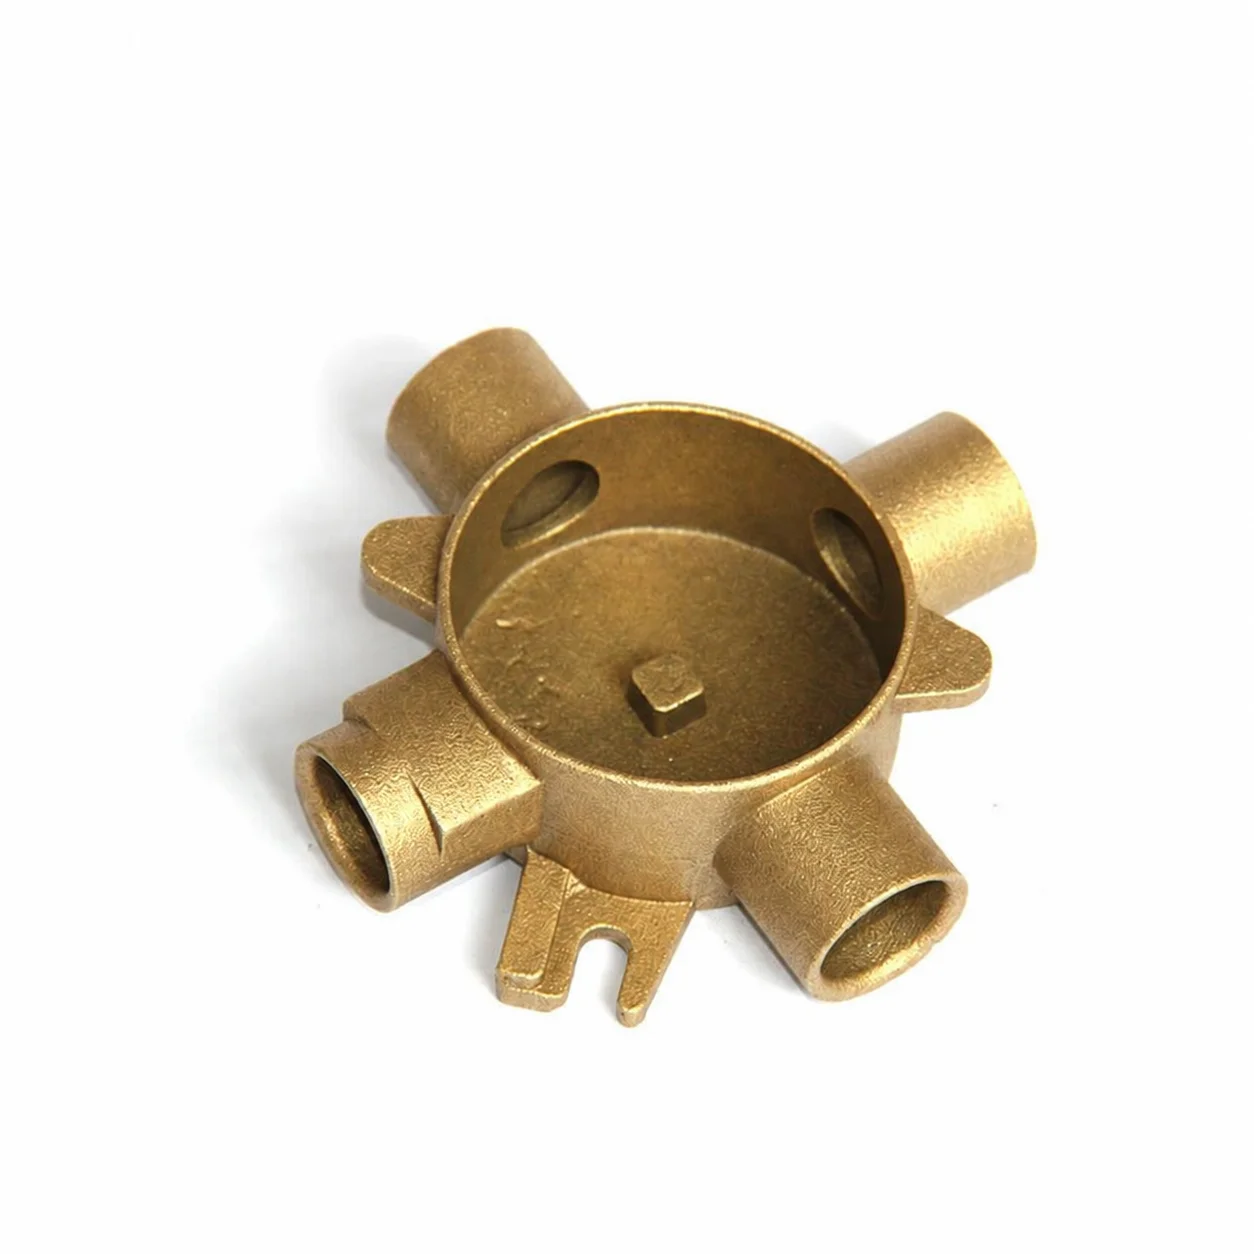
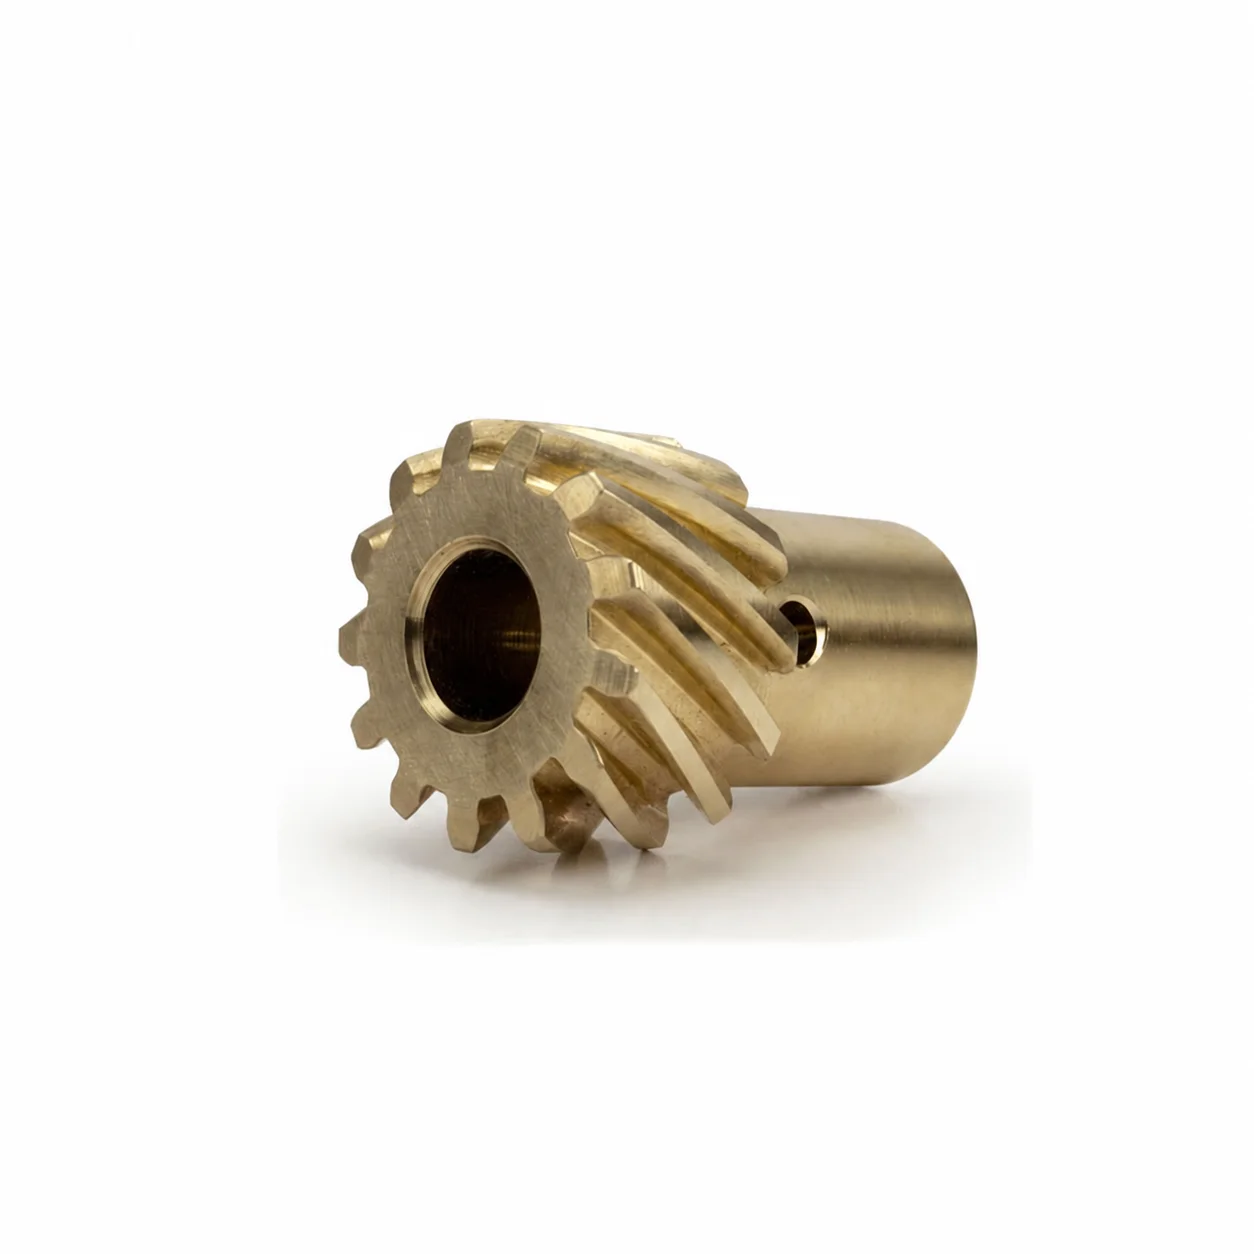
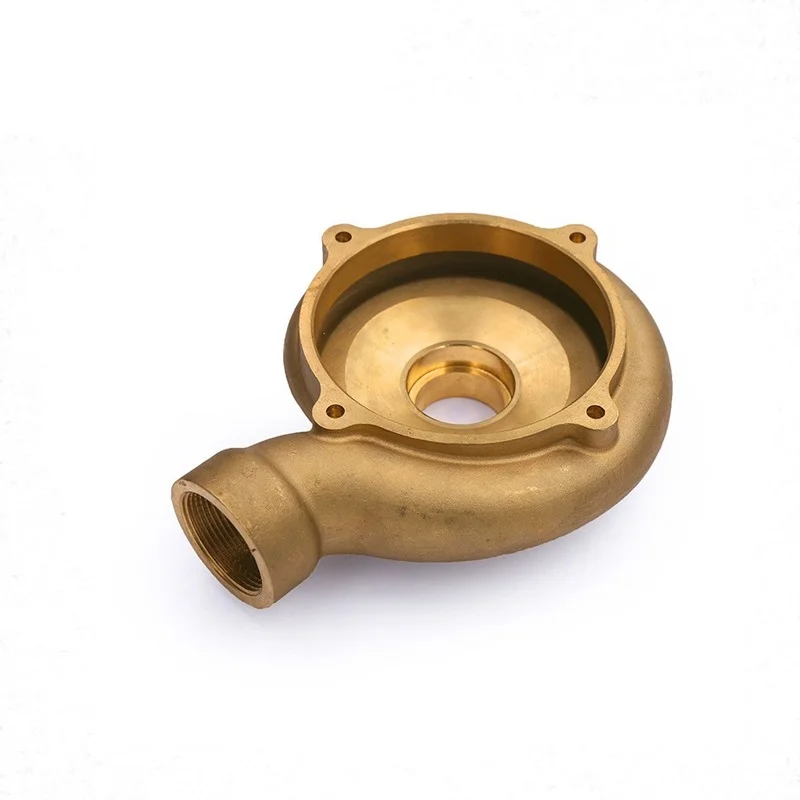
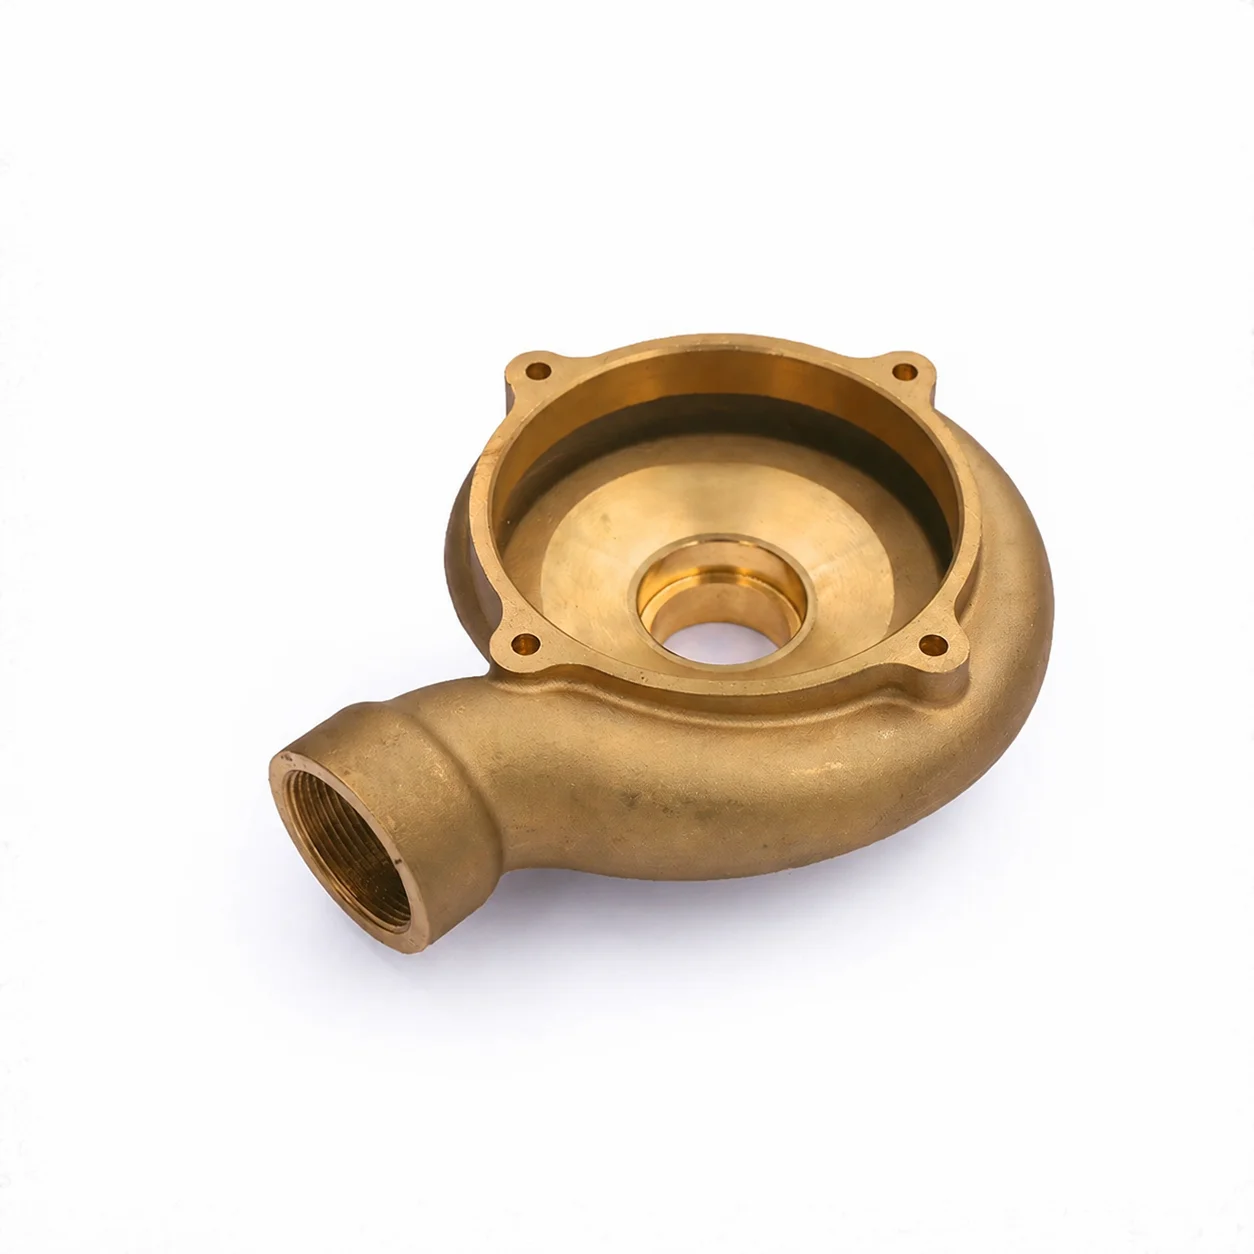
Custom Brass/Bronze Investment/Lost-Wax Parts | 304/316/316L Stainless Options and CNC Machining
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishPassivated , PolishedAlloy Grade316L , 316 , 304
-
ItemLost Wax Method Casting Part Custom Metal Brass Bronze Casting
-
MaterialCasting stainless steel 304, 316, 316L etc. As customers request.Manufacturing ProcessInvestment casting, option Lost wax casting
-
Casting ToleranceCT4-8Machining ProcessCNC Machining/ Lathing/ Milling/ Turning/ Boring/ Drilling etc.
-
Machining TolearnceUp to IT7, Ra 0.8~3.2 , according to customer requirementSurface TreatmentSurface Passivatin, Polish. As customer request
-
Package of lost wax castingMulti-layer wooden box/pallet, with big plastic bag insideLead Time45 days for invest casting metal brass bronze
-
Our ServiceSupply invest casting metal brass bronze
Custom brass and bronze parts are directed to investment/lost-wax casting, with 304, 316 and 316L stainless-steel material references also available for selection. CNC machining, lathing, milling, turning, boring and drilling are machining directions. Passivation and polishing follow customer requirements for the actual material and surfaces.
Brass, bronze or the selected stainless grade
The required material should be selected with the component's geometry and intended function. Identify whether the actual part uses brass, bronze or a chosen 304/316/316L stainless grade. Connect that choice to the investment/lost-wax scope and the interfaces that need machining, so the material and manufacturing definition address one actual component.
CT4–CT8, up to IT7 and Ra 0.8–3.2
CT4–CT8 is the casting-tolerance reference, while machining is referenced up to IT7. The Ra reference is 0.8–3.2, with its unit and measurement areas to agree. Assign those distinct criteria to the relevant cast dimensions, machined features and surfaces. The selected inspection requirements should explain how the actual component's geometry is accepted at each stage.
Six machining directions and two surface treatments
Choose the applicable CNC, lathing, milling, turning, boring or drilling work for the component's important dimensions and interfaces. Passivation and polishing are surface directions to define for the selected material and areas. Agree the required finished condition and its inspection with the actual grade and component function, keeping the cast, machined and treated acceptance within the same custom-part request.