
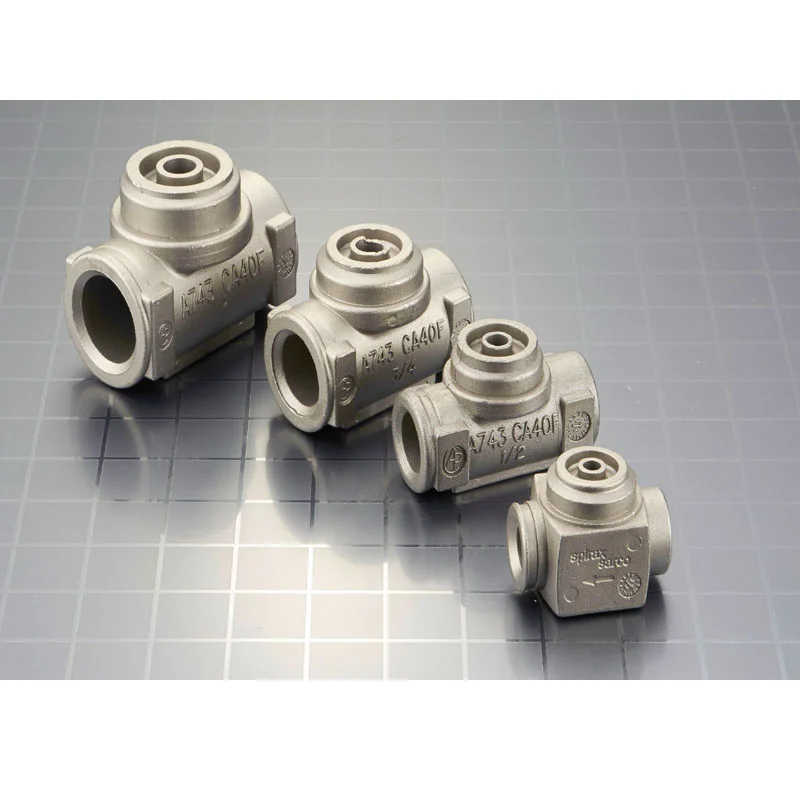
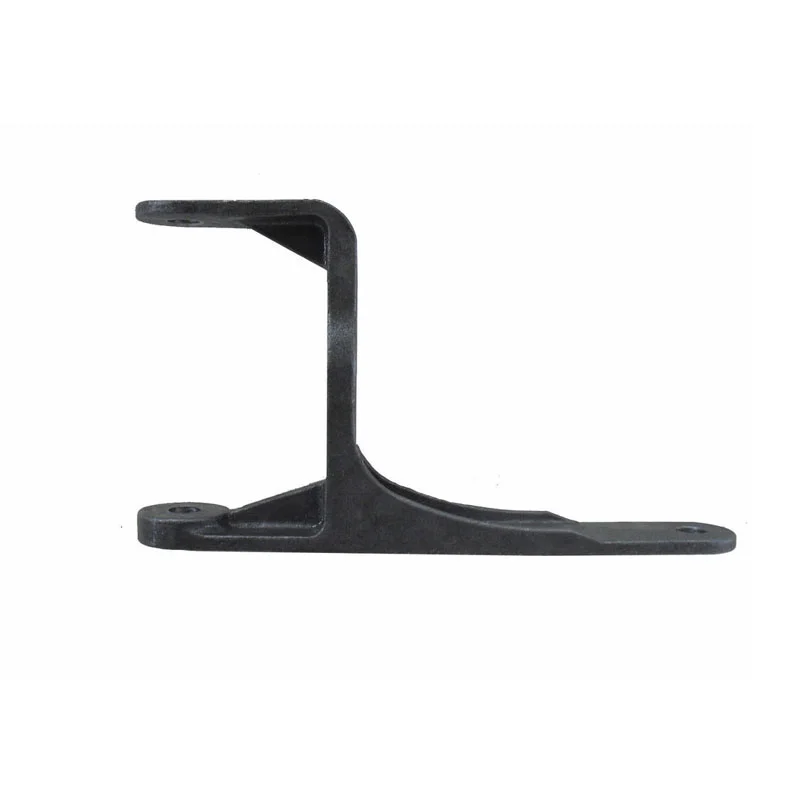
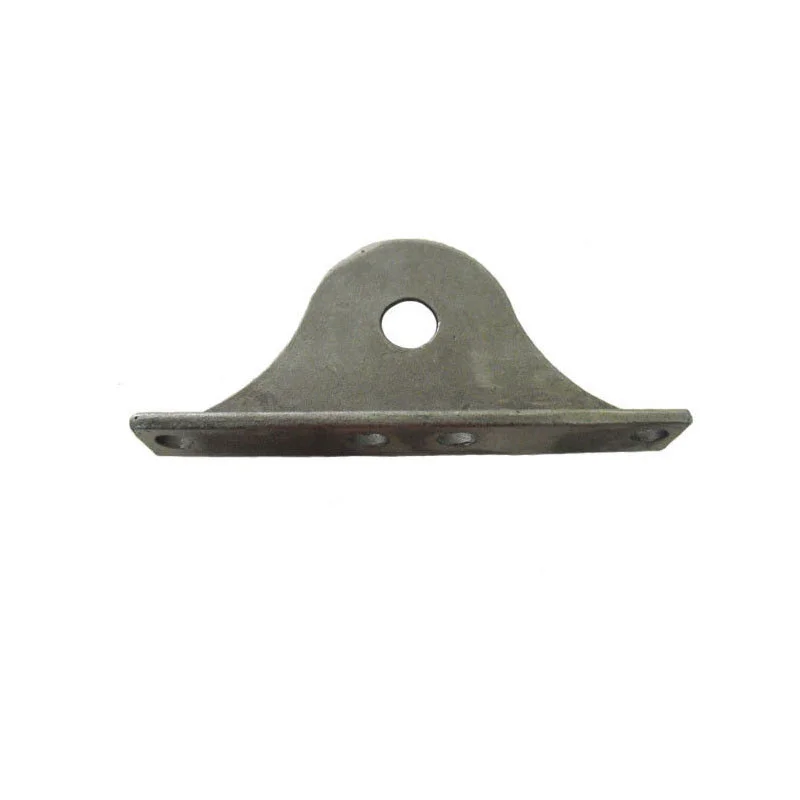
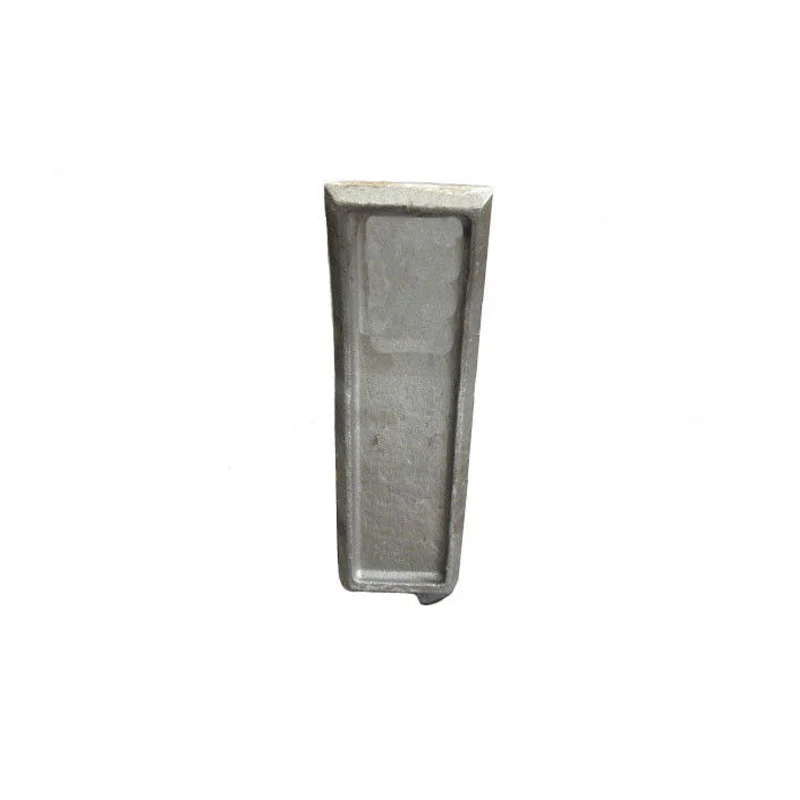
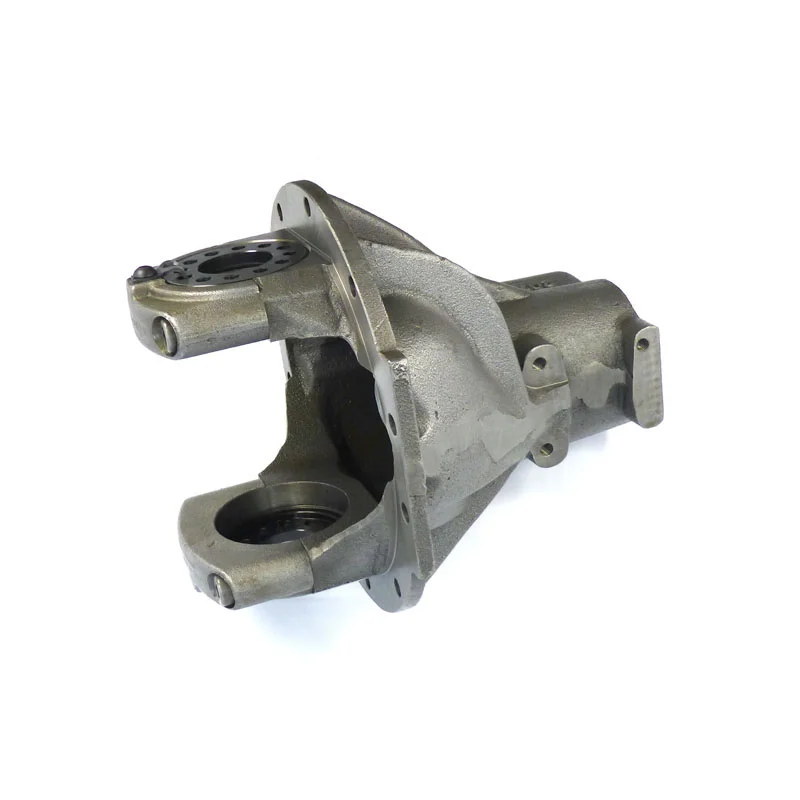
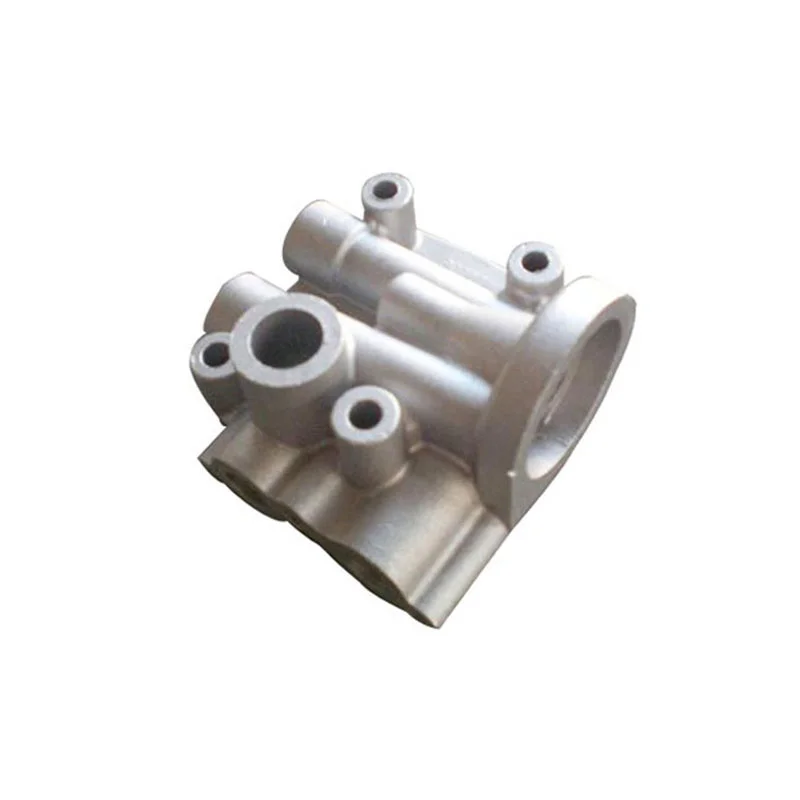
Custom Aluminum Die/Investment Lost-Wax Casting | CT4–CT8, ±0.02mm Machining and Ra3.2–Ra6.3 Roughness
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishSandblasted , Polished
-
MaterialStainless Steel,Steel,Brass,Copper,Aluminum,Iron,Plastic
-
TechnologyInvestment Casting,Sand Casting,Machining,Welding,ForgingMachiningBroaching,DRILLING,Milling,Turning,Tapping,Wire
-
ProcessMolds,Casting,Deburring,Machining,Surface Treatment,PackingWeightAvailable from 0.01 Kg-10T
-
StandardISO,GB,DIN,JIS,ANSI,BSW,ASTM,ASME,BS,API,ENCasting ToleranceCT4-CT8
-
Machining Tolerance+/-0.02mmSurface TreatmentPolishing, Passivating, Sandblasting, Zinc plating, Oxide black
-
CertificationIS09001: 2015,TUV
Customized aluminum die-casting and investment/lost-wax inquiries cover the actual route selected for the component. The casting-tolerance reference is CT4–CT8, while machining tolerance is ±0.02 mm. Roughness is referenced as Ra3.2–Ra6.3, with its unit and measurement basis to agree for the required surface.
Selected material and manufacturing route
Material capabilities cover stainless steel, steel, brass, copper, aluminum, iron and plastic work. Technology directions include investment casting, sand casting, machining, welding and forging. Choose the actual material and route for the component, identifying the geometry and intended function that the manufacturing scope needs to address.
Machining operations and the work sequence
Machining choices include broaching, drilling, milling, turning, tapping and a Wire operation whose actual meaning should be defined. Select the operations required for the chosen material and component geometry. Work stages cover molds, casting, deburring, machining and surface treatment. Relate the selected stages to the finished areas and interfaces needed on the actual part.
Casting class, machining tolerance and roughness
Agree the dimensions governed by CT4–CT8 and those governed by the ±0.02 mm machining reference. Define the process stage and measurement criteria for each group. Assign the Ra3.2–Ra6.3 reference to the actual surfaces with its required unit and inspection basis, connecting casting, machined fit and surface acceptance in the component definition.
Five surface treatments and standard references
Finish directions include polishing, passivating, sandblasting, zinc plating and black oxide, selected for the actual material. Standard references are ISO, GB, DIN, JIS, ANSI, BSW, ASTM, ASME, BS, API and EN. Identify the applicable material, dimensional and finish requirements within those reference families. Agree the actual component acceptance with the chosen manufacturing route and surface work.








