
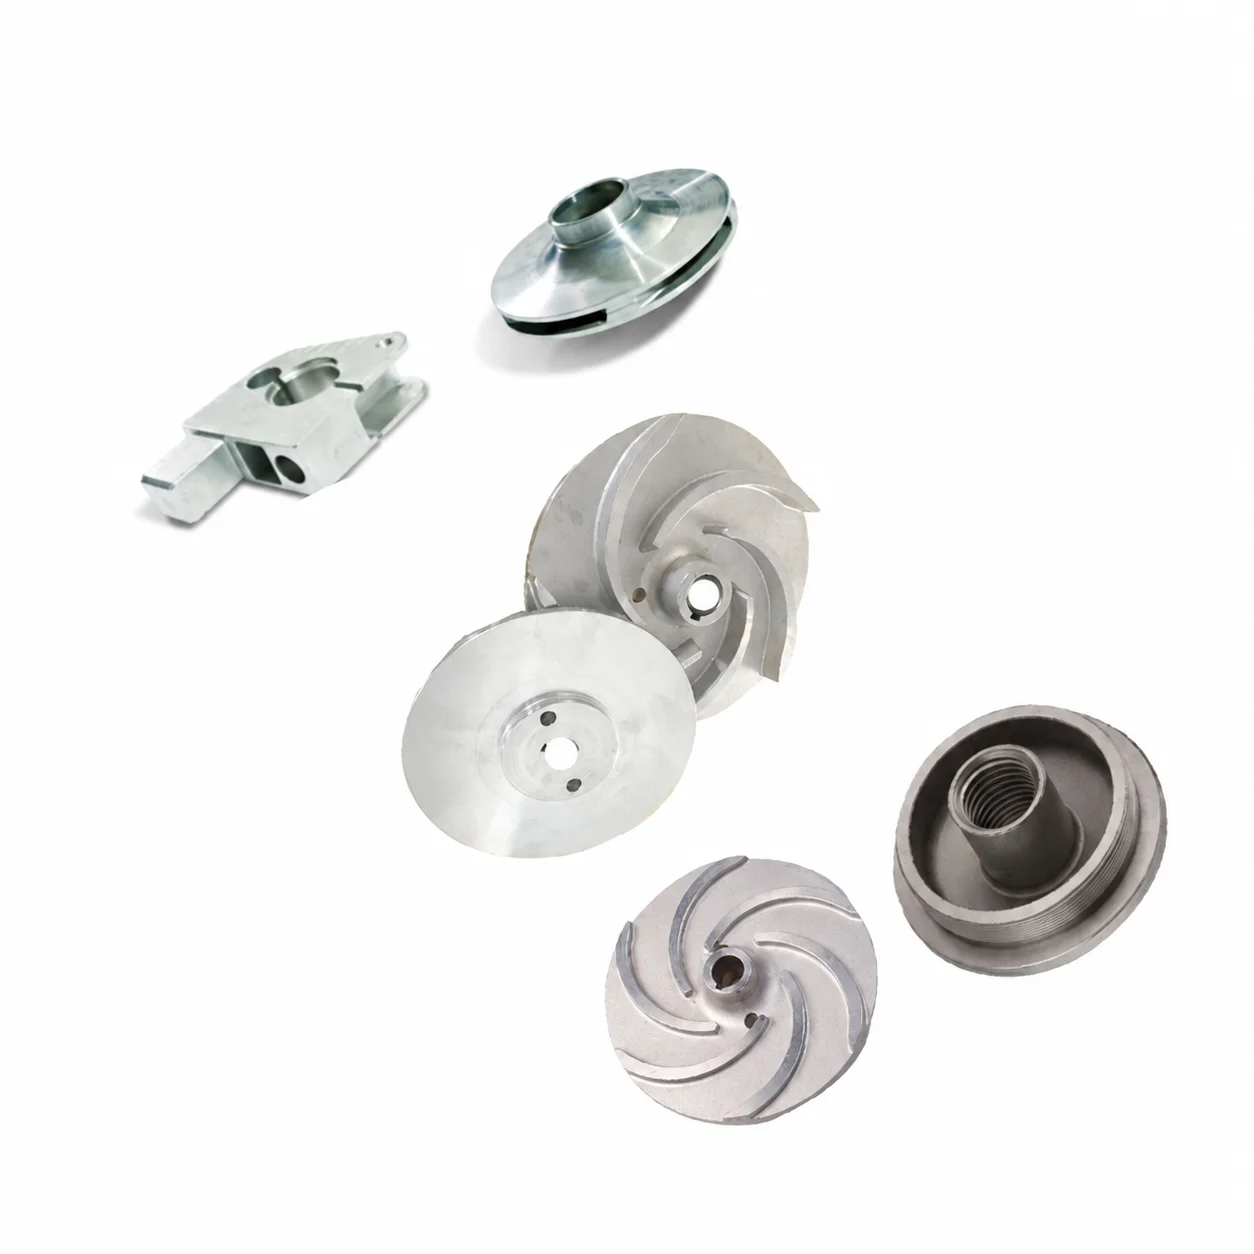
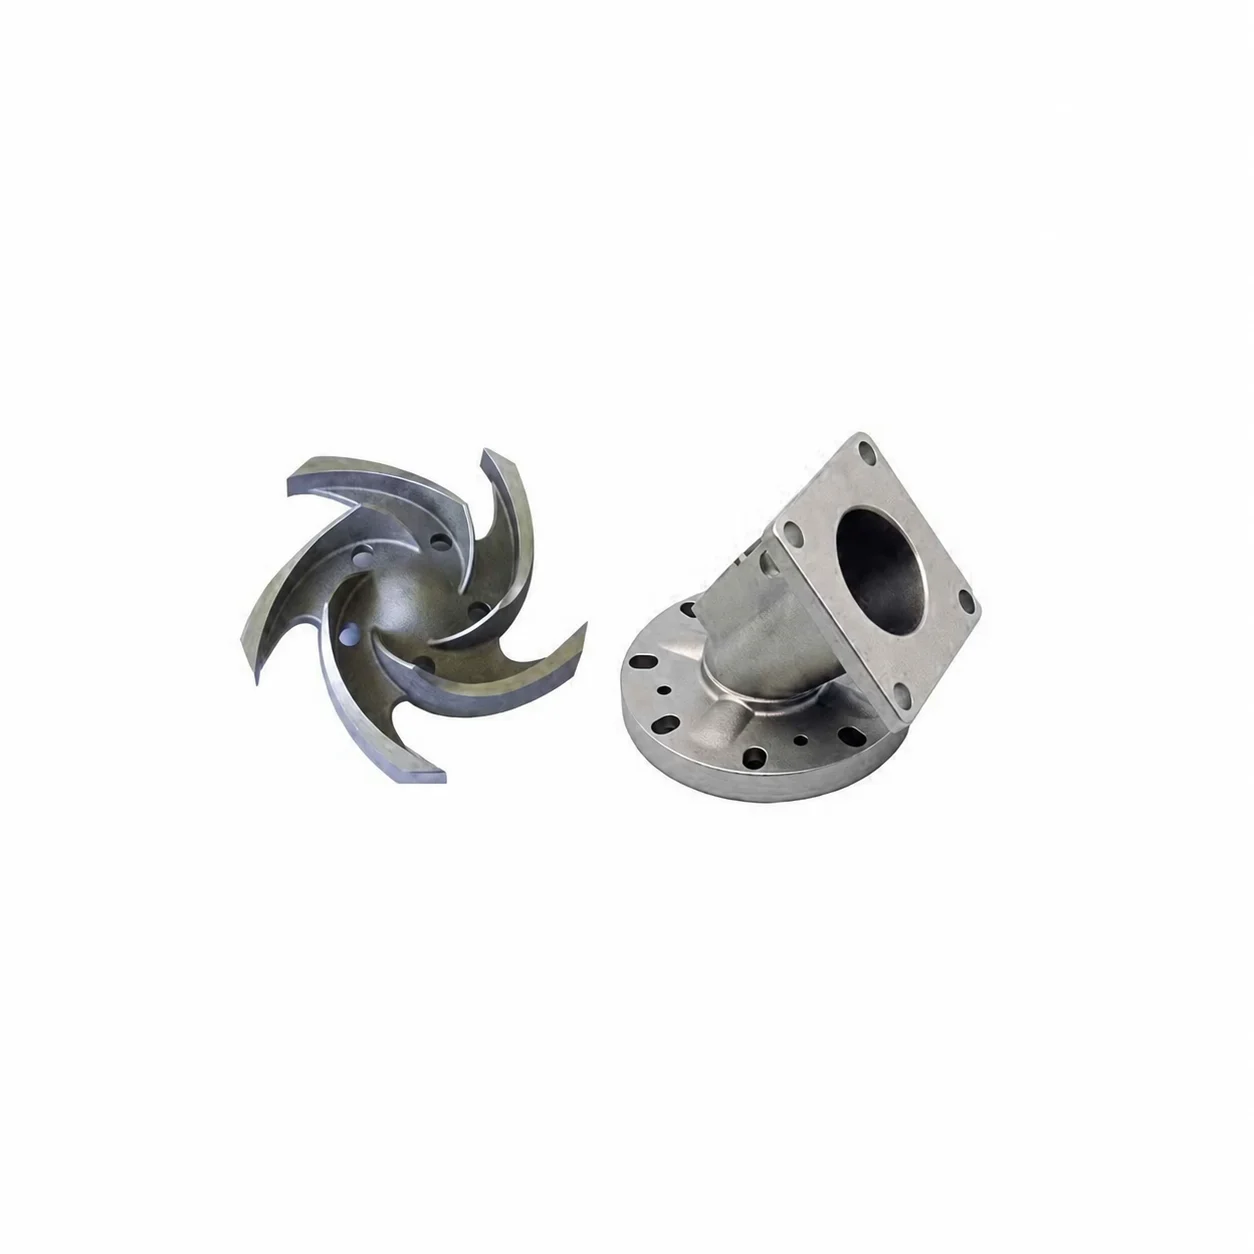
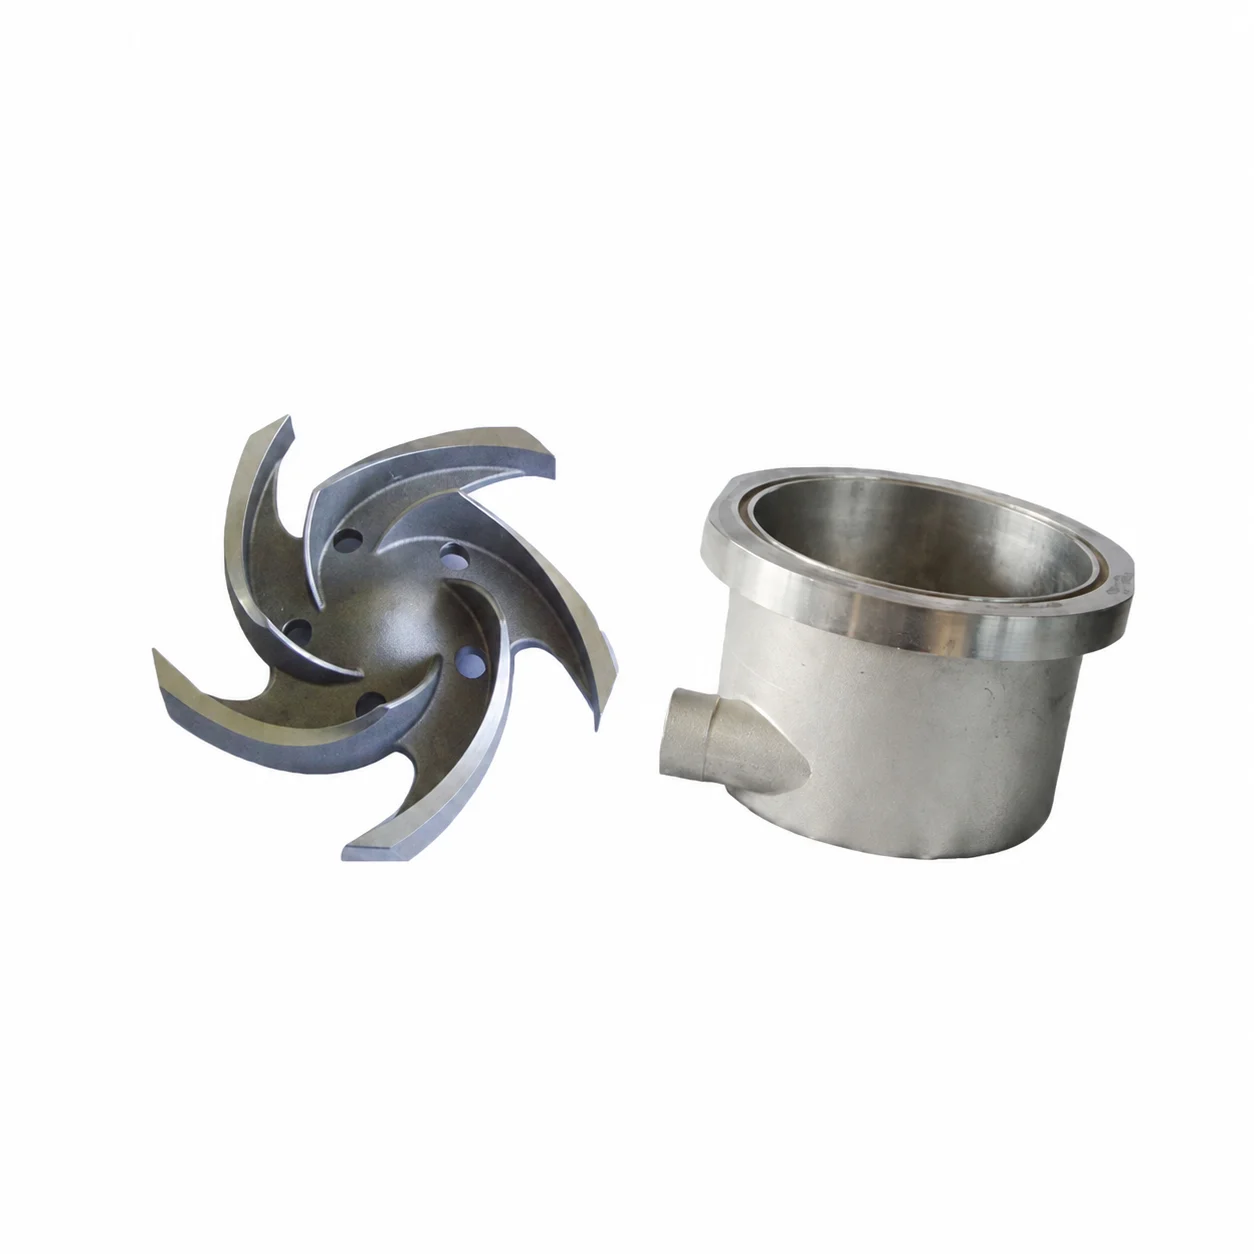
304/304L/316/316L Stainless Pump Impellers, Silica Sol Lost Wax Investment Casting with CNC Machining
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Component FormImpeller / RotorSurface FinishPassivated , Polished
-
Alloy Grade316 , 304L , 304
-
SizeCustomized Size
-
Surface TreatmentPassivation, Brush Polishing, Mirror PolishingMaterials304/304L/316/316L Stainless Steel
-
Product nameInvestment Precision Casting with MachiningMaterial304/316/304L/316L Stainless Steel
-
ProcessLost WaxingSurface treatmentPassivation, Brush Polishing, Mirror Polishing
-
ServiceODM/OEMMachiningCNC machining
-
Surface RoughnessRa3.2-6.3μmMachining Precision0.01mm
-
CertificationTUV ISO,SGS,OHSASToleranceCT4-CT6
Custom stainless steel pump impeller requests are offered through silica sol lost wax investment casting and CNC machining. Material choices are 304, 304L, 316 and 316L, with OEM and ODM service and customized size. Select the actual impeller grade and geometry around the pump application.
Pump duty and impeller definition
Describe the pump fluid, temperature, pressure and rotational duty for the component being selected. Use the impeller drawing to define the geometry and the features important to the intended assembly. Agree the actual material and functional acceptance for that duty before approving the custom casting. Identify the impeller interfaces that control fit within the intended pump assembly.
Casting tolerance and CNC precision
The casting-tolerance reference is CT4–CT6, while machining precision is 0.01 mm. Allocate those separate references to the relevant cast and CNC-finished features, with the required tolerance form to agree. Keep the stage and feature definition clear when specifying the dimensional inspection records needed by the pump project.
Surface roughness and three finish choices
Surface roughness is referenced as Ra3.2–6.3µm. Identify the surfaces to which that range applies and agree the measurement method and final condition for those areas. Passivation, brush polishing and mirror polishing are offered surface-treatment choices. Select the actual method for the chosen grade and impeller duty, then define how its finished appearance and surface requirements will be accepted.








