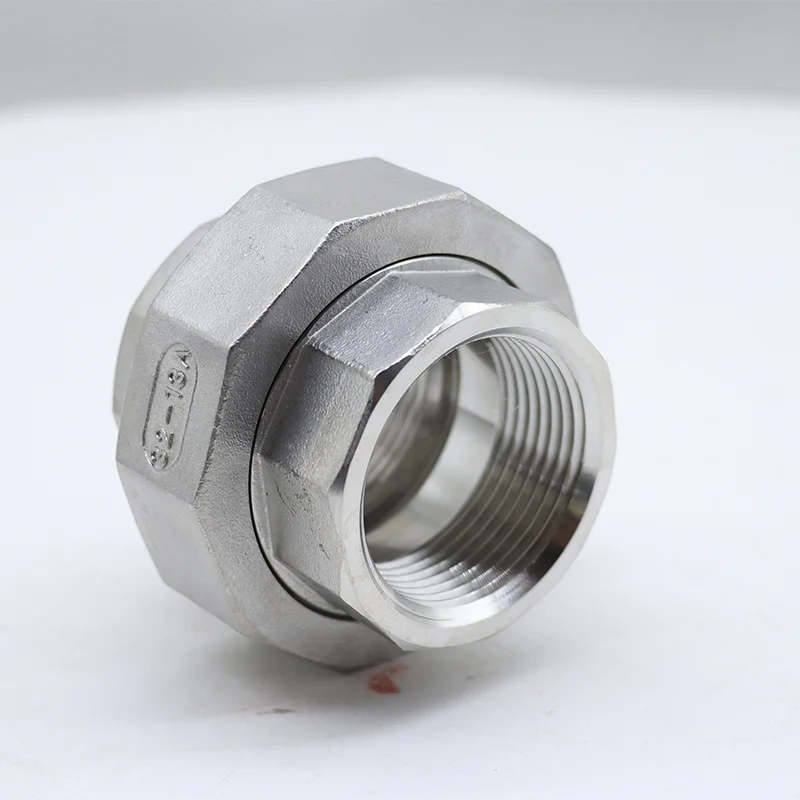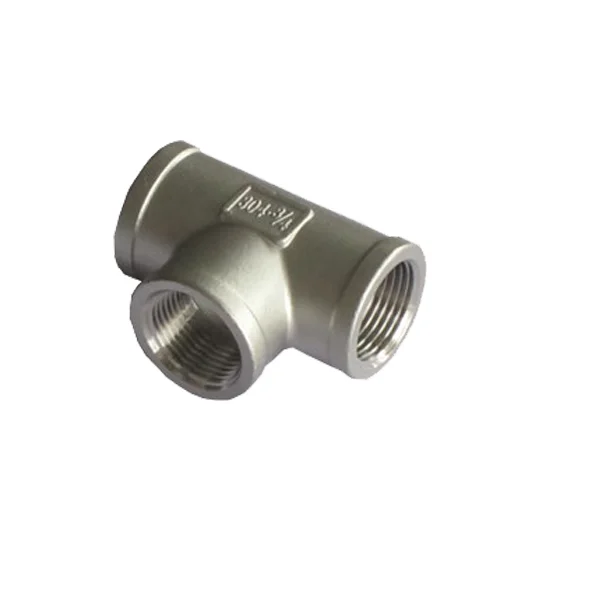
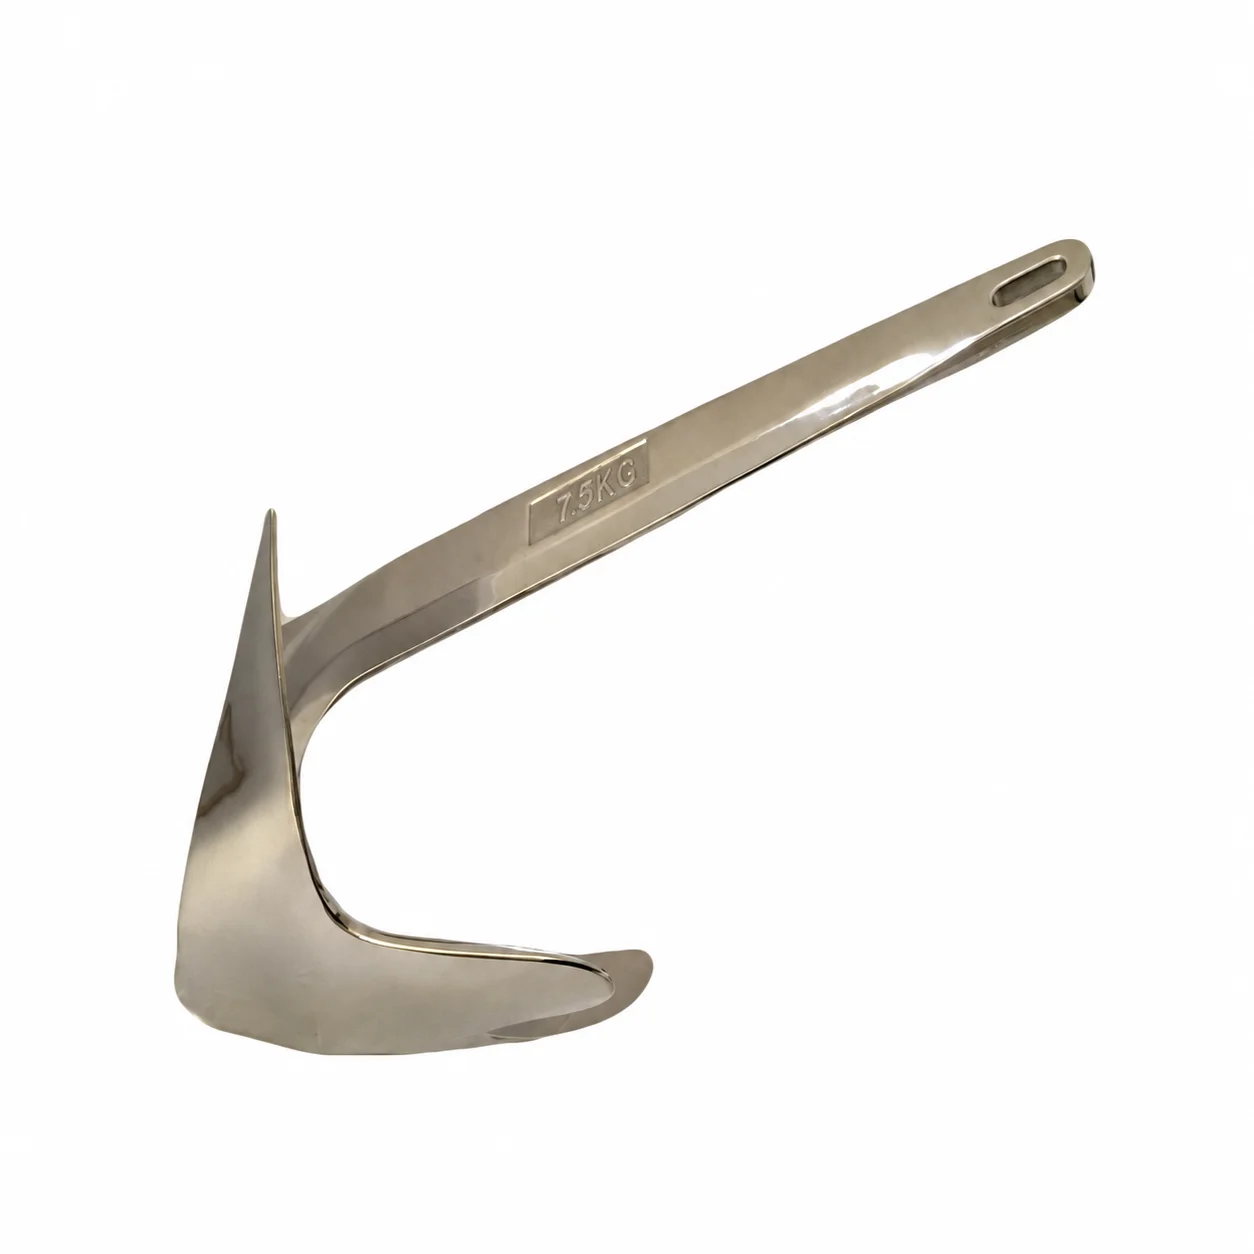
Stainless-Steel Lost-Wax Investment-Casting Services | Water-Glass/Silica-Sol Routes, CNC and Zinc/Mirror Finishes
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishPlated , Polished
-
Product nameInvestment Casting
-
MaterialStainless Steel,Alloy steel,carbon steelManufacturing Area (sqm)10000
-
Machining EquipmentCNC, Lathe, Milling machine, Drilling, etcStandardASTM, DIN, ISO, BS, JIS, etc
-
Weight Range0.01 KG to 20 KGHeat TreatmentNormalizing, Tempering, Hardening, etc
-
ProcessWater glass investment casting,Silica sol investmentcastingSurface TreatmentZinc Plating, Mirror Polishing ect
-
Lead Time30 Days
Investment/lost-wax casting services cover stainless steel, alloy steel and carbon steel, with water-glass and silica-sol process directions. Machining equipment includes CNC, lathe, milling machine and drilling. Heat-treatment directions are normalizing, tempering and hardening, with zinc plating and mirror polishing among the surface choices.
Steel designation and water-glass or silica-sol route
Select the actual steel designation and define the component geometry required for its intended use. Agree the investment-casting route within the water-glass or silica-sol directions. Identify the important cast dimensions and interfaces, connecting the material and process choice to the supplied condition and acceptance needed for that particular component.
Machining areas and applicable standards
Define the interfaces requiring CNC, lathe, milling or drilling work. Reference standard families are ASTM, DIN, ISO, BS and JIS. Agree the actual material and dimensional requirements within that scope, including the measurement basis for controlled areas. Relate those criteria to the selected casting geometry and finished fit needed for its function.
Normalizing, tempering and hardening requirements
Select the heat-treatment direction appropriate to the chosen material and component. Define the required material condition and acceptance after the selected work. Connect those requirements to the actual part geometry, machining areas and intended duty, establishing what the treated casting needs to meet within the manufacturing request.
Zinc-plated or mirror-polished surfaces
Identify the actual surface direction and the areas requiring it. Agree the required appearance and surface condition for the selected steel. Define the dimensional and visual checks after treatment, relating them to important machined interfaces and the supplied component geometry. This connects the chosen finish to the finished-part acceptance for the requested casting.