
Small Inconel 718 and 304/316L Ceramic Core Castings | Heat-Resistant Vacuum Investment, Lost-Wax and JIS Enquiries
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishSandblasted , Polished
-
warranty2 Yearsweight (kg)100
-
video outgoing-inspectionProvidedmachinery test reportProvided
-
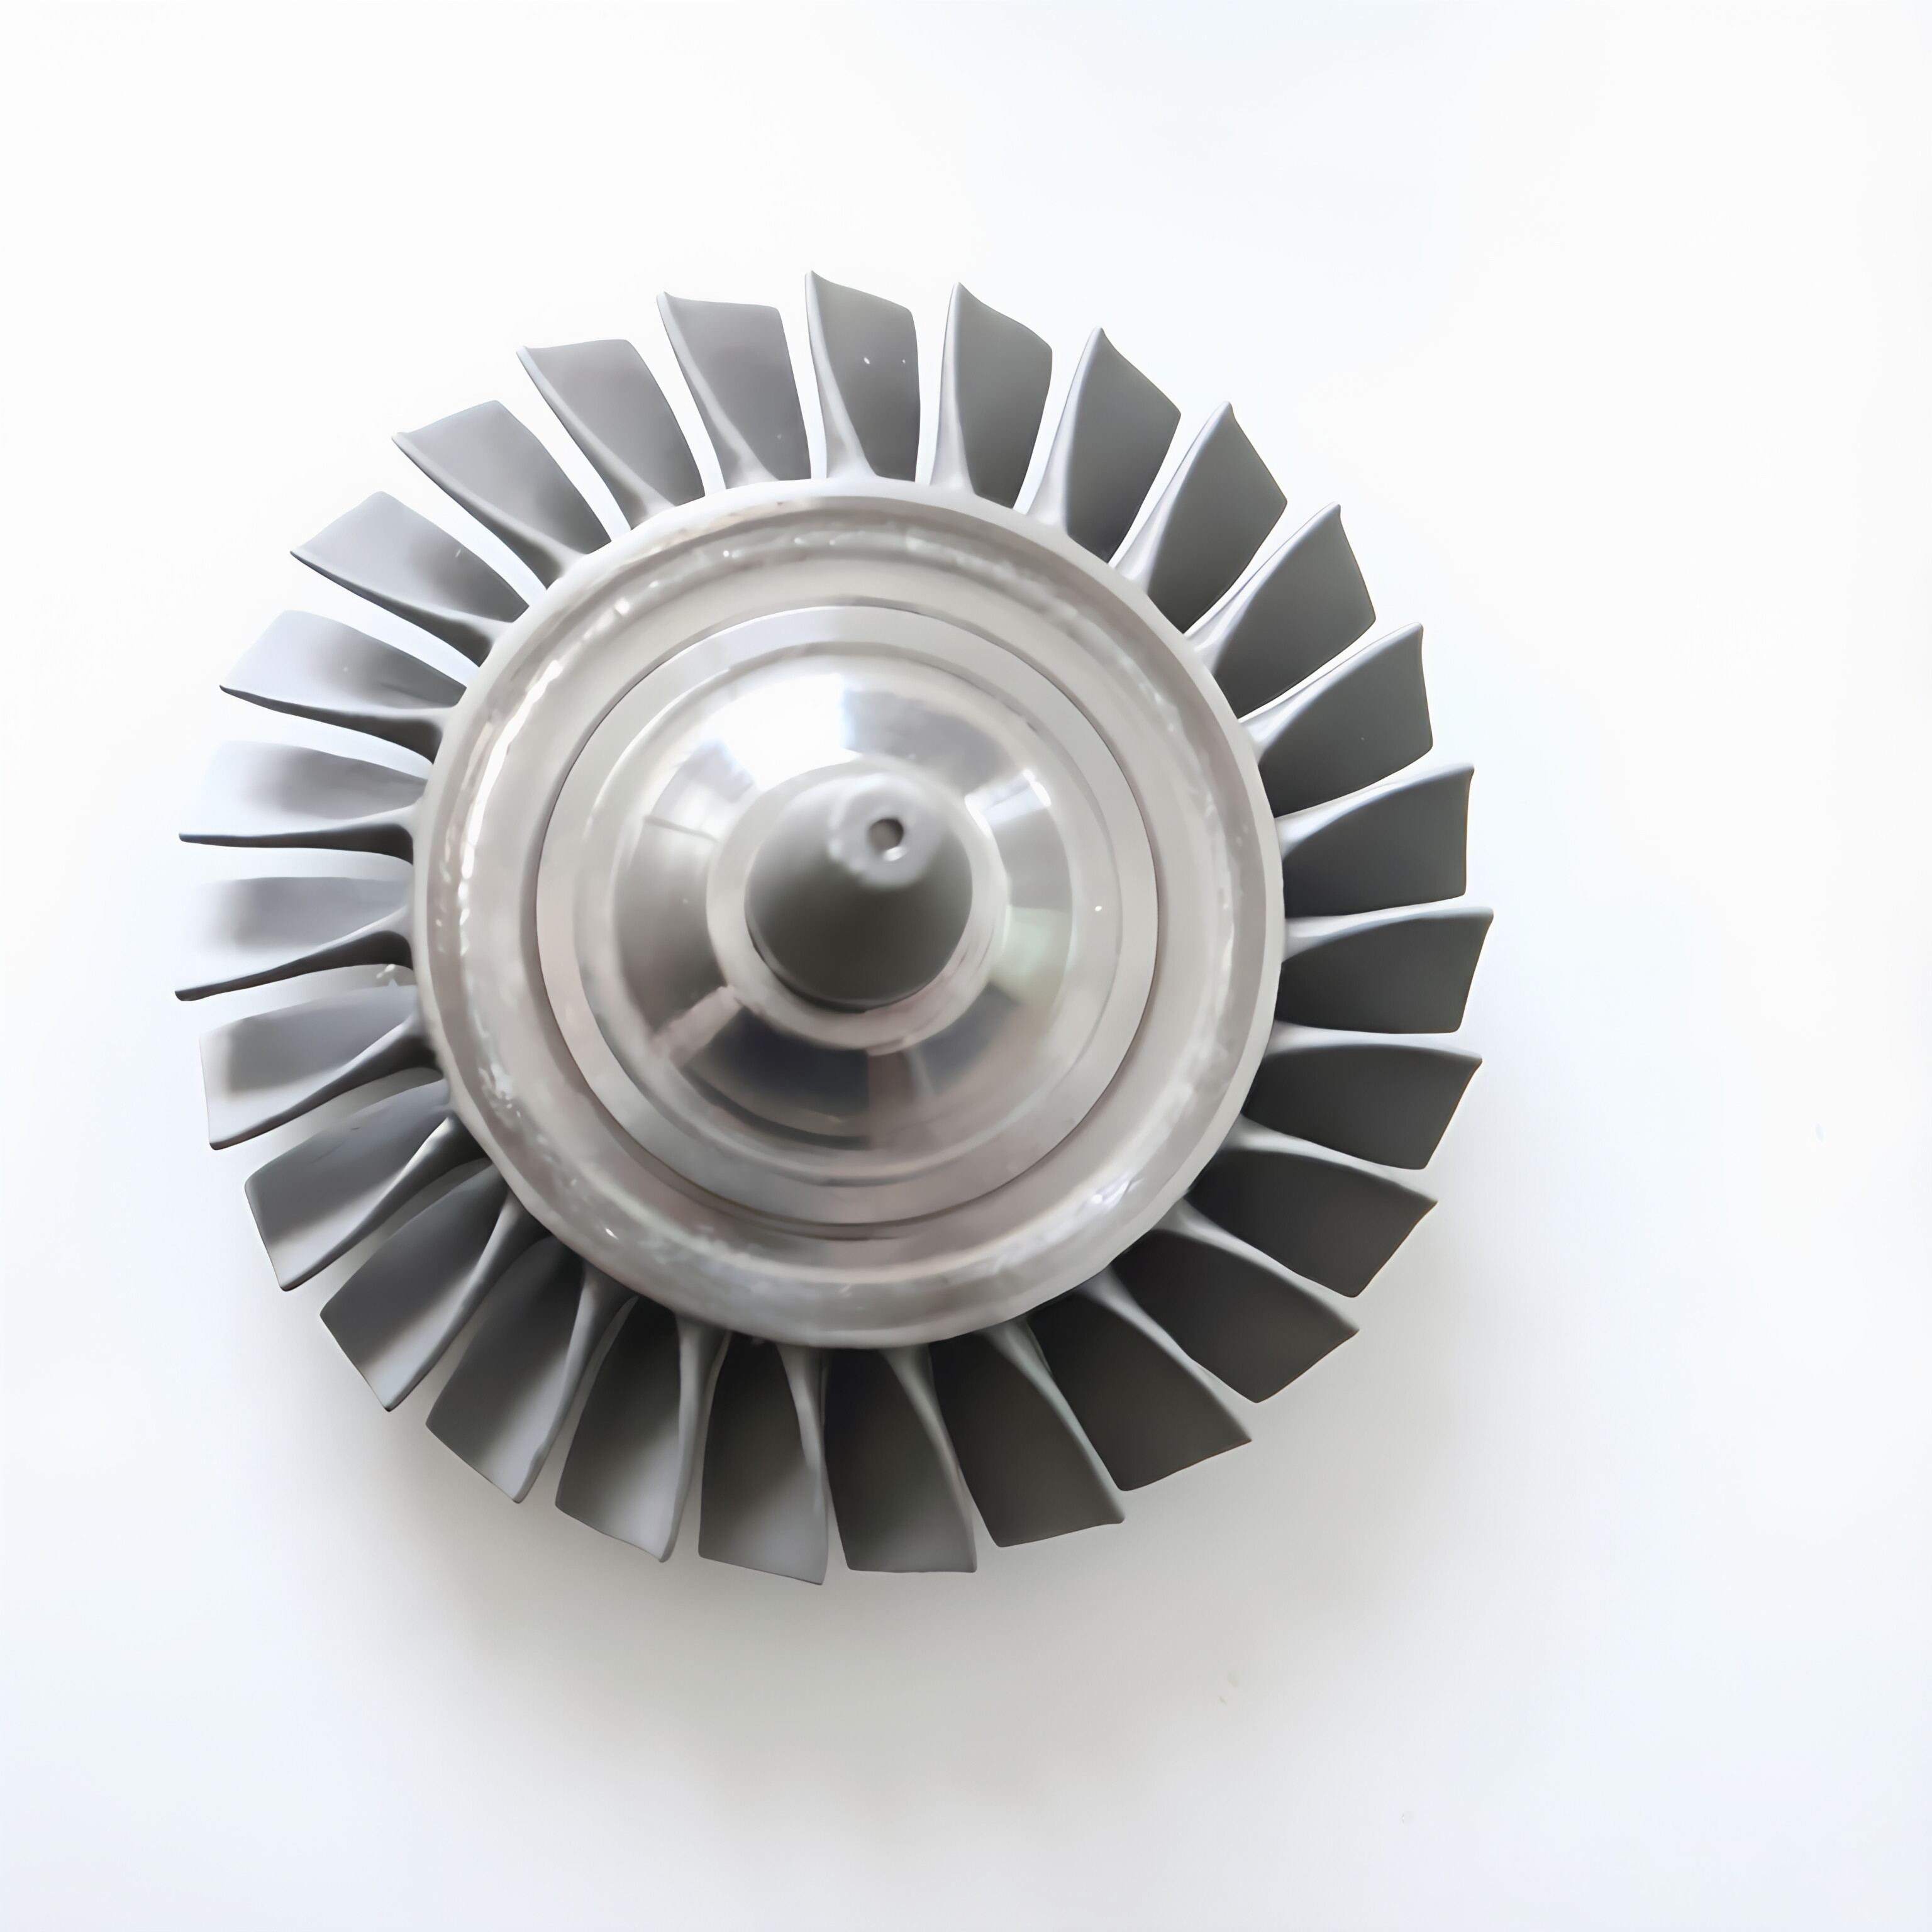
engine typeTurbocharger,Turbine WheeltypeTurbocharger,Turbine Wheel
-
Product TypePrecision Power & Propulsion Components
-
MaterialInconel 718 / 625 / Titanium Alloy / Stainless SteelProcessInvestment Casting / Lost Wax Casting / CNC Machining / HIP
-
ApplicationTurbine Engines / UAV Propulsion Systems / Industrial Power UnitsMax Temperature Resistance≥1000°C (Alloy Dependent)
-
Max Rotational Speed30,000-100,000 RPMTolerance±0.01-0.05 mm (Precision Grade)
-
Surface TreatmentGrinding / Polishing / Sand Blasting / Coating / Heat TreatmentDrawing Format2D: PDF, DWG, DXF / 3D: STEP, IGS, STP
-
PackagingCarton / Plywood Case / Anti-Rust Protection
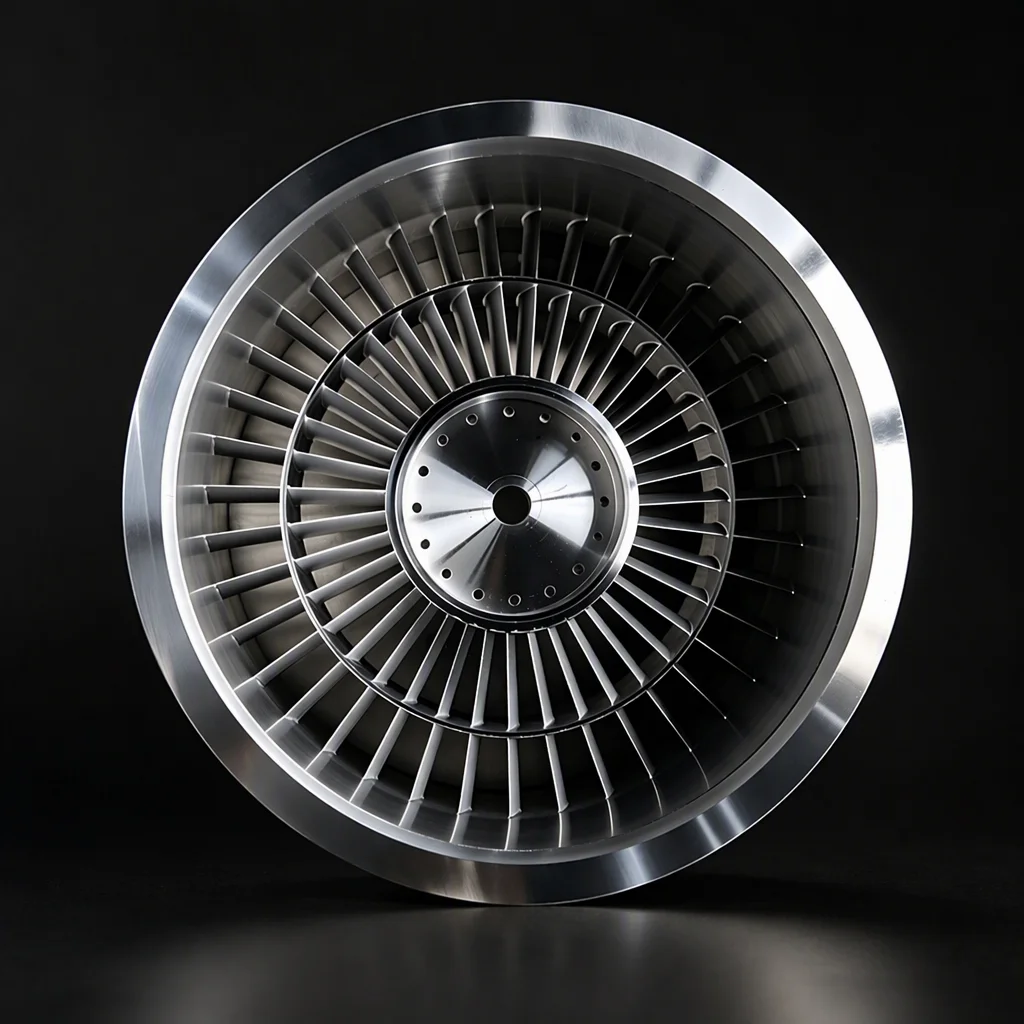
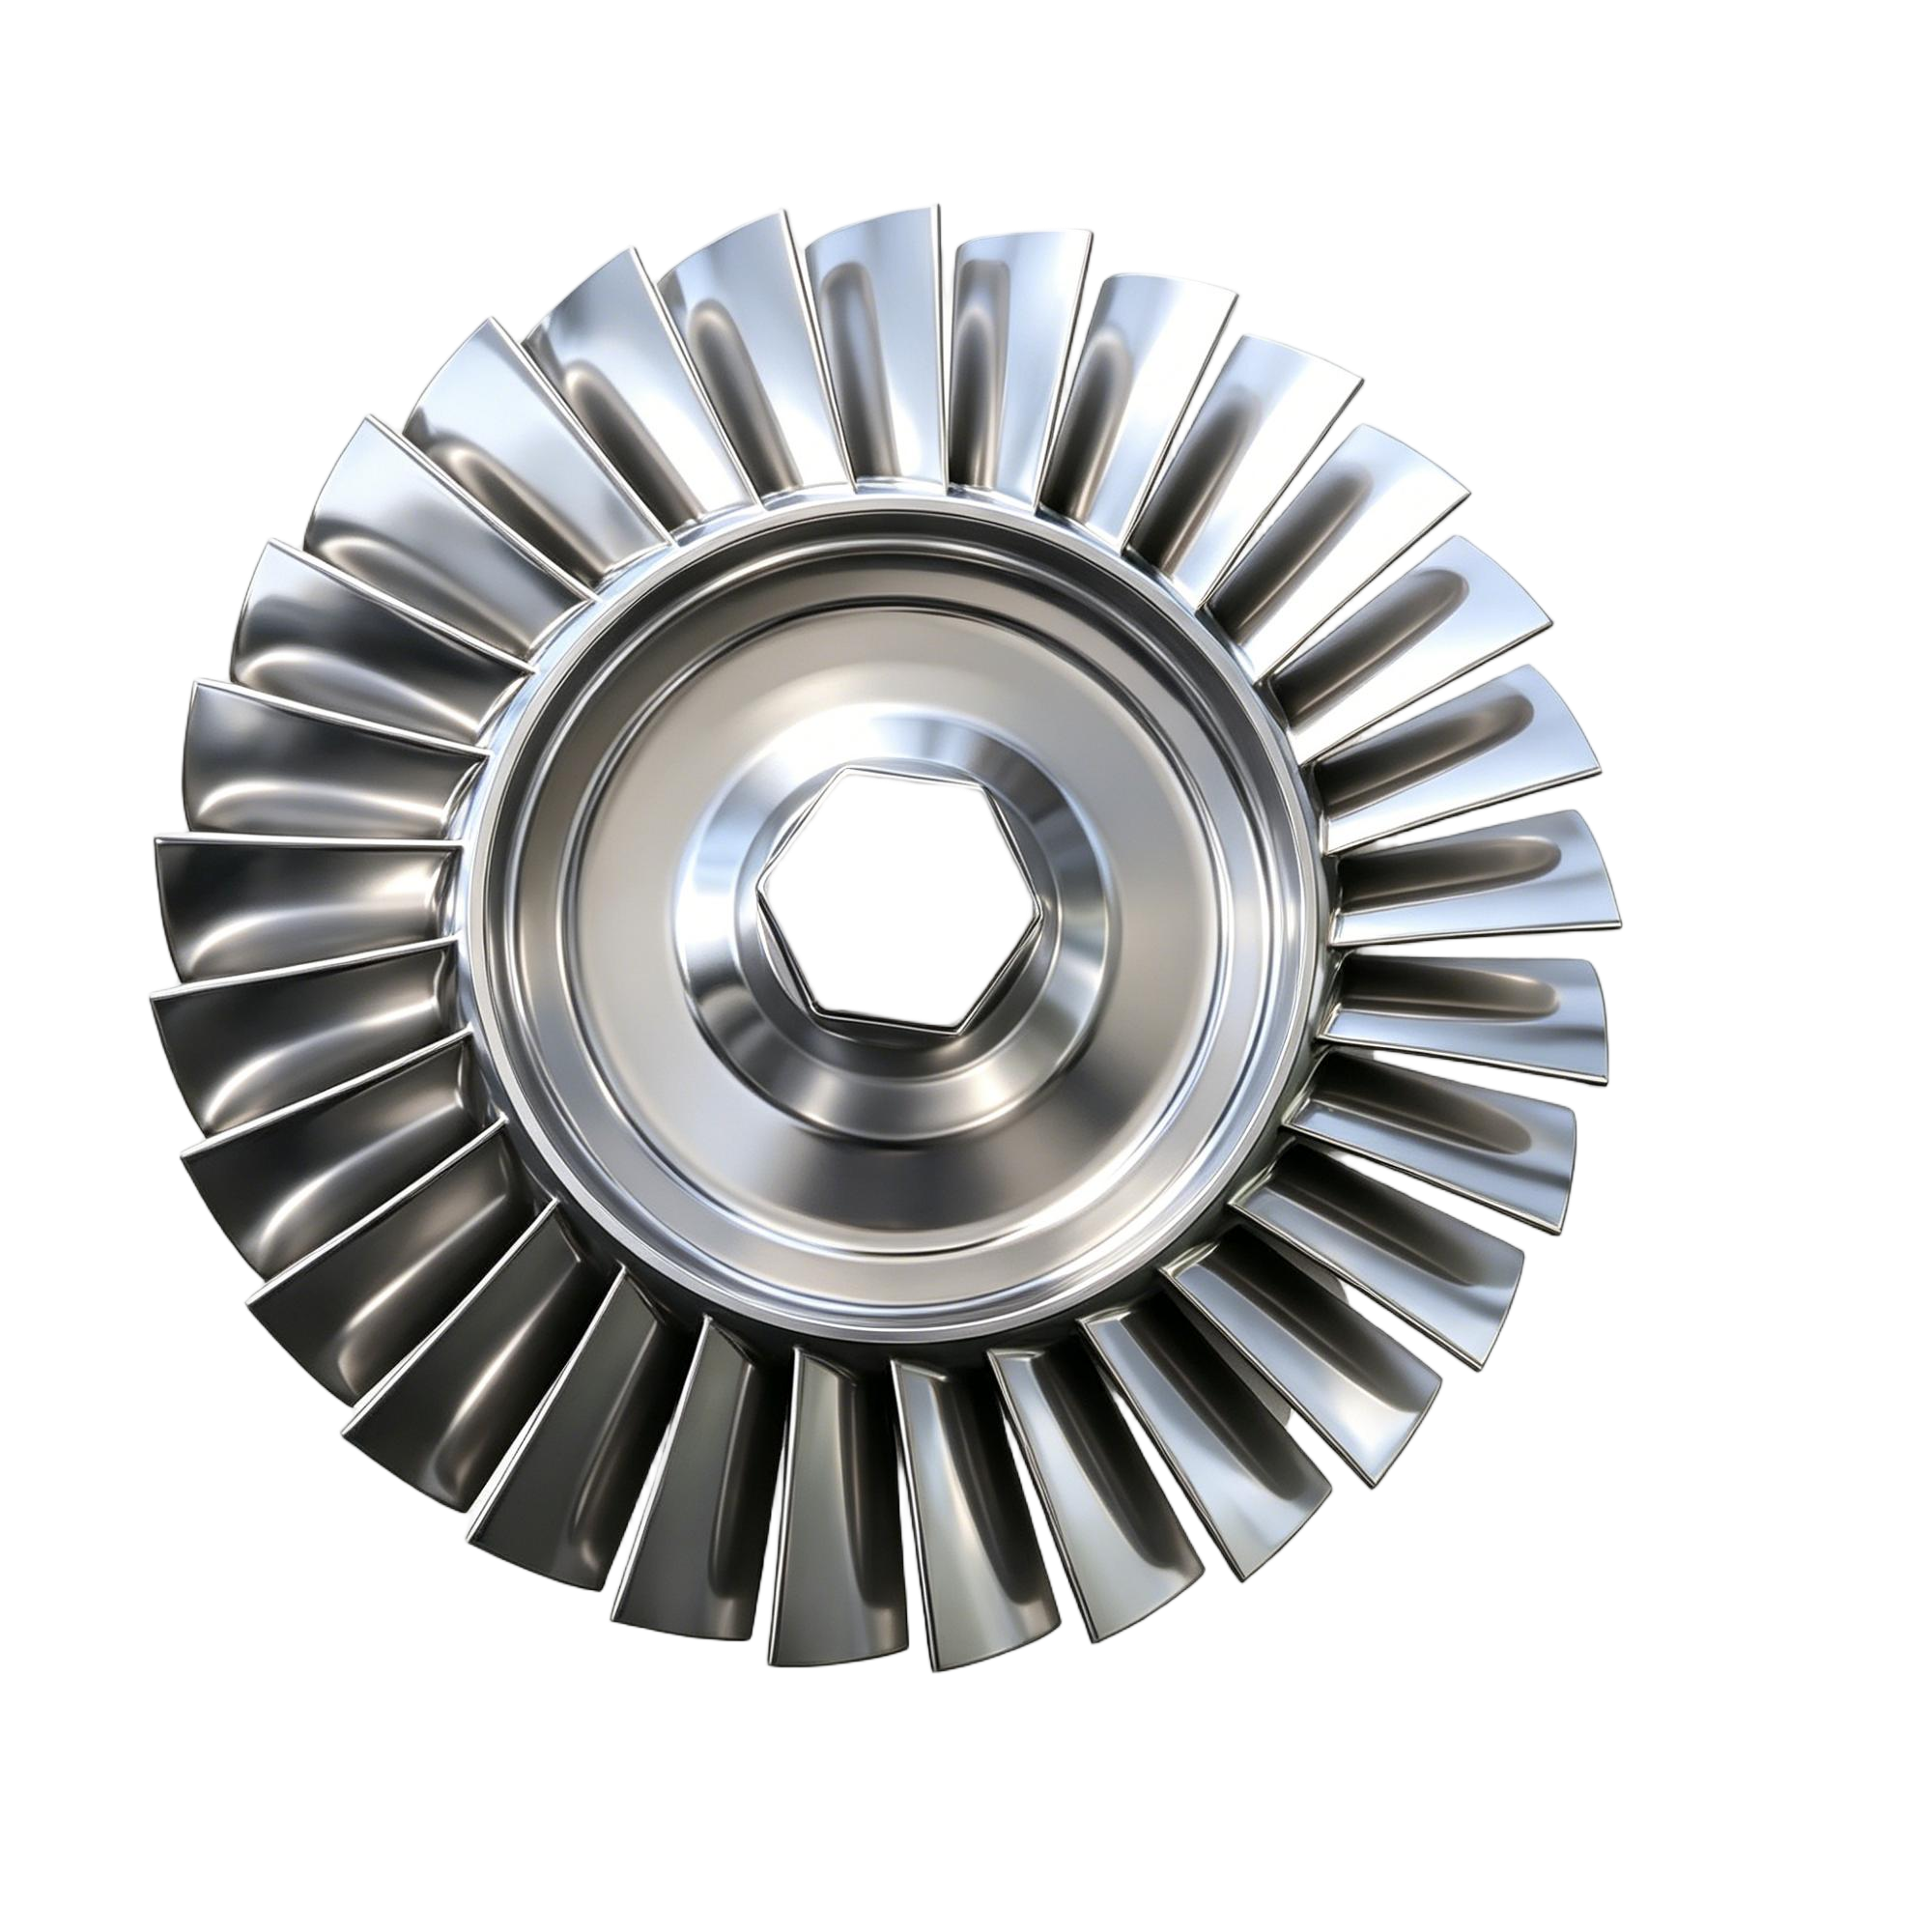
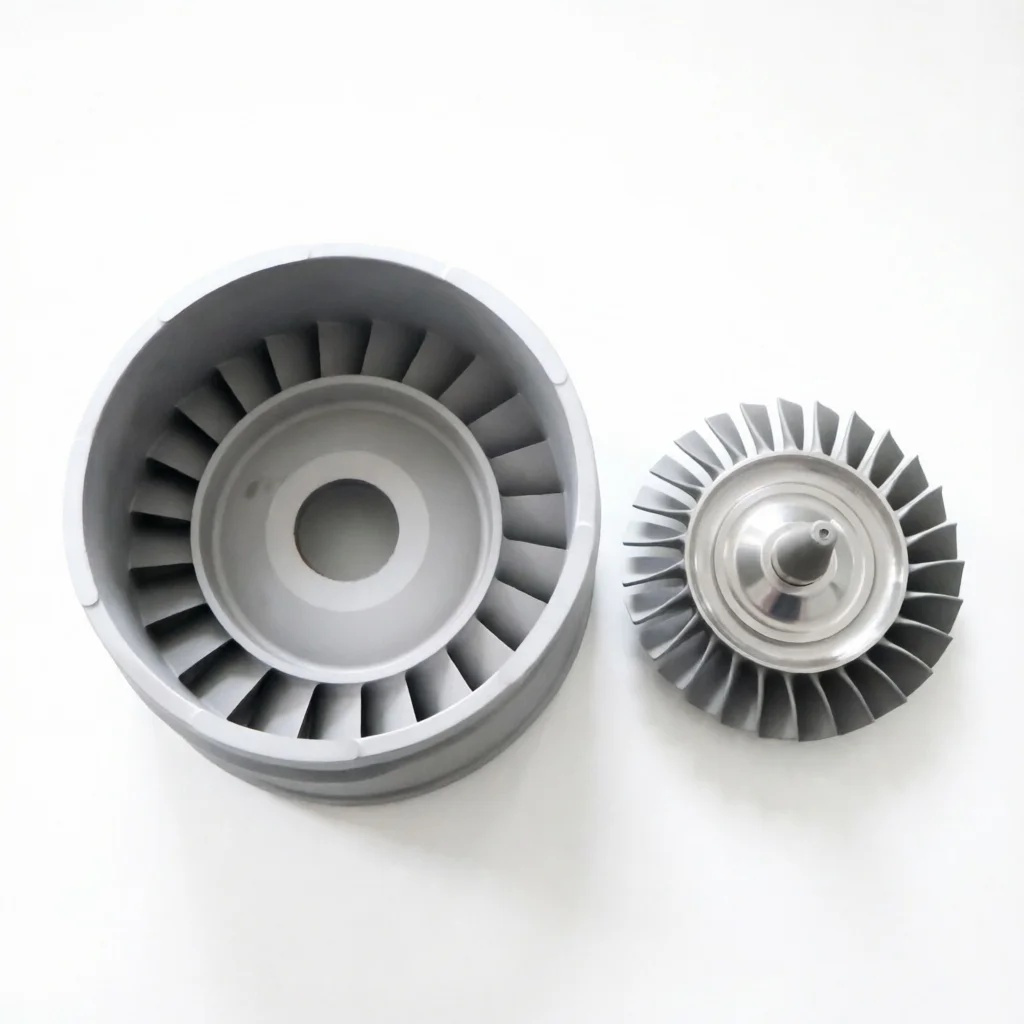
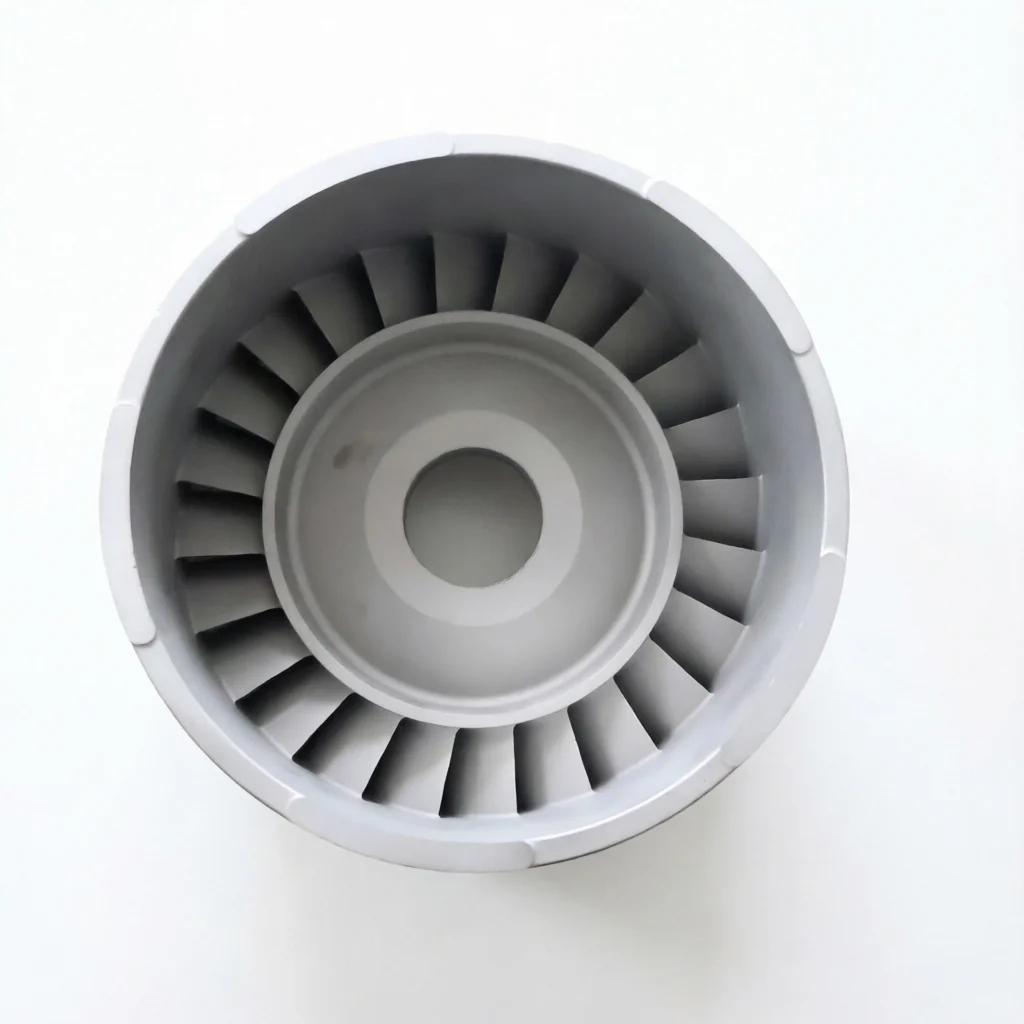
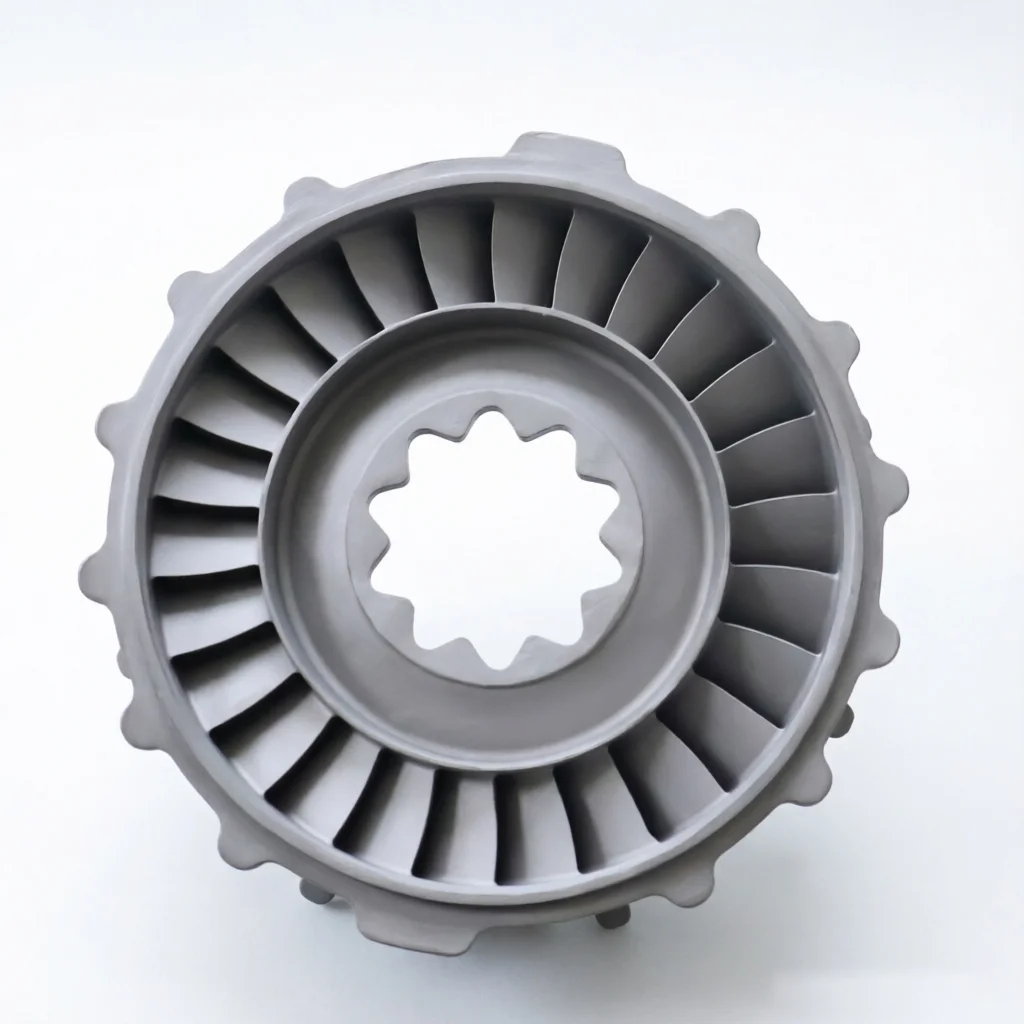
Define a small heat-resistant cast part through its alloy, geometry and manufacturing route. Material directions include Inconel 718 and 625, titanium alloy and stainless steel, with 304/316L enquiries and ceramic-core, vacuum investment and lost-wax casting directions.
Agree the alloy and ceramic-core process requirement
Select the complete material grade for the component and establish the core and casting scope needed for its geometry. CNC machining and HIP are additional process options to discuss. If a JIS requirement applies, identify the complete specification that should govern the selected material and part.
Connect temperature and speed to the chosen component
The temperature-resistance reference is ≥1000°C and is alloy dependent. Rotational speed is referenced at 30,000–100,000 RPM for the component direction. Define the actual temperature and speed requirements for the selected alloy and geometry, together with the acceptance needed for that duty.
Set precision and finished-surface acceptance
A precision-grade tolerance reference of ±0.01–0.05 mm should be connected to the relevant finished features. Grinding, polishing, sand blasting, coating and heat treatment are operations or surface choices to agree for the part. Identify the measurement methods and finished-condition criteria required by the component drawing.
Complete the application and review scope
Turbocharger and turbine-wheel enquiries can address turbine engines, UAV propulsion systems or industrial power units. Define the actual interface and duty for the intended component. A two-year warranty, outgoing-inspection video and machinery test report are offered with coverage and review scope to establish. Drawings can be supplied as 2D PDF, DWG or DXF and 3D STEP, IGS or STP.








