
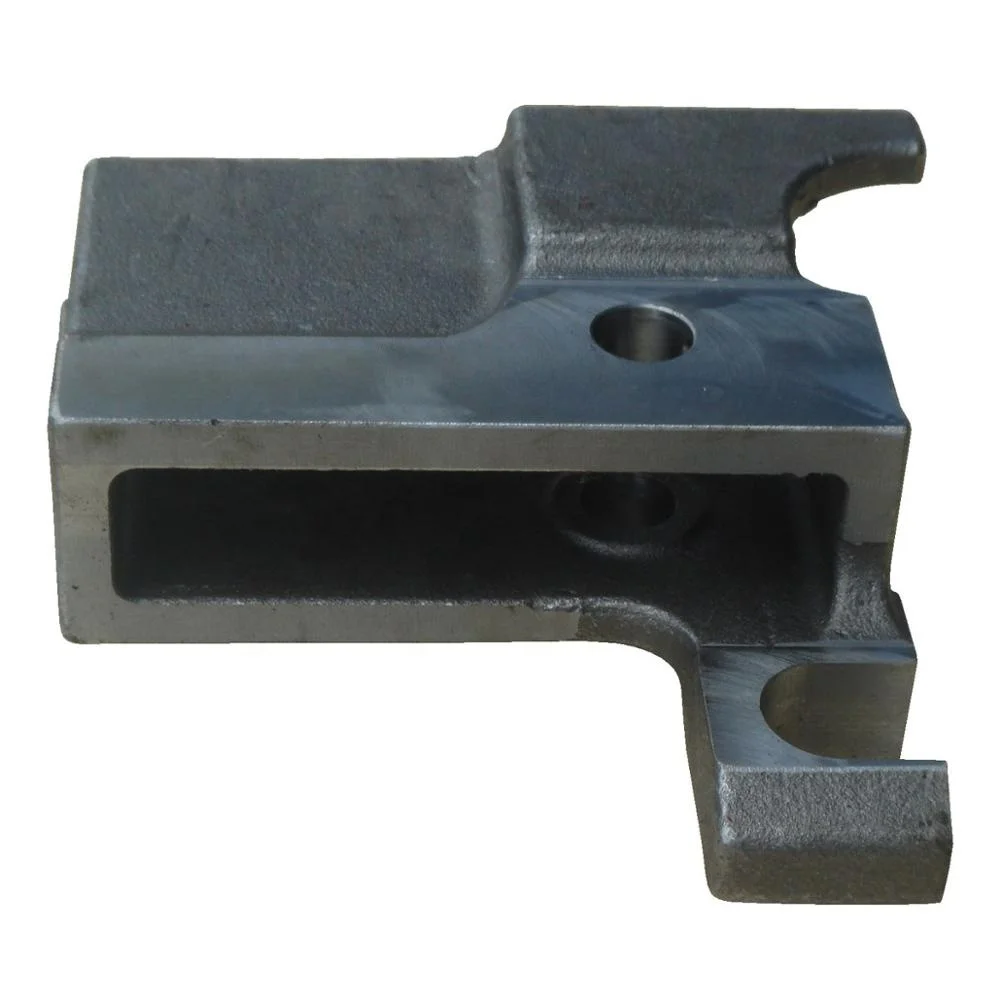
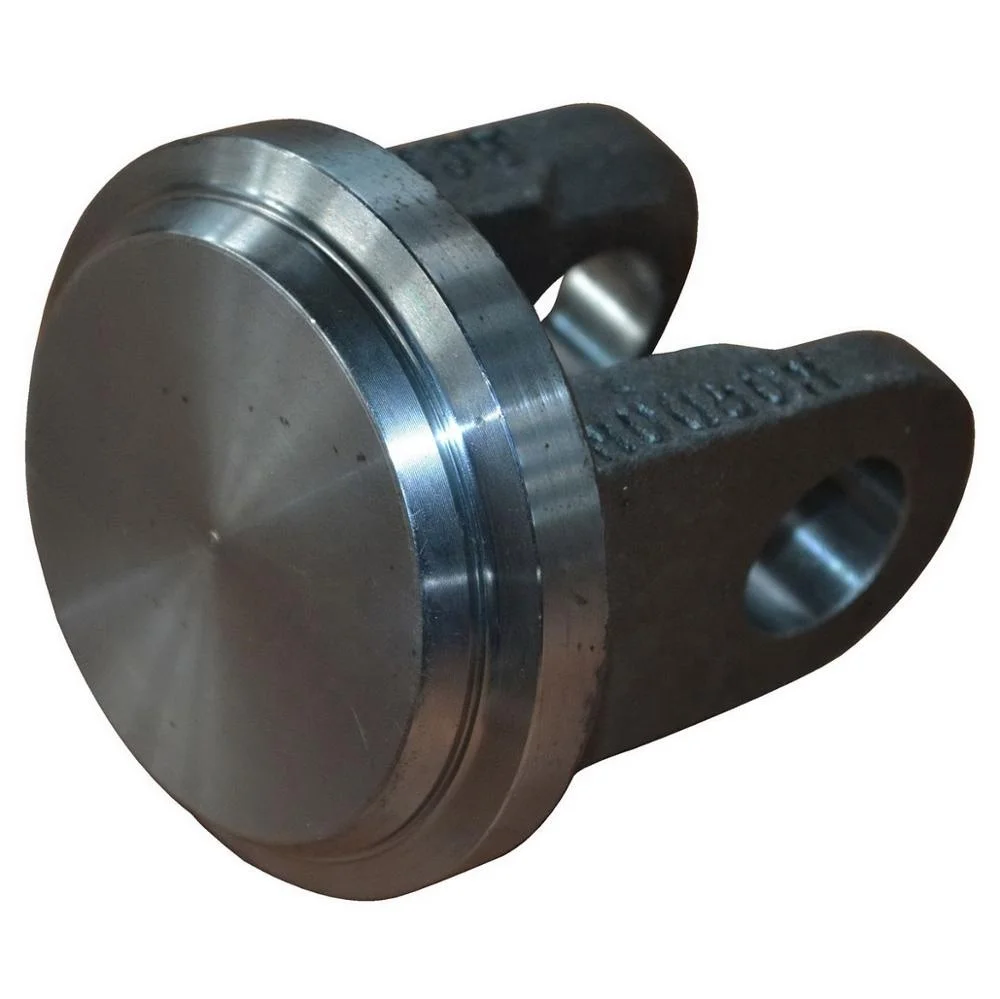
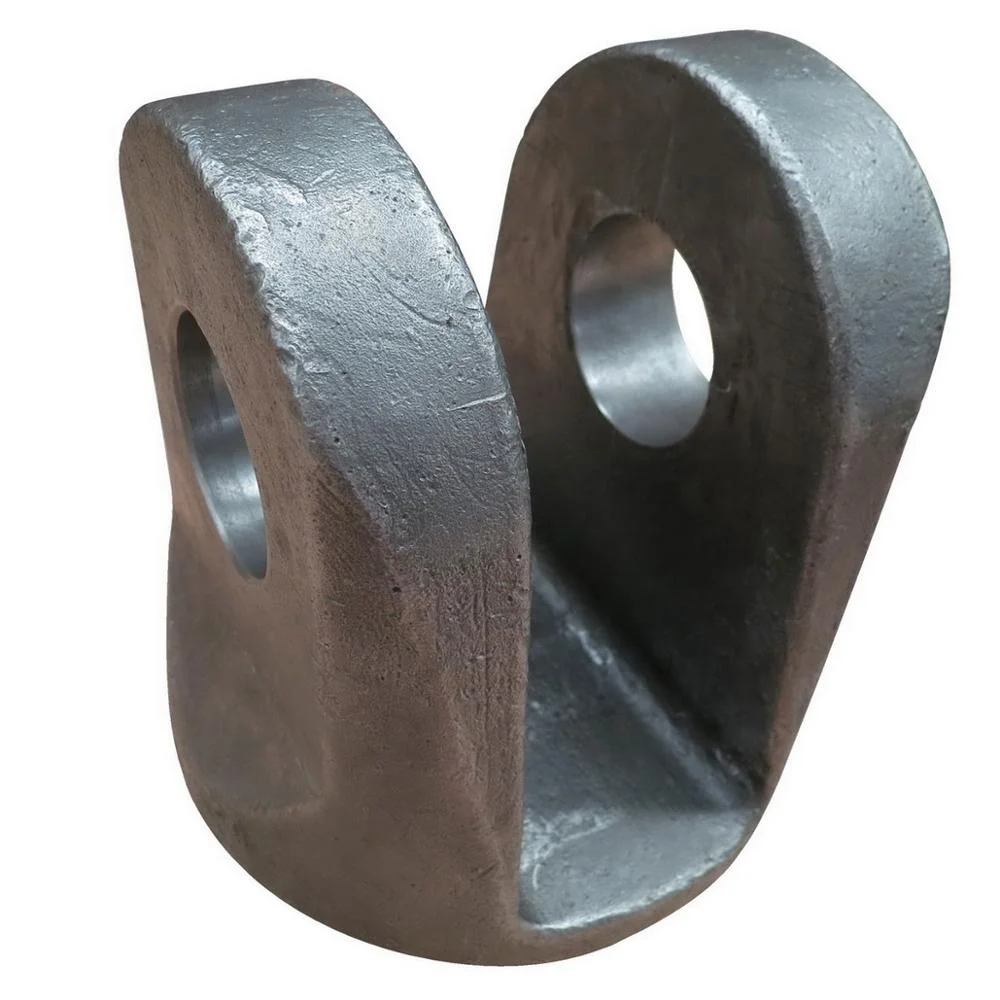
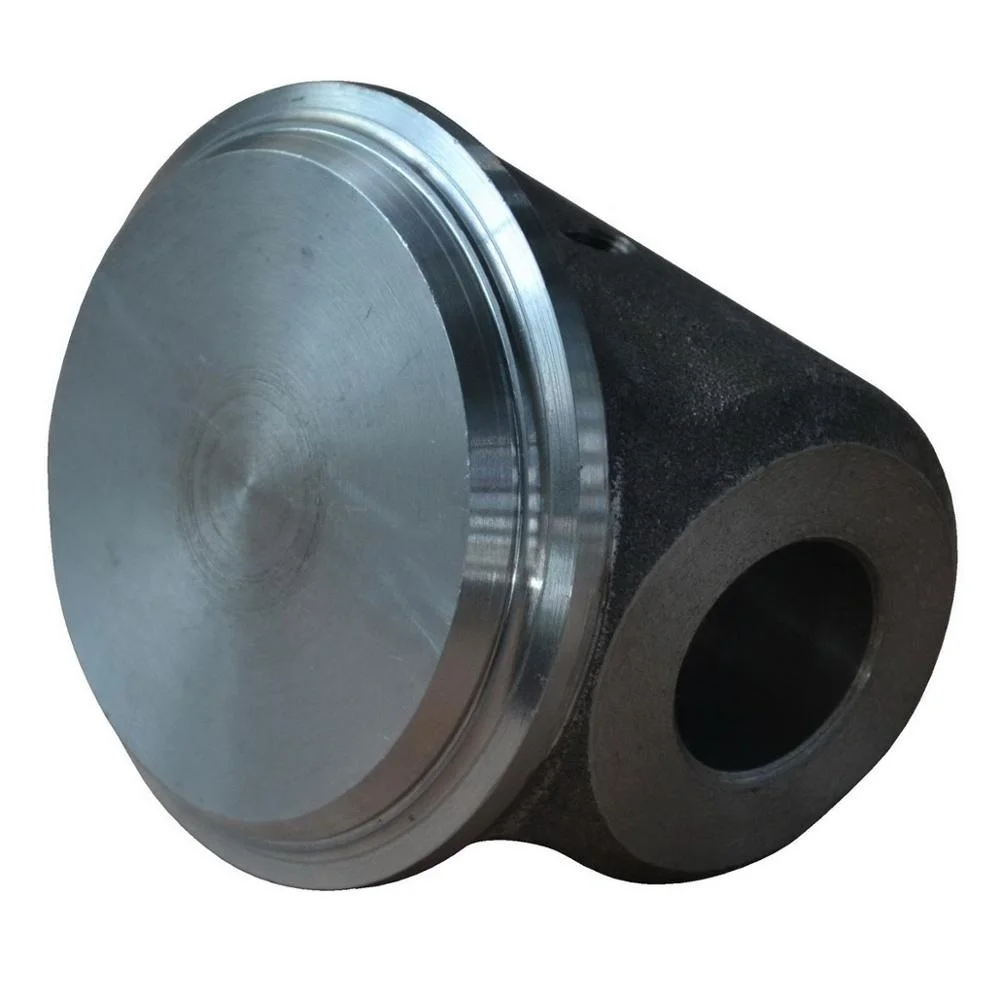
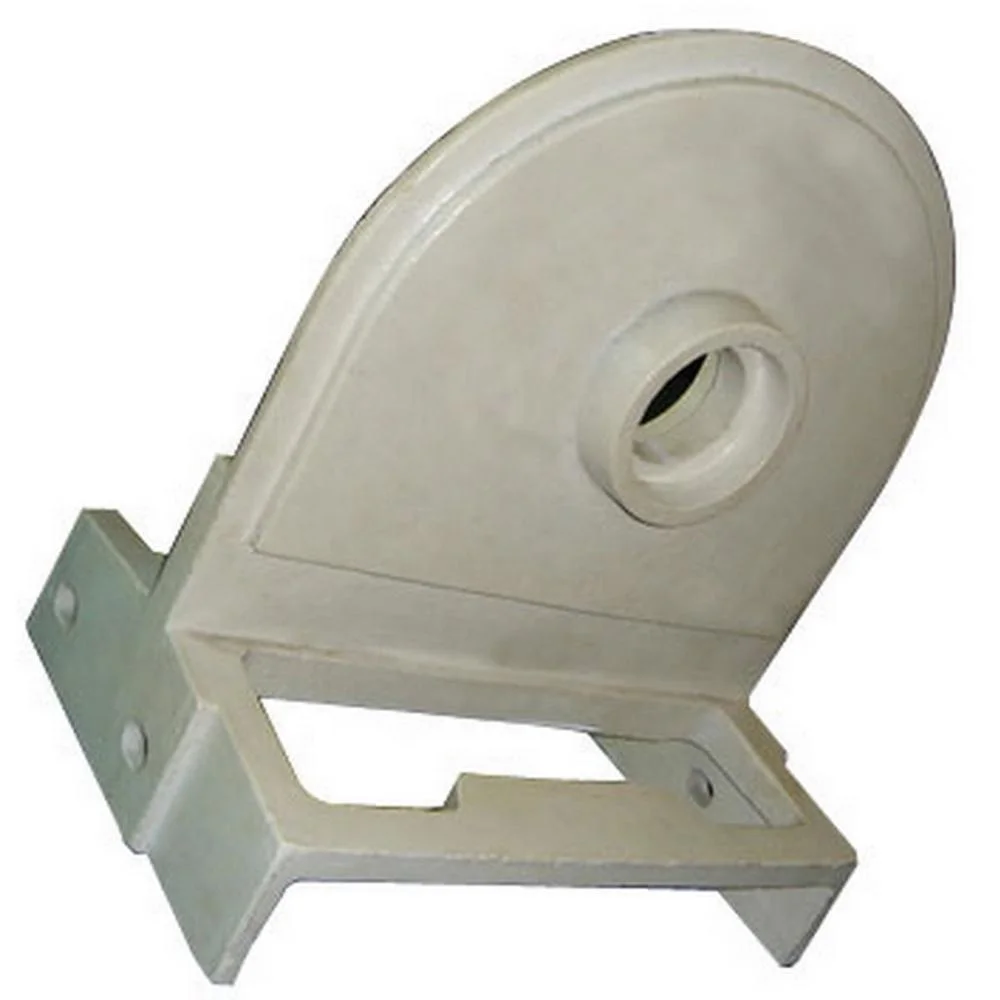
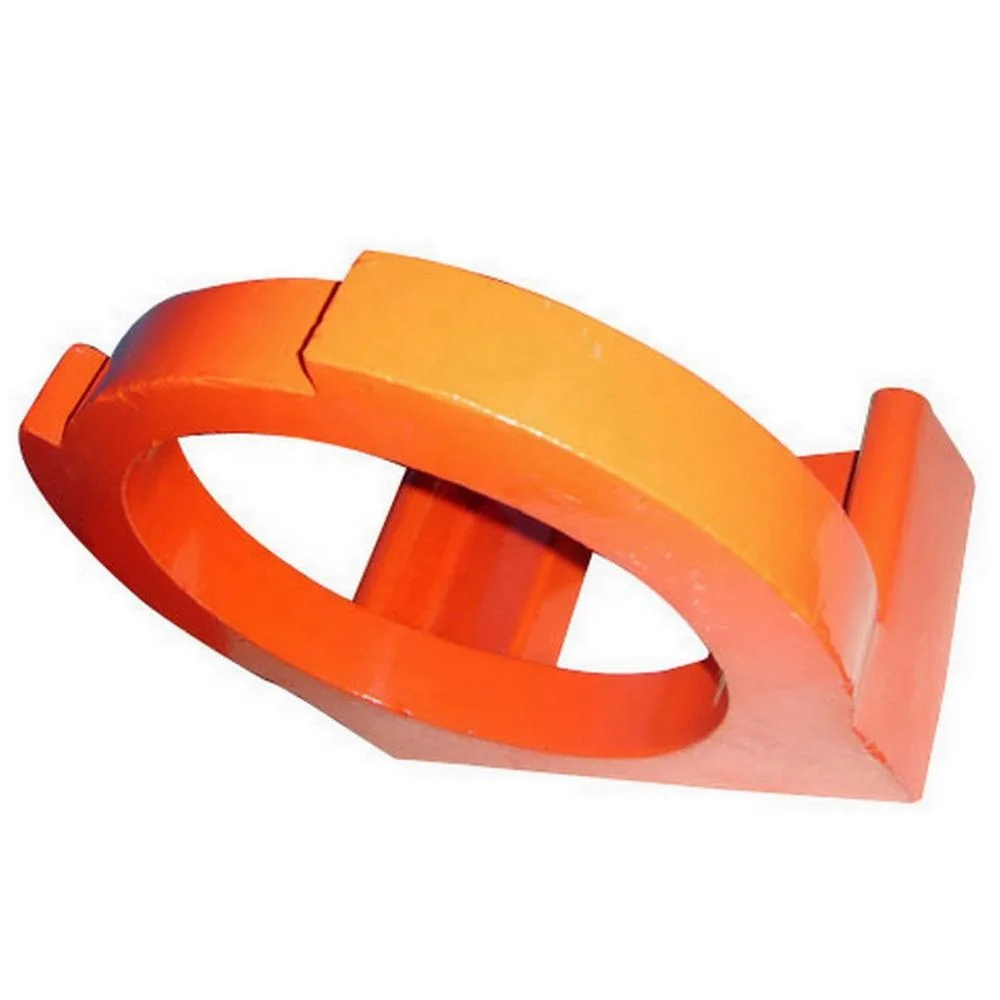
OEM Steel Precision Lost Wax Investment CNC Castings, Quench/Temper, Shot-Blast Assembly and 100% Visual/Gage Inspection
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishShot Blasted
-
MaterialSteel
-
NameOEM Precision Investment Casting PartsKeywordsprecision casting parts
-
ProcessLost wax investment casting+CNC machinedHeat TreatmentQuench and temper by 2 set mesh belt furnaces
-
Surface TreatmentShot blasting+AssemblingMachining Facility50+ Machining centers,80+ CNC machines
-
InspectionMT/UT/RT/100% visual+100%gage/CMMStandardASTM. AISI. DIN. BS. JIS. NF. AS.
-
CertificationIATF16949/ISO14001
OEM precision steel castings bring together lost wax investment casting, CNC machining, quench and temper, shot blasting and assembly. The inspection direction includes 100% visual and 100% gage inspection, with MT, UT, RT and CMM selected to the actual job. Define the component, supplied steel and finished requirements for that combined work scope.
Quench/temper requirements for the OEM steel part
Quench and temper is supported by a two-mesh-belt-furnace direction. Establish the required heat-treated condition for the chosen steel and drawing. Identify the material and dimensional evidence used to accept the resulting part for its actual working duty.
Machining references and assembly interfaces
The separate facility references are 50+ machining centers and 80+ CNC machines, with actual job/facility allocation to confirm. Define cast and CNC-machined limits, shot-blasted areas and the mating arrangement of any assembly. Agree the final condition and interface acceptance for the component being supplied.
Visual/gage coverage and additional tests
Allocate the full visual and gage checks to actual inspected characteristics and accepted records. Specify the relevant MT, UT, RT or CMM methods and coverage separately for the selected job. Connect that inspection plan to the drawing, heat condition and completed assembly or surface requirements.
Seven engineering families for the selected job
ASTM, AISI, DIN, BS, JIS, NF and AS provide engineering reference families whose applicable documents, editions and grades need selection. IATF16949 and ISO14001 are management-system references; establish actual organization/site and current document scope where required. Confirm quantity and OEM manufacturing/assembly responsibility with the agreed component requirements.








