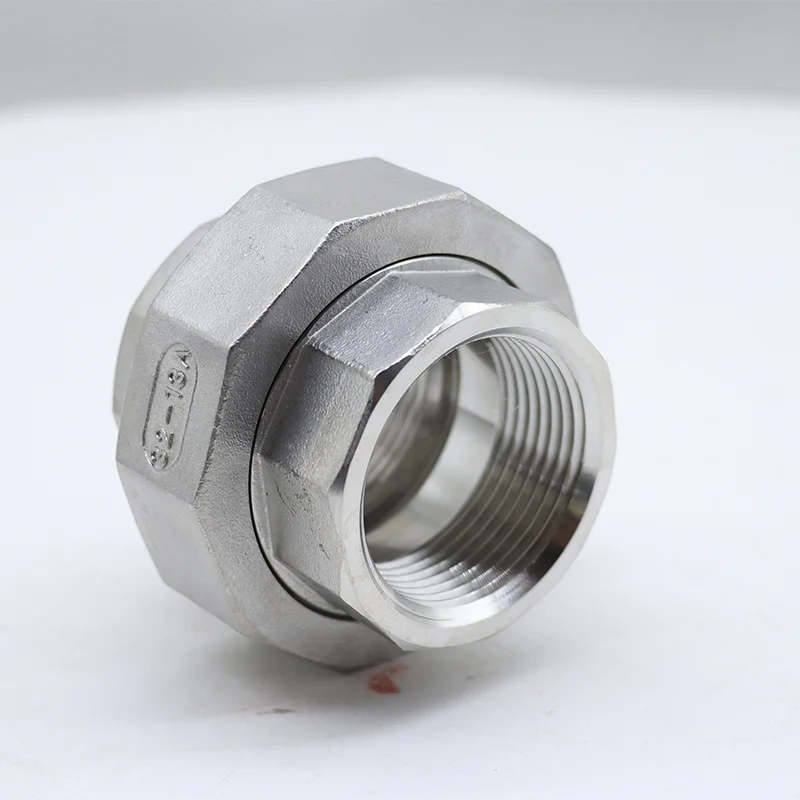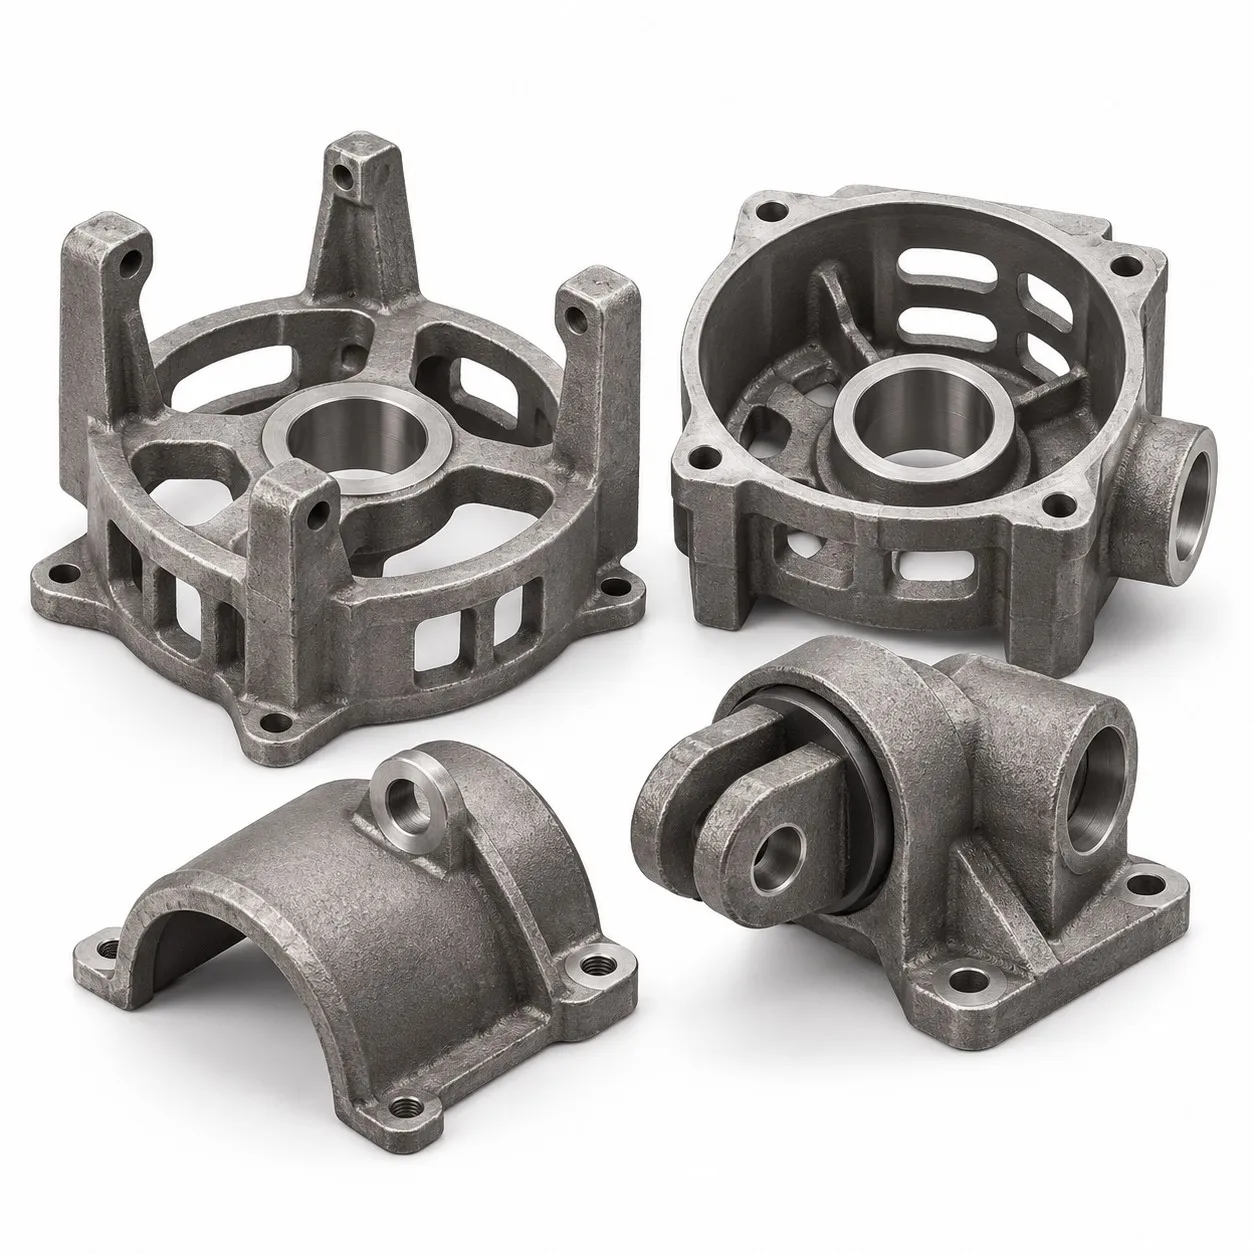
OEM SS304 SS316 Stainless Steel Lost Wax Investment Casting with Polishing and In-House Tooling
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishPowder Coated , Shot Blasted
-
Casting MethodDie Casting
-
MaterialStainless Steel, Ductile Iron, Aluminum, Spectrometer AnalysisSurface TreatmentShot Blasting, Powder Coating, Hot Dip Galvanized, E-coating, Painting
-
Tolerance & Surface RoughnessCT4-CT6 (Investment), CT10-CT12 (Sand), Ra 1.6-3.2 (Smooth Finish)Tooling & Mold DesignIn-house Tooling Design, Mold Manufacturing, Prototyping Service
-
Service TypeOEM/ODM Custom Manufacturing / PrototypingDrawing FormatsSTEP, STP, IGES, DXF, DWG, PDF
-
CertificationISO 9001, IATF 16949 , AS 9100 , CE, RoHSQuality Control100% Inspection, CMM, Projector, Caliper, Salt Spray Test
-
Lead Time7-10 Days (Prototype), 15-25 Days (Mass Production)
SS304 and SS316 stainless steel lost wax investment casting supports OEM/ODM custom parts and prototype enquiries. In-house tooling design, mold manufacturing and prototyping connect component development with the casting route. Polishing and several additional surface treatments let the finished condition be considered alongside the material and geometry.
Keep casting classes tied to their routes
Investment-casting tolerance references are CT4-CT6, while the separate sand-casting reference is CT10-CT12. Apply the appropriate class to the selected manufacturing route and drawing dimensions. Ductile iron and aluminum are additional material choices, and die casting is another process enquiry whose compatibility should be established for the actual grade. The surface roughness reference is Ra1.6-3.2; agree its measurement unit and the surfaces it governs.
Develop the mold and finished surface
Tooling and prototype discussions can use STEP, STP, IGES, DXF, DWG or PDF files. A drawing revision, exact grade and controlled geometry give the in-house mold work a defined target. Surface choices include polishing, shot blasting, powder coating, hot-dip galvanizing, E-coating and painting. Select a treatment suitable for the chosen metal and identify which faces need that condition on the finished part.
Build a component-specific inspection plan
The quality provision includes 100% inspection, with spectrometer analysis for material review and CMM, projector, caliper and salt-spray methods available for an agreed plan. Distinguish overall inspection coverage from the particular measurements or tests required on each component. ISO9001, IATF16949, AS9100, CE and RoHS references can be reviewed for the relevant current document, object and scope. These details help align prototype evaluation and subsequent manufacturing acceptance without assuming that every method applies to every part.