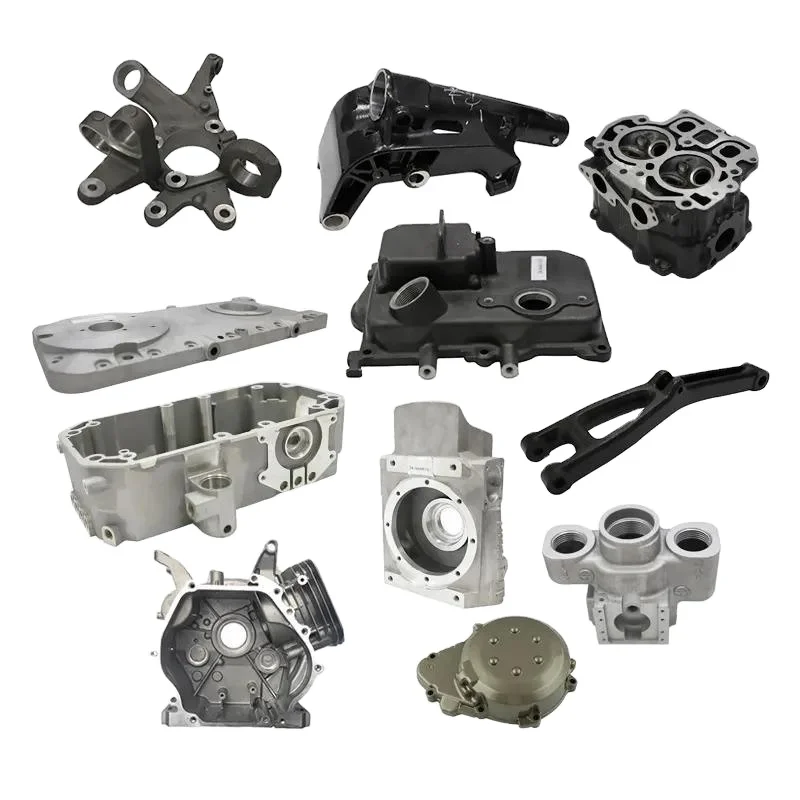
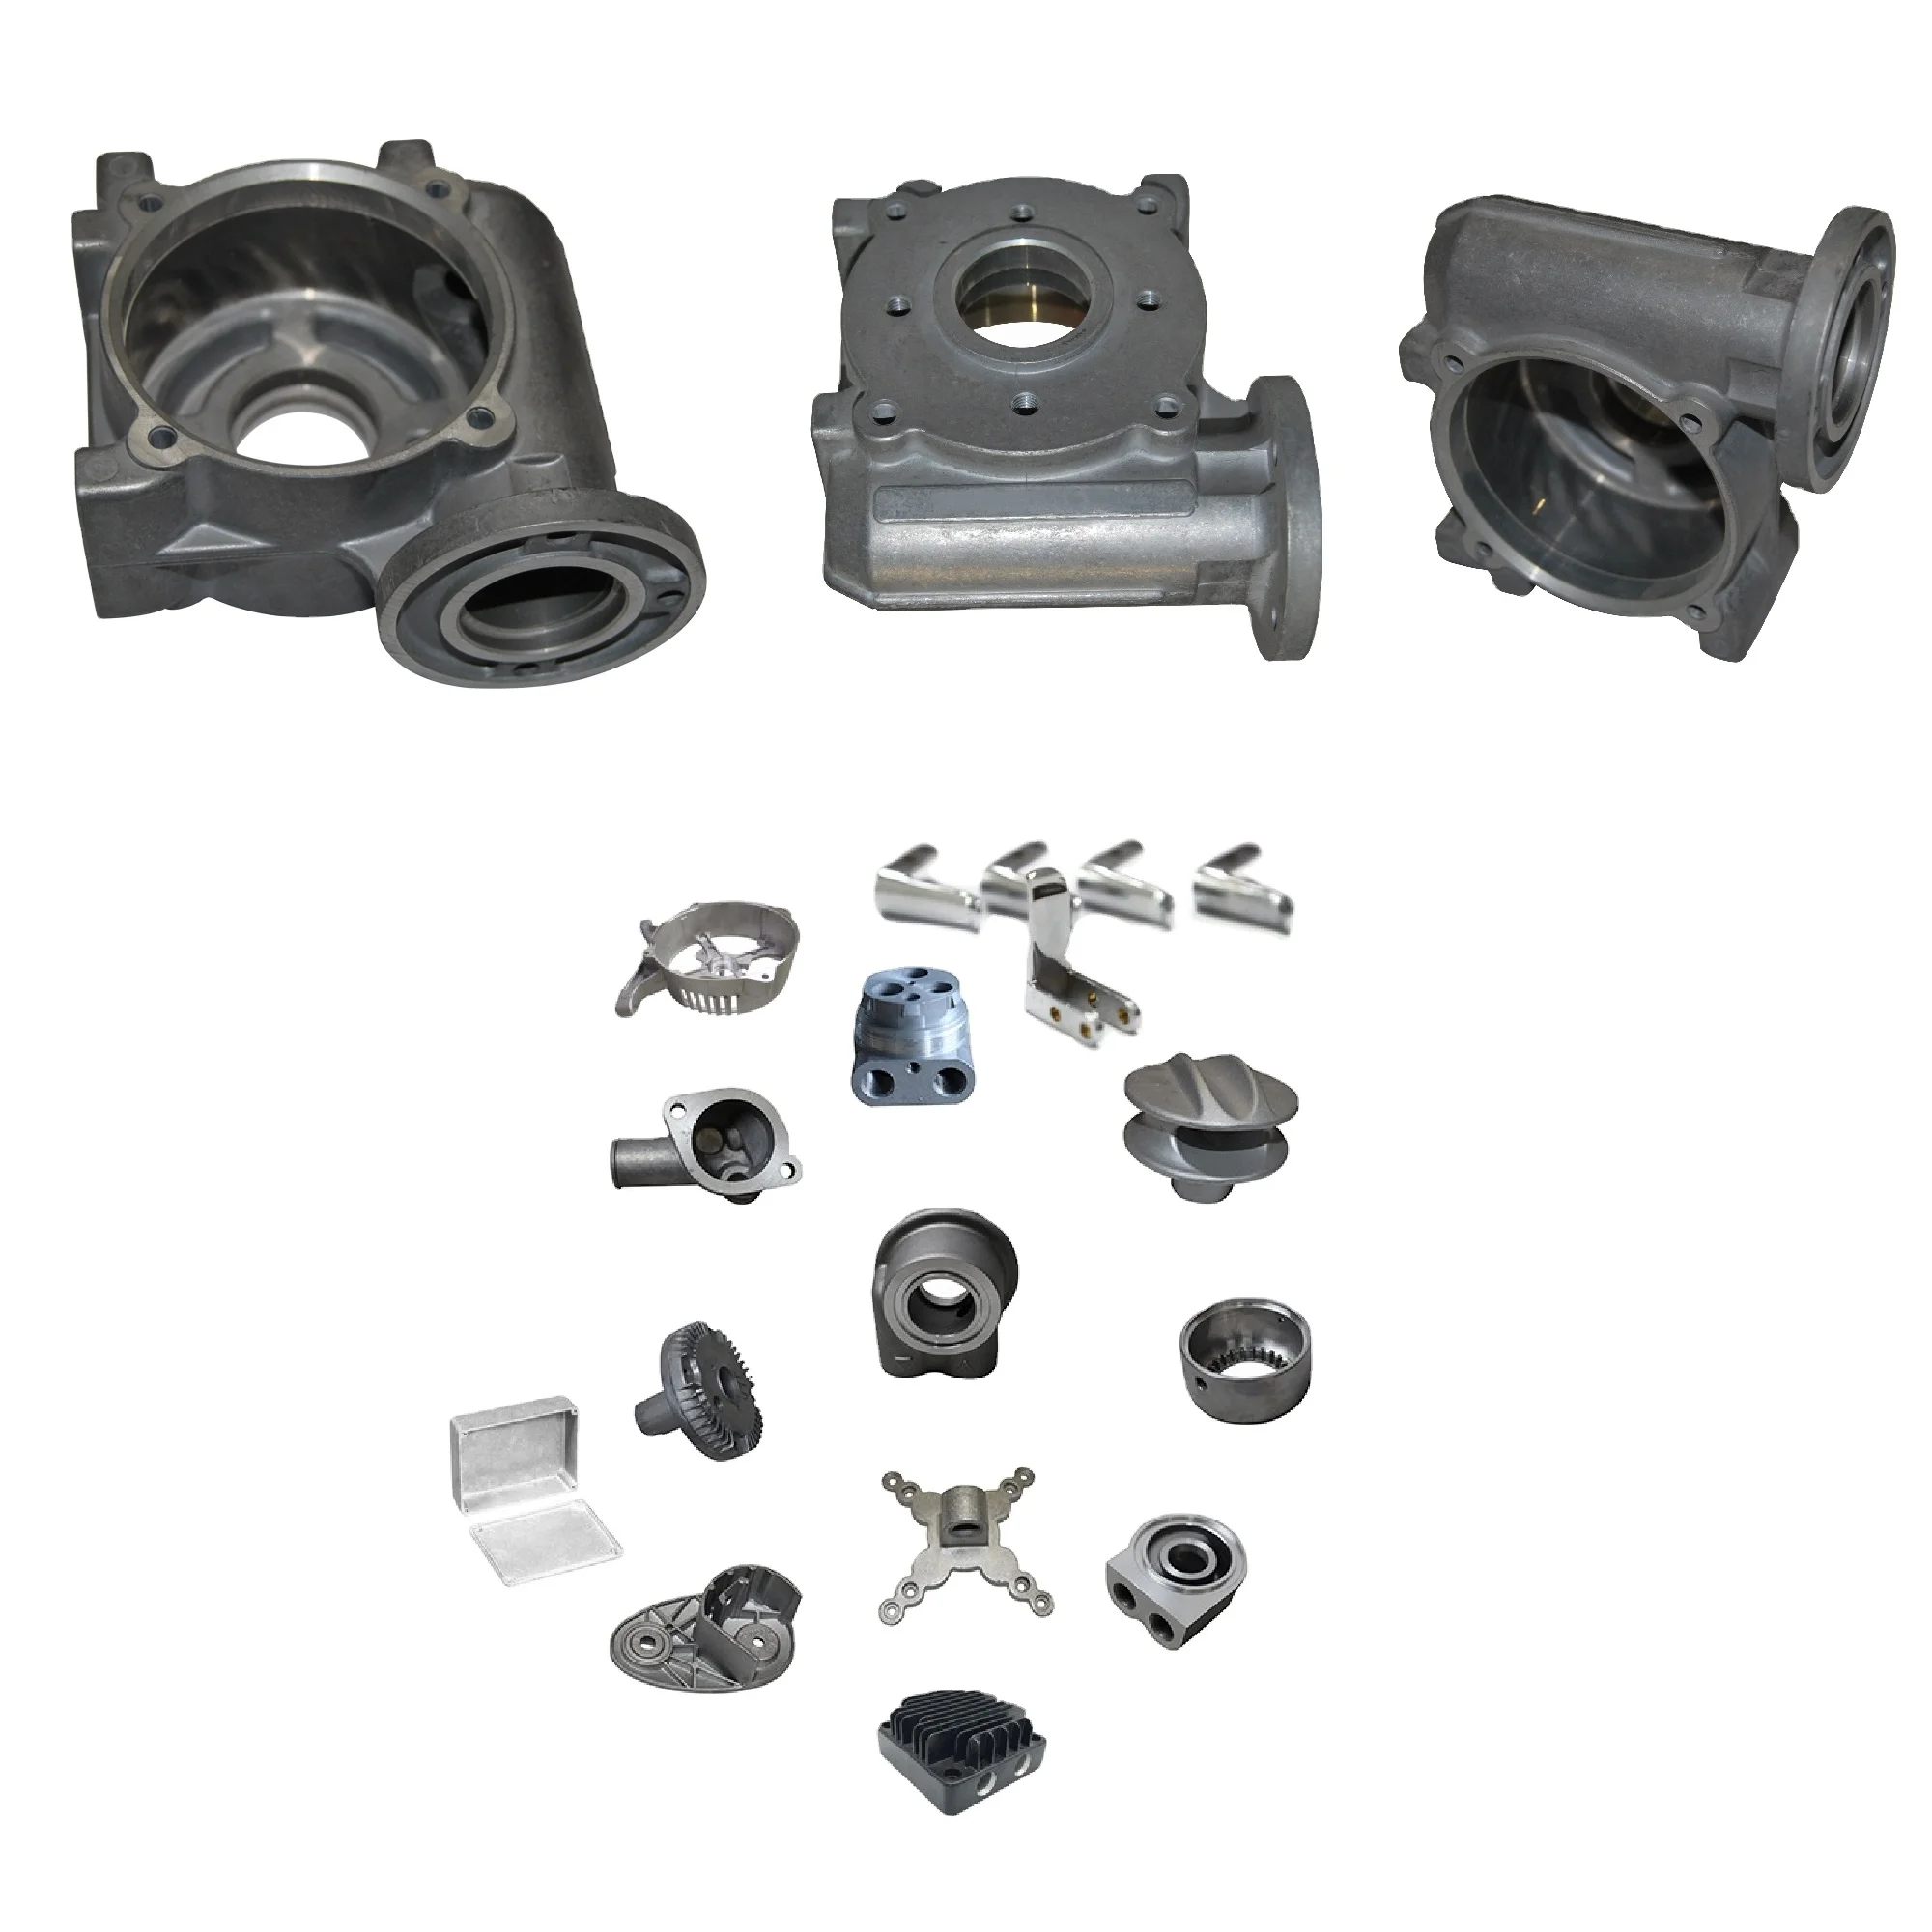
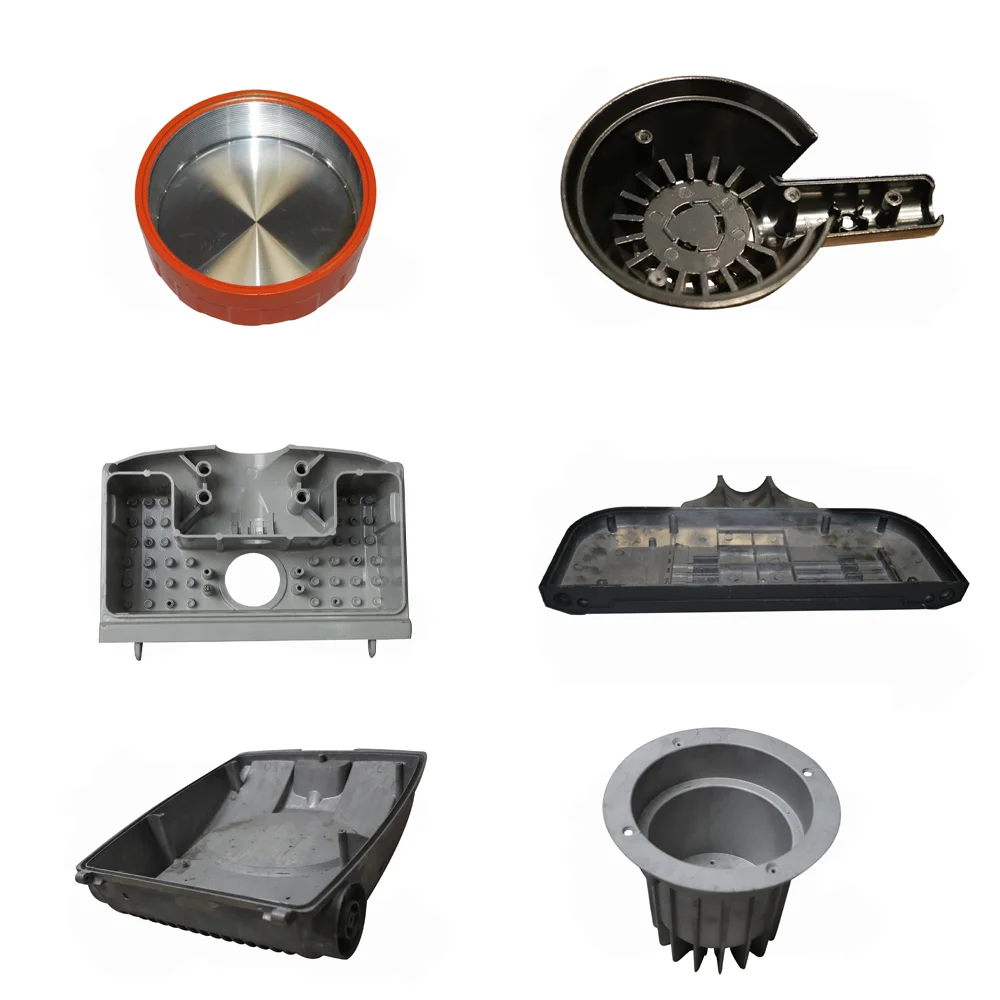
OEM ADC12/A380 Aluminum-Alloy Die Cast Parts, CT4–6, Optional CNC Machining/Finishing and Up-to-IT7 Requests
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishPassivated , PolishedAlloy GradeA380 , ADC12
-
ItemMetal Die Casting Fabrication Aluminum Alloy Die Casting
-
MaterialAluminum Alloy ADC12, A380 etc. As customer request.Manufacturing ProcessDie casting+(Machining+Surface treatment if need)
-
Casting ToleranceCT4-6 for aluminum die casting partsMachining ProcessCNC Machining/ Lathing/ Milling/ Turning/ Boring/ Drilling etc.
-
Machining TolearnceUp to IT7, Ra 0.8~3.2 , according to customer requirementSurface TreatmentSurface Passivatin, Polish. As customer request
-
Package of Die Casting PartsMultilayer wooden box/pallet, with big plastic bag insideLead Time40-50 days for Die Cast Aluminum
-
ServiceCustom Die Cast Aluminum as per drawings or samples
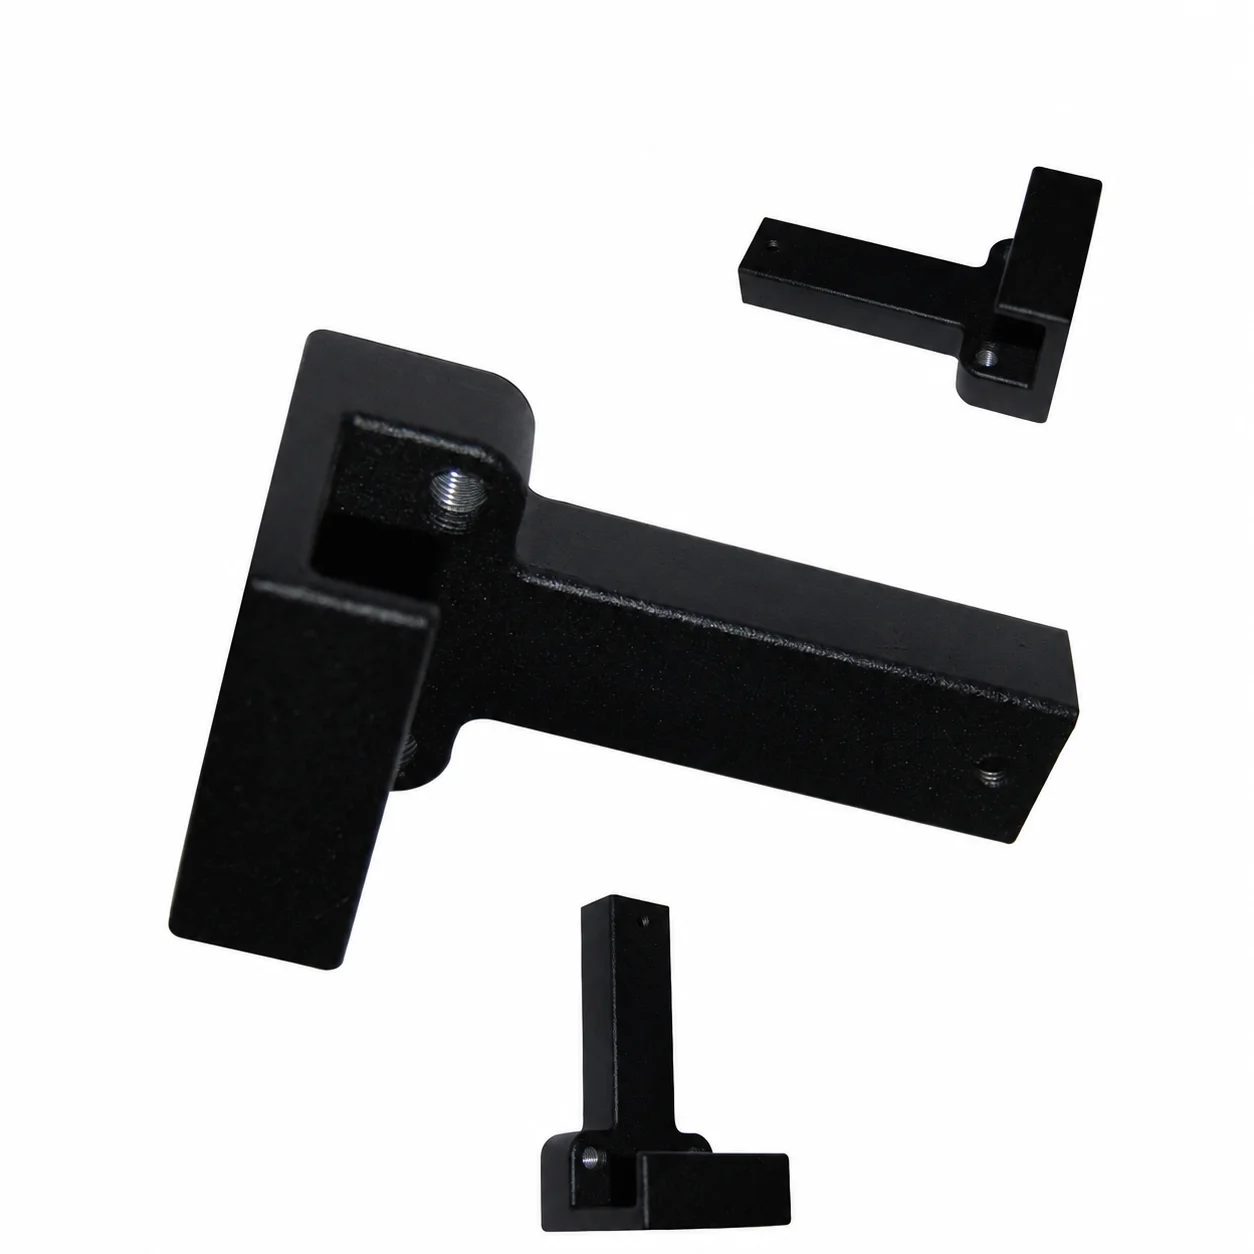
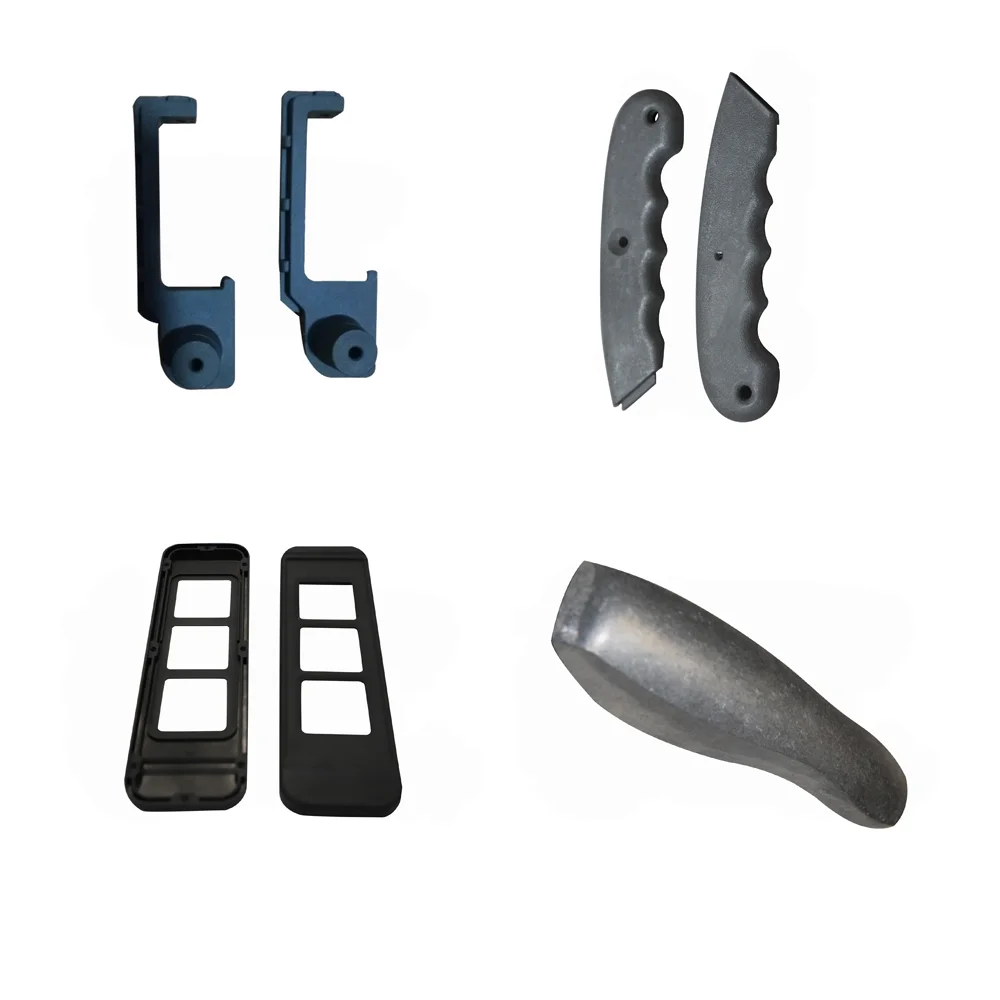
OEM custom aluminum-alloy die-cast parts include ADC12 and A380 material directions and customization from drawings or samples. The aluminum casting-tolerance reference is CT4–6. Machining and surface treatment are selected if needed, with actual dimensional limits, finished condition and working acceptance agreed for the component.
ADC12 or A380 drawing and cast geometry
Choose the actual aluminum-alloy specification and provide the part drawing or agreed sample. Define the geometry, interfaces and working duty that the component must satisfy. Assign the CT4–6 casting direction to the relevant aluminum die-cast features and set their acceptance criteria. Agree how the actual sample or finished casting will be compared with those requirements.
Optional operations and machined acceptance
The secondary-work directions cover CNC machining, lathing, milling, turning, boring and drilling. Identify which are needed and the locations they control on the drawing. Machining is referenced up to IT7 according to customer requirement, with actual feature limits and measurement basis to agree. For Ra 0.8–3.2, confirm the unit and applicable surfaces before defining roughness acceptance.
Passivation, polishing and custom responsibility
Passivation and polishing are surface directions to customer request. Select the applicable treatment areas and final condition with the actual material and cast or machined dimensions. Establish inspected characteristics, methods and records for that finished component. Confirm quantity and OEM manufacturing responsibility with drawing/sample comparison, selected operations and any working-duty evidence the project requires.