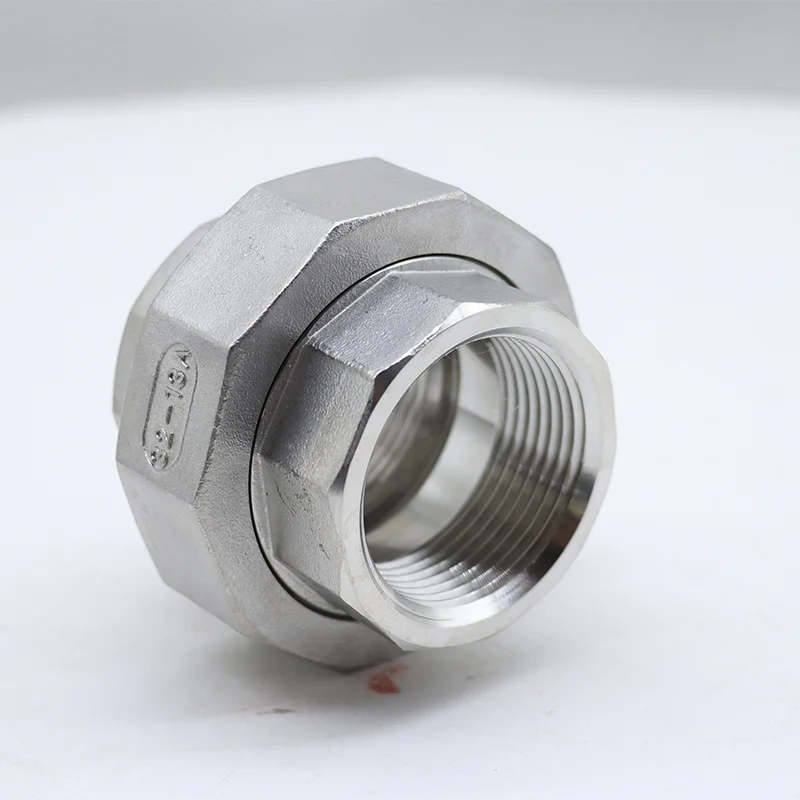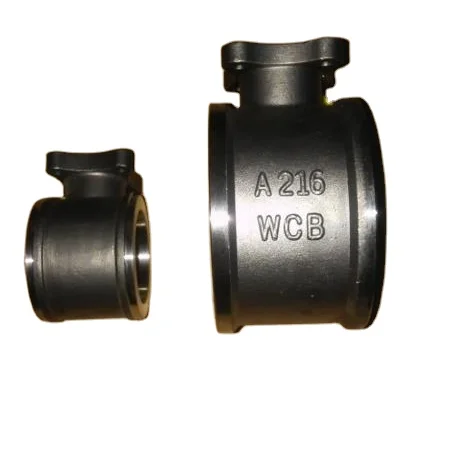
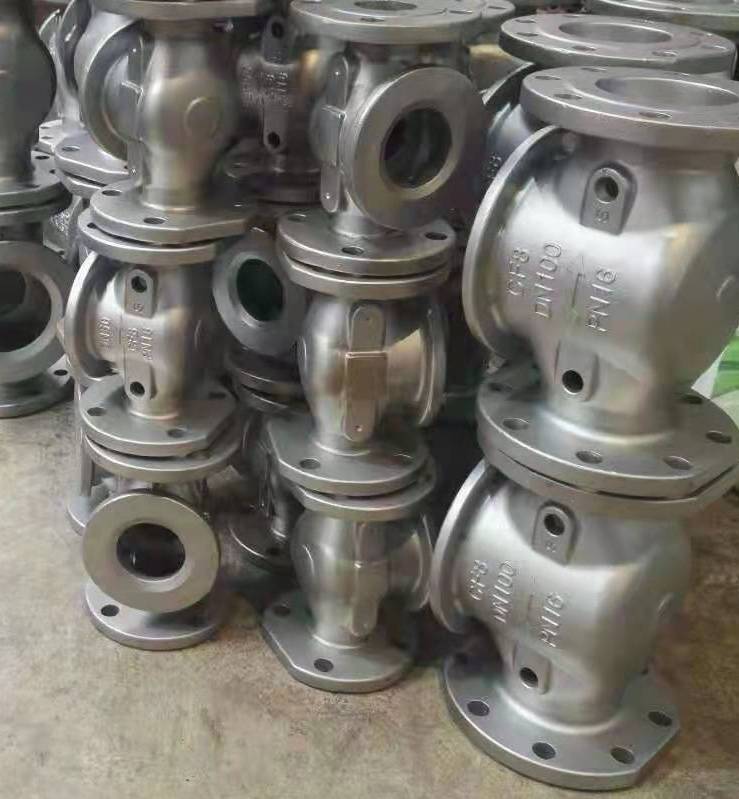
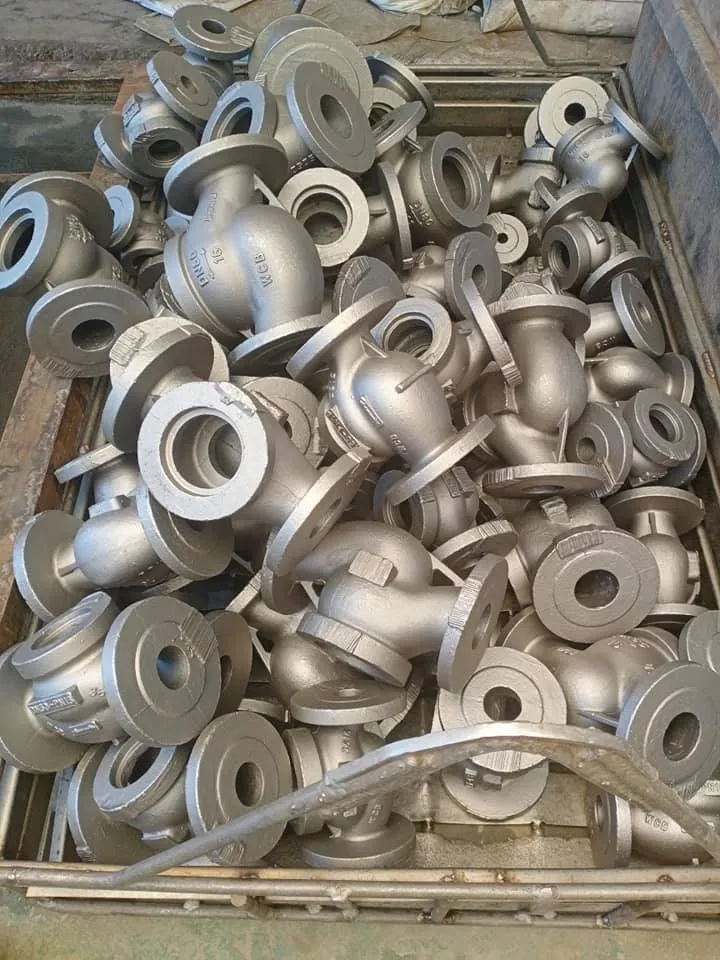
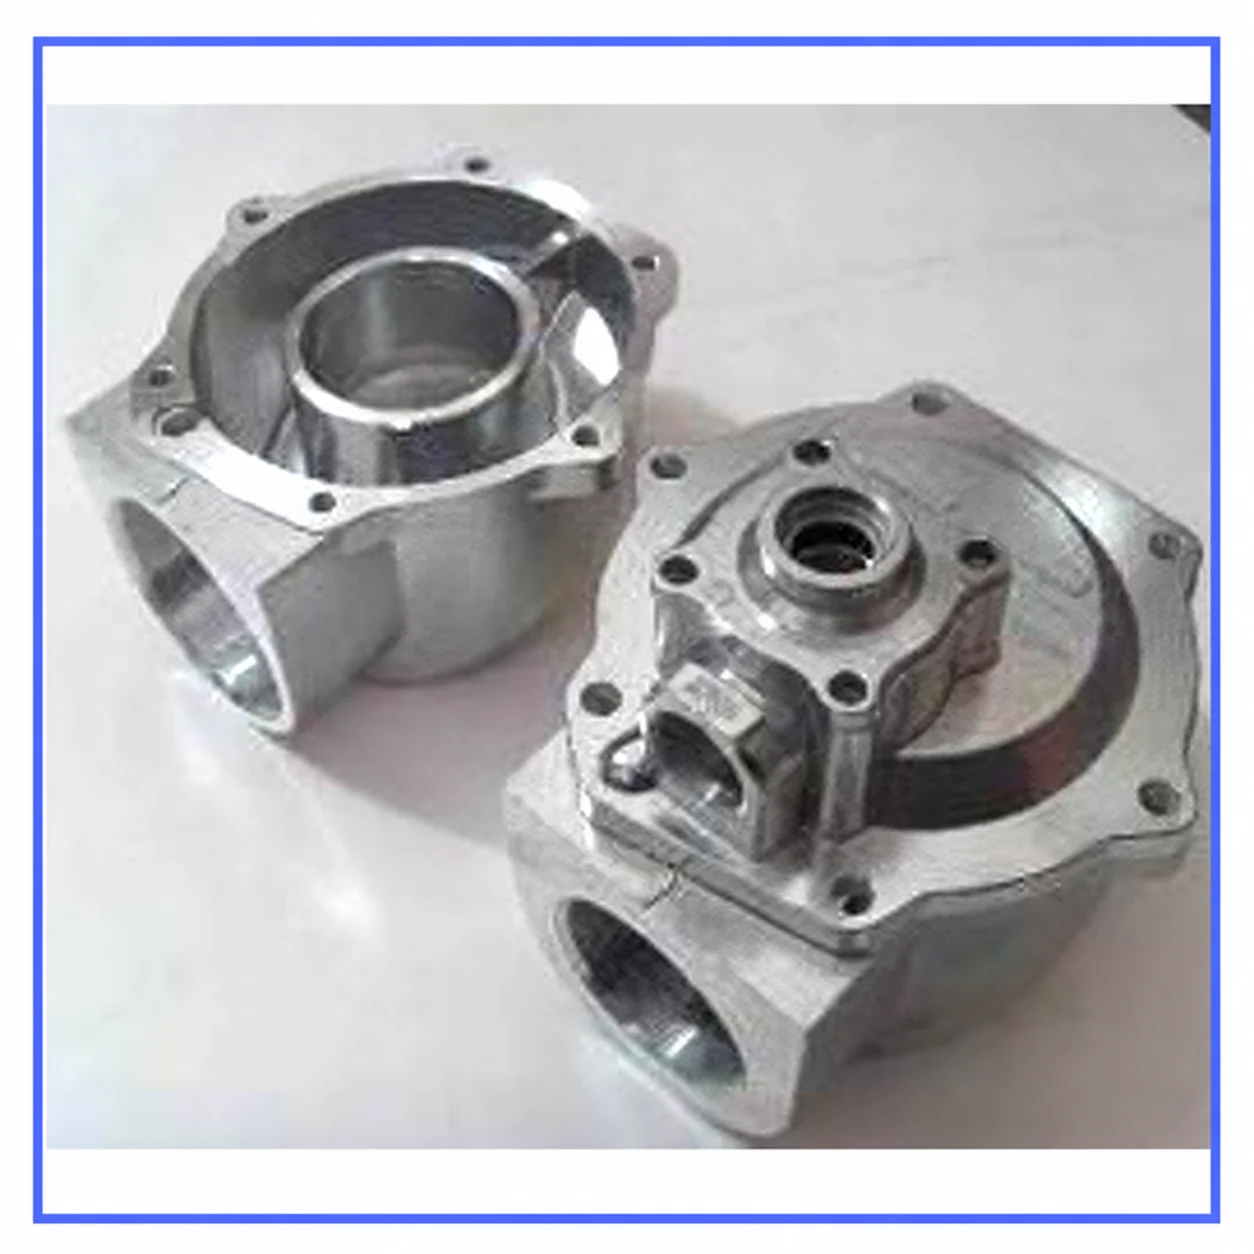
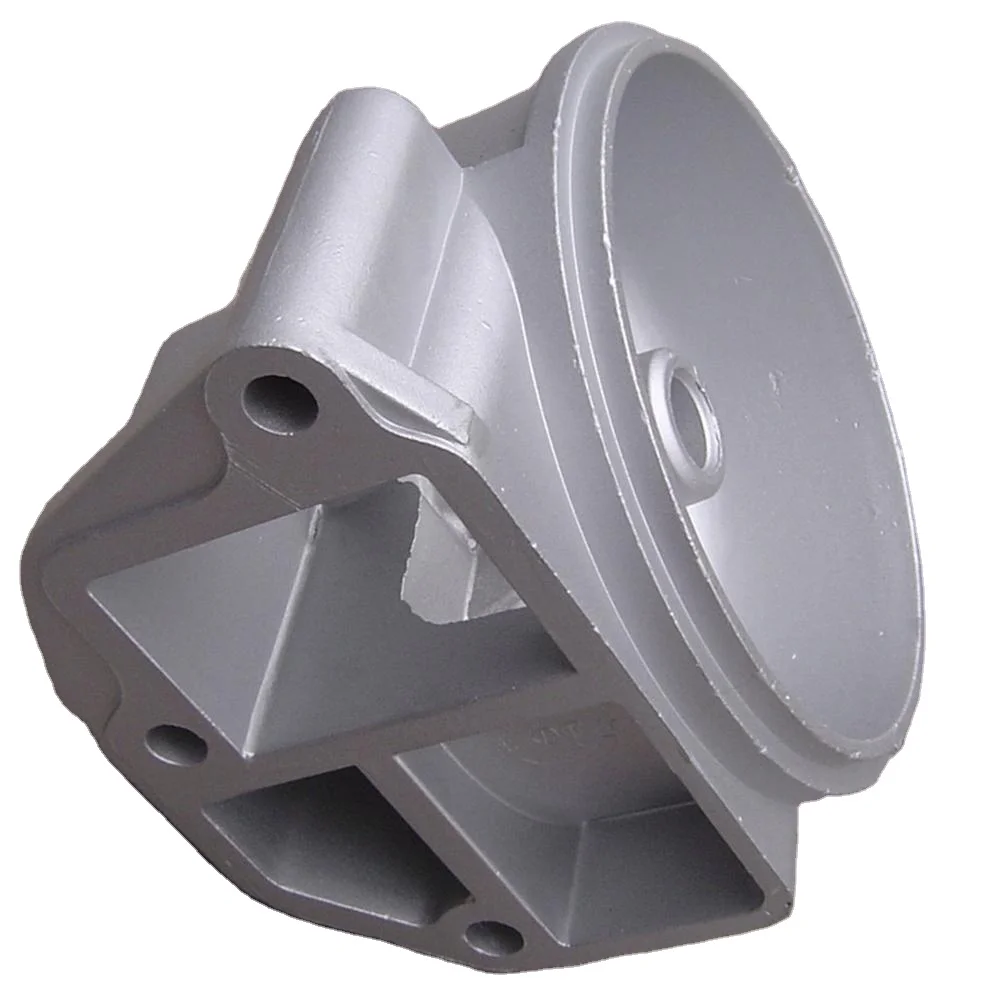
Custom OEM ODM A216/WC6/WC9 Steel Valve-Body Lost Wax Investment CNC Casting Requests, ±0.01–0.05mm and Galvanized
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishPlated
-
Applicationcustom Machinery Parts
-
Dimensionssilicon sol lost wax investment castingNameCustomized Machined CNC Machining
-
MaterialMild steel, carbon steel,steel alloyProcesscasting,Cnc Machining,deburrs, finish
-
ServiceOEM ODMMachiningtap, punching,milling
-
Tolerence±0.01-0.05MMFinishgalvanized zinc plating
OEM/ODM steel valve-body and machinery-part requests combine silicon-sol lost wax investment casting with CNC machining, deburring and finishing. A216, WC6 and WC9 are material/specification references whose exact role and relationship need agreement. The tolerance reference is ±0.01–0.05mm, with galvanized and zinc-plating finish directions.
Steel references and valve-body duty
Material directions also include mild steel, carbon steel and steel alloy. Specify the actual supplied steel and component drawing, and clarify how A216, WC6 and WC9 apply to that request. Define the valve-body or machinery working duty together with its geometry and dimensions before agreeing the manufacturing scope.
Tapping, punching, milling and tolerance
Tapping, punching and milling are machining directions alongside CNC work. Assign the required operations to the actual component locations and confirm the interpretation of the ±0.01–0.05mm reference. Agree its feature and process allocation, measurement conditions and acceptance records for the selected dimensions.
Galvanized or zinc-plated condition
Define the actual galvanized or zinc-plating treatment method and the areas it covers. Specify the final condition and how the surface will be assessed with the dimensional requirements. Deburring and finishing belong within the agreed work scope for the component concerned.
OEM/ODM acceptance for the component
Confirm project quantity and the allocation of design and manufacturing responsibility for the valve-body or machinery request. Agree the inspection criteria and documents needed to evaluate the finished part. Any particular valve pressure, temperature or service-approval requirement needs a separate acceptance basis for that actual component.