
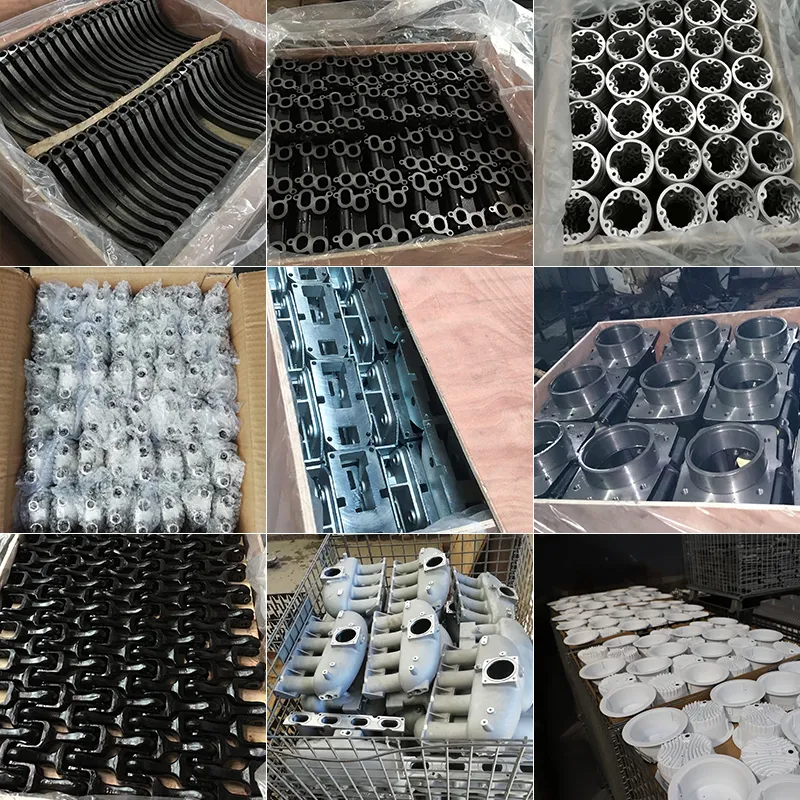
Custom Industrial Ductile/Grey-Iron Sand Castings | CT9–CT11, CNC and Durability Requirements
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
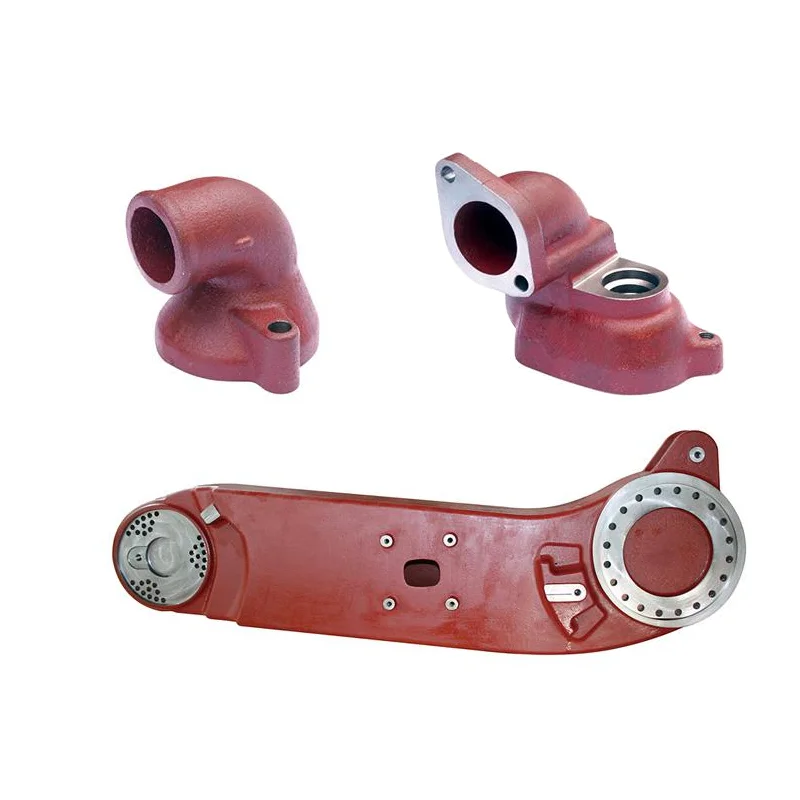
Surface FinishPainted
-
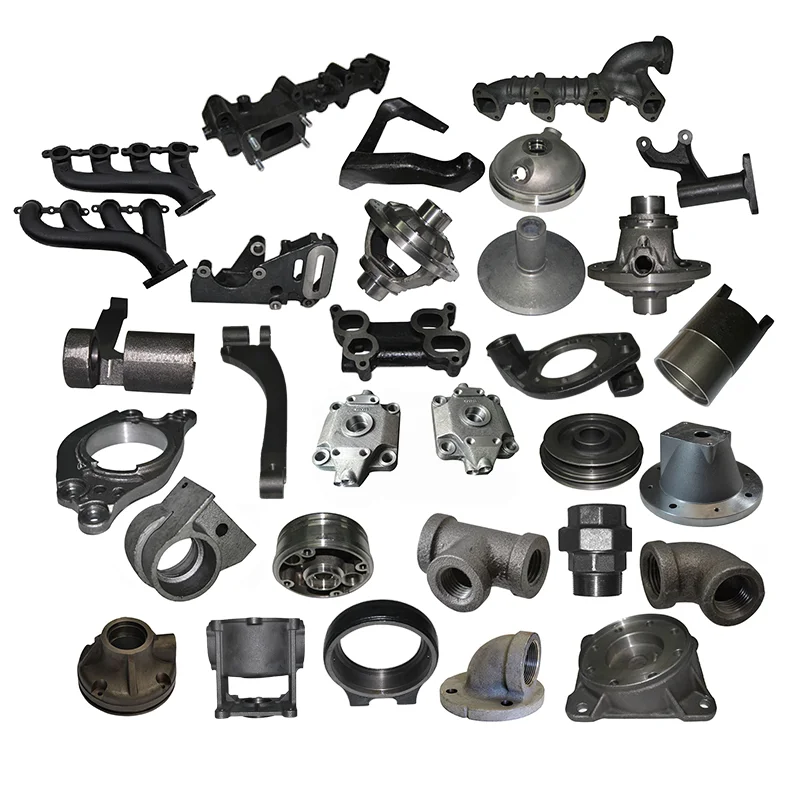
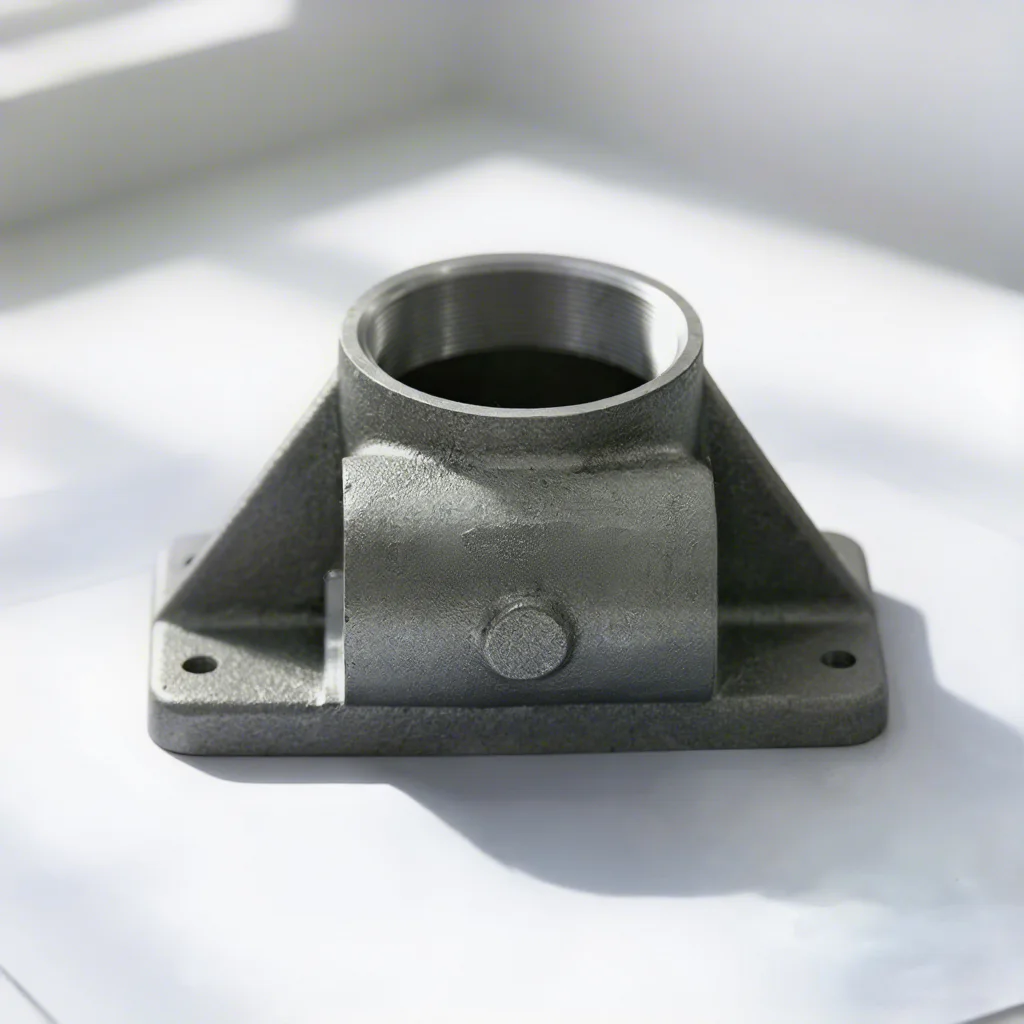
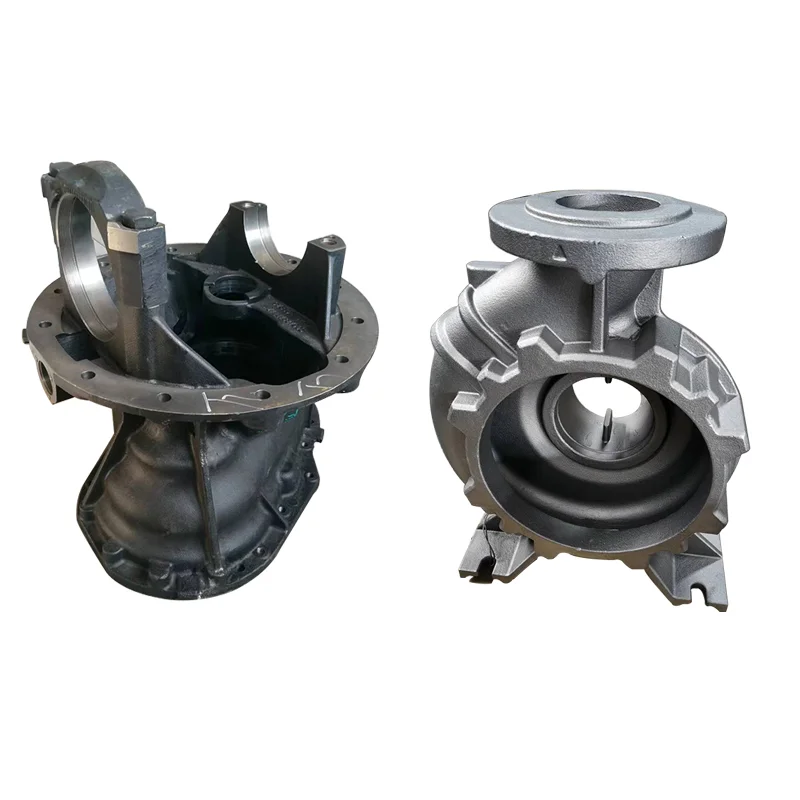
Product NameCast Iron Casting Manufacturer Industrial Durable Metal Part Castings
-
MaterialDuctile iron or grey iron etc. As customers requestBlank ProcessSand casting, cast iron
-
Casting ToleranceCT9-11 for Sand CastMachining ProcessCNC Machining/ Lathing/ Milling/ Turning/ Boring/ Drilling etc.
-
Machining ToleranceUp to IT7, Ra 0.8~3.2 , according to customer requirementSurface TreatmentDacromet Coating, Finish Painting etc. As customers request
-
Package for iron casting partMultilayer wooden box with big plastic bag insideLead Time50 days for iron casting part
-
Our ServiceCustom make iron casting part as per drawings or samples
Custom industrial cast-iron parts are directed to ductile iron or grey iron and sand casting, sized to customer drawings or samples. The sand-casting tolerance is CT9–CT11. Machining capability is up to IT7, with an Ra0.8–3.2 reference whose unit and measurement basis should be agreed for the actual surface.
Ductile or grey iron for the industrial part
Select the actual iron designation and the geometry needed for the component. Connect the drawing or sample dimensions to its intended function and operating duty. Durability is a qualitative requirement to define around that material and use, with acceptance reflecting the actual finished part and its important interfaces.
Sand-cast dimensions and the machining scope
Define the dimensions governed by the CT9–CT11 sand-casting reference and the areas requiring finished machining. Operation directions include CNC machining, lathing, milling, turning, boring and drilling. Select the actual operations for the chosen geometry, relating the cast and machined areas to the required component fit.
Up to IT7 and the Ra reference
Agree where the machining capability applies and identify its controlled dimensions and measurement acceptance. Assign the Ra0.8–3.2 reference to the actual surfaces with its unit and inspection basis. Connect those requirements to the selected iron, operation sequence and finished interfaces so the dimensional and surface expectations remain clearly defined.
Dacromet coating or finish painting
Dacromet coating and finish painting are surface-treatment directions following customer requirements. Select the requested work and the areas receiving it on the industrial casting. Agree the appearance, dimensional and inspection criteria for the chosen finish, linking the actual geometry and material to the finished condition needed for its use.








