ADC12/A380 Aluminum Die Cast Lighting Parts | High Pressure, Powder Coating & X-Ray
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishAnodized , Powder Coated
-
SizeOEM/ODM Supported (Size, Material, Surface Finish)Surface TreatmentMill Finish, Anodizing, Powder Coating, Electropla
-
MaterialsZinc, Aluminum, Magnesium, Stainless Steel, etc.Tolerance Standard±0.05mm, Custom Tolerance Available
-
Die Casting ProcessHigh-Pressure Die Casting, Precision Die CastingApplication FieldAutomotive, Electronics, Industrial Machinery, Medical Devices
-
Quality CertificationISO 9001, IATF 16949, RoHS CompliantLead Time7-15 Days for Samples, 20-30 Days for Mass Production
-
Drawing Format3D.STP. STEP . IGS . PRT . X_TPackageCustomers Specific Requirement
-
ProcessDie casting moldQuality Control100% Inspection, CMM, Projector, Caliper, Salt Spray Test
-
Service TypeOEM/ODM Custom Manufacturing / Prototyping
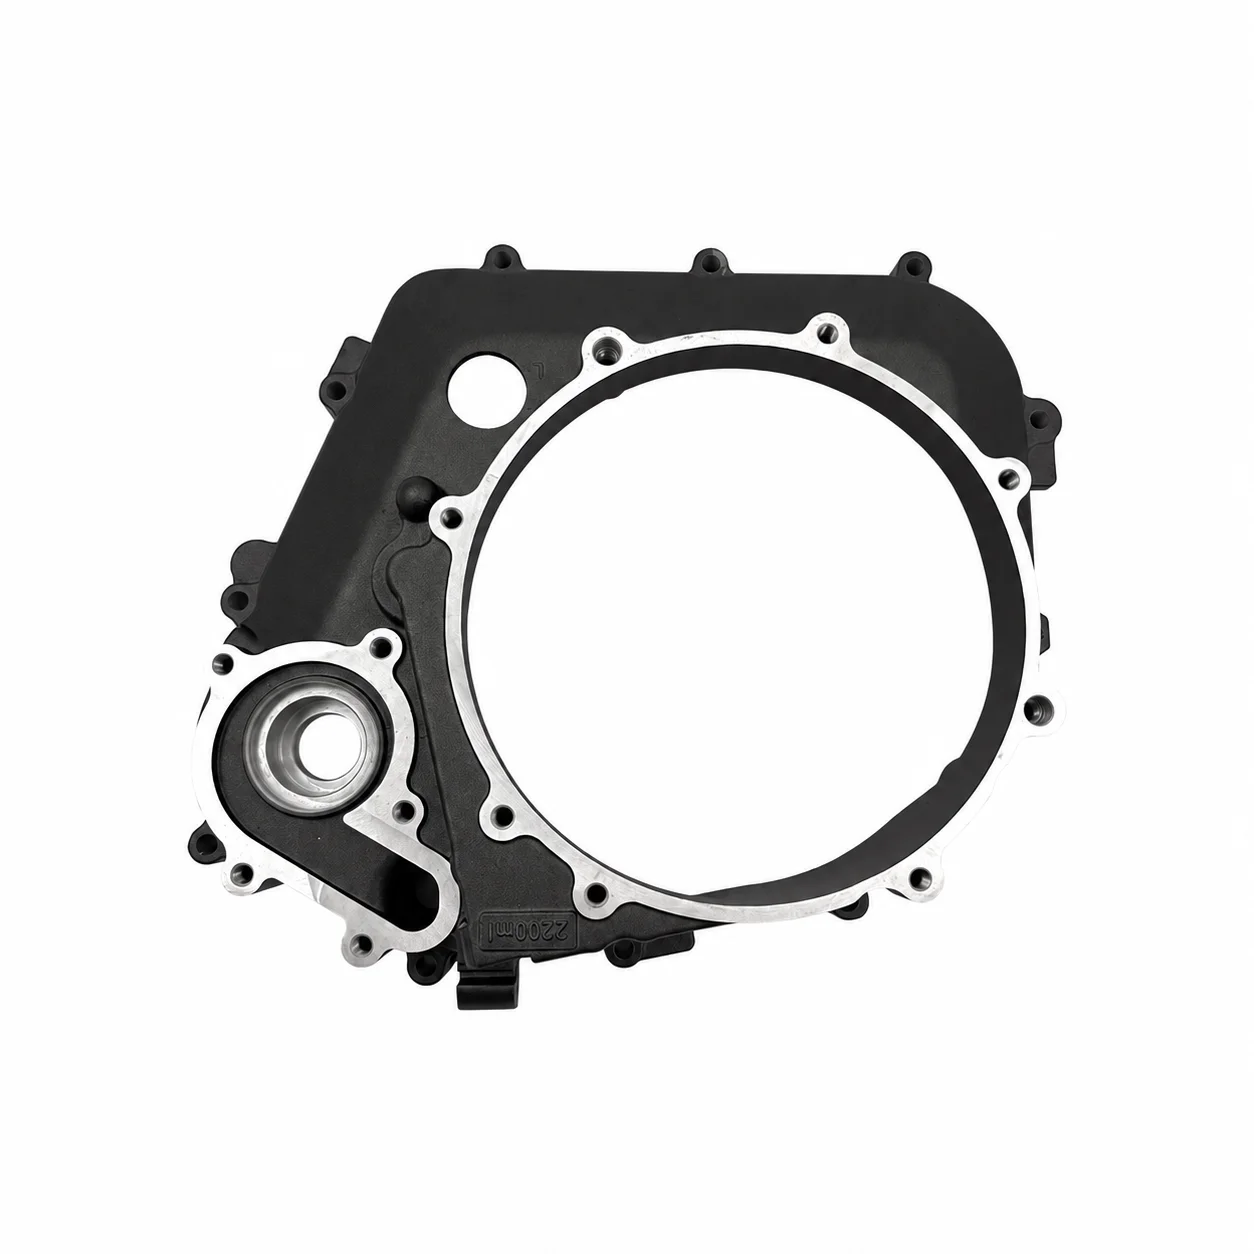
ADC12 or A380 aluminum lighting components are offered through high-pressure and precision die casting. OEM/ODM support covers size, material and surface finish, with a ±0.05 mm tolerance reference, custom tolerance availability, die-casting mold work, prototyping and samples.
Lighting geometry and selected die casting alloy
Choose ADC12 or A380 for the actual aluminum component and connect that grade to its 3D geometry and dimensional acceptance. Broader material enquiries also include zinc, magnesium and stainless steel, with the process pairing to be agreed separately. STP, STEP, IGS, PRT and X_T are supported 3D inputs for defining the particular part.
Mill finish, anodizing and coated surfaces
Finish directions include mill finish, anodizing, powder coating and electroplating. Identify the lighting surfaces that require a particular finished condition. Identify the treated surfaces and select the finish for the chosen material, relating it to the dimensions that need the ±0.05 mm or an agreed custom tolerance. This keeps the lighting component's appearance and dimensional requirement within one coherent manufacturing definition.
X-ray and other inspection requirements
The components receive 100% inspection, with X-ray, CMM, projector, caliper and salt-spray testing as methods to allocate in the acceptance plan. Other application directions include automotive, electronics, industrial machinery and medical-device components. Define the required test object and criteria for the actual application, and confirm relevant ISO45001, ISO9001, IATF16949 or RoHS documentation scope when the sourcing project requires it.