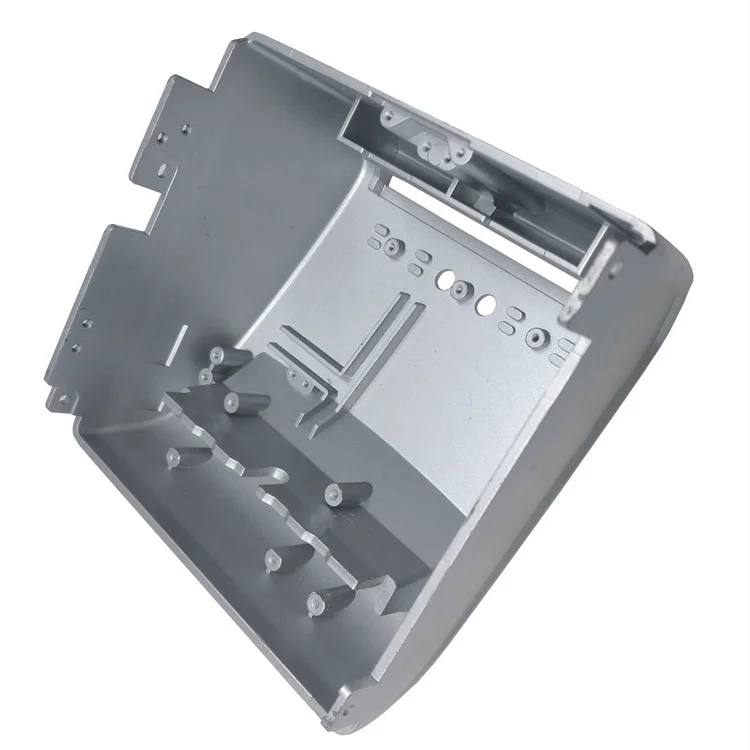
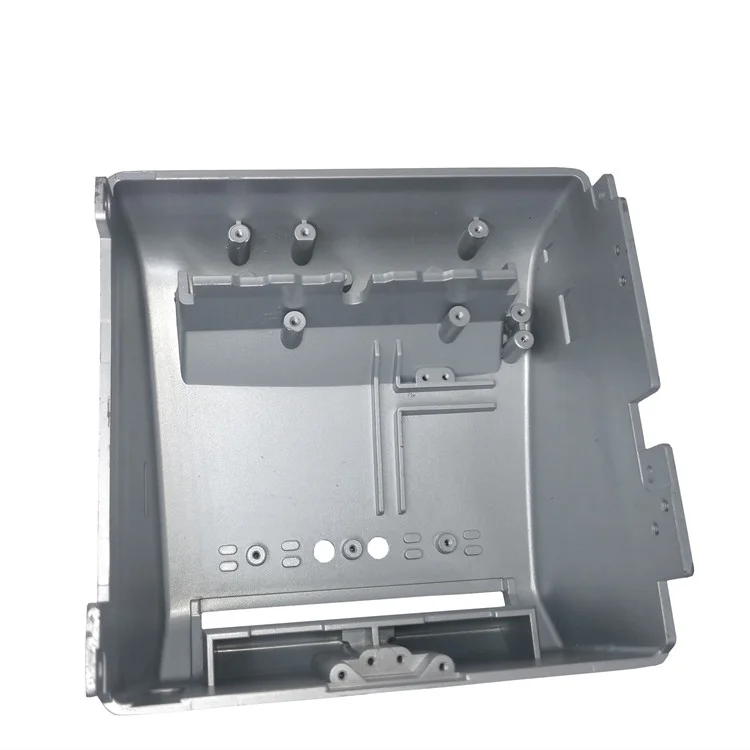
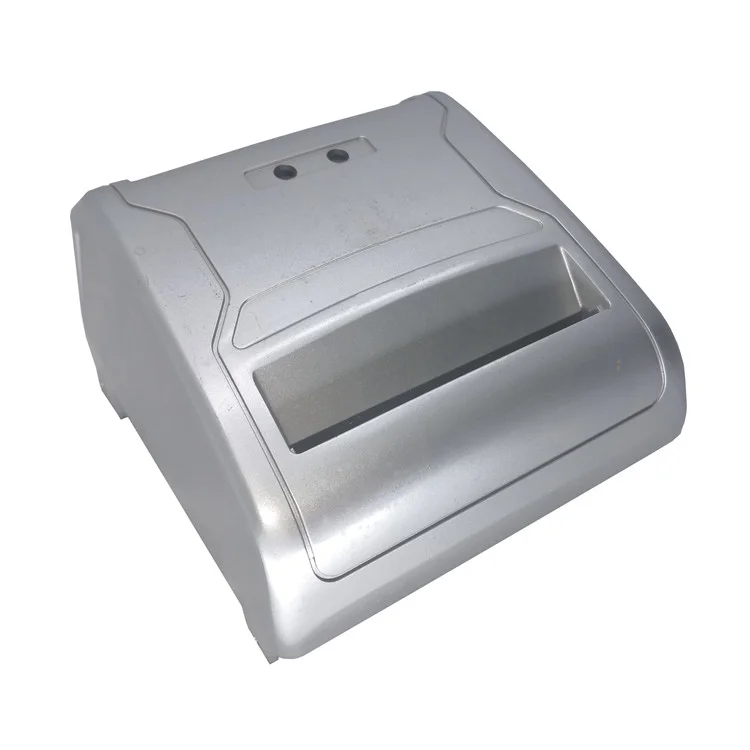
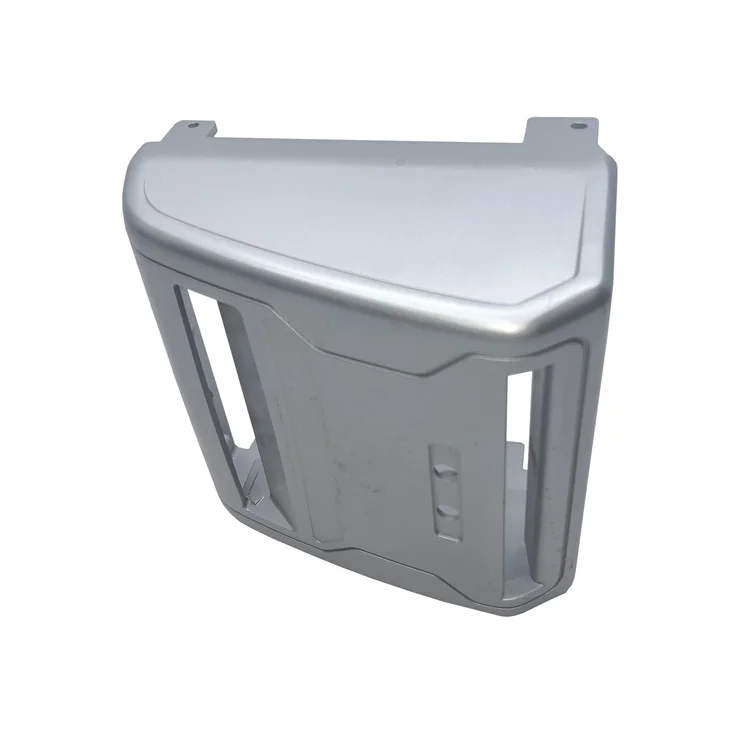
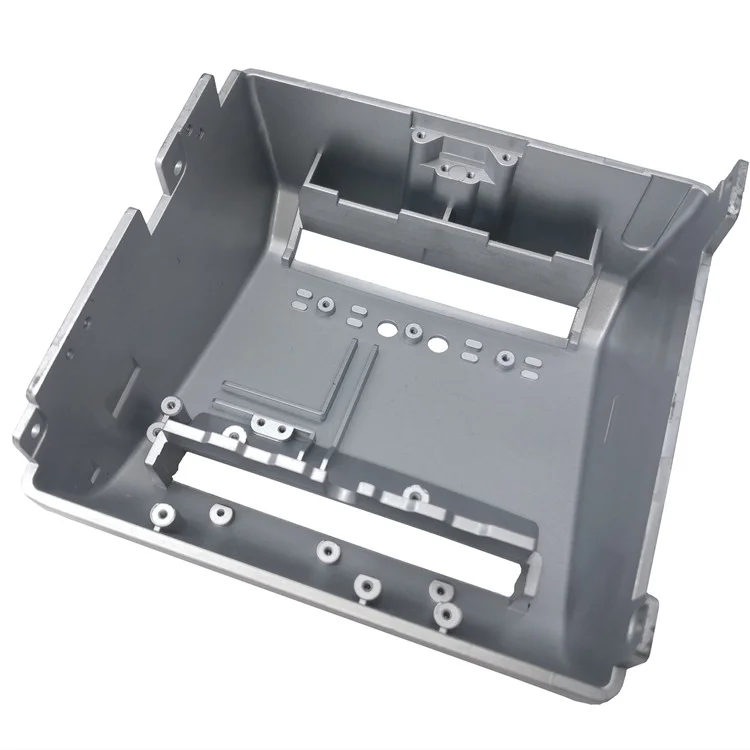
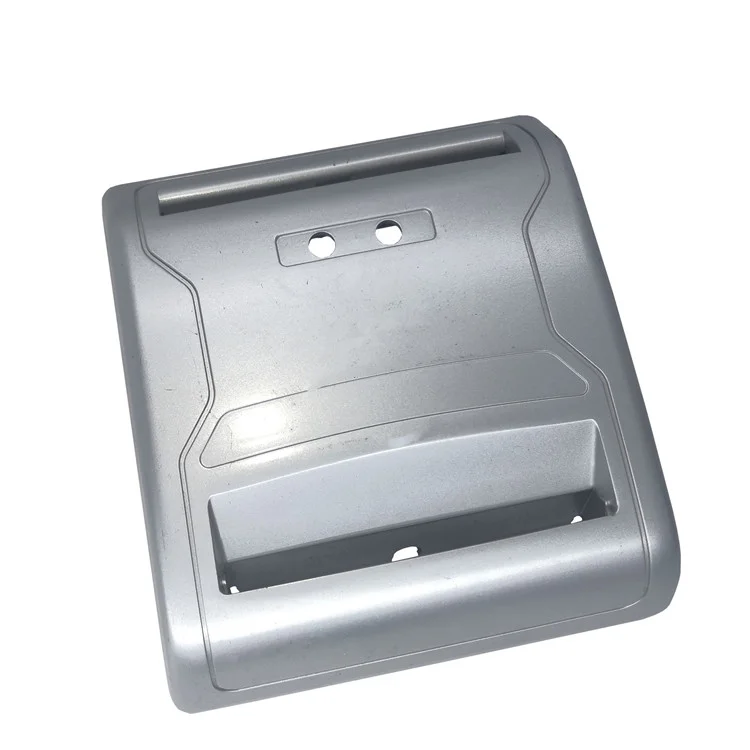
Zinc Alloy Die-Cast ATM Movement-Mouth Housing with CNC Processing and Custom Drawing-Based Dimensions
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Component FormHousing / EnclosureSurface FinishPowder Coated , Polished
-
Surface treatmentPainting/powder coating/electroplate/Anodizing/mirror polishing
-
PortYantian ShenzhenMaterial ScienceZinc alloy Aluminum Alloy ADC12/A380/A383 and magnesium/zinc alloy
-
DRW mode:PDF / DWG / IGS / STP /etctoleranceGB5237.1-2008 High Precision Grade
-
equipment400 tons die casting machine+ CNC Machining CenterDelivery timeAccording to the quantity of the order
-
AuthenticationCE/RoHSpurposechassis shell
-
Size145*119*83mm Or customized machining 2d/3d drawings
The ATM movement-mouth housing is a cast chassis component with CNC processing, offered in a specified size or a drawing-based custom version. Treat the housing as part of the intended ATM mechanism, with its selected material and interfaces defining the component inquiry.
Check the mechanism envelope from the nominal size
The 145*119*83 mm size provides a concrete reference for the housing envelope. Compare that geometry with the intended assembly and identify the dimensions needed at its interfaces. Custom machining from 2D or 3D drawings allows the proposed version to follow the component brief, while the nominal size alone should not establish compatibility with an unspecified ATM.
- Housing reference
- 145*119*83 mm, with drawing-based customization available.
- Component files
- PDF, DWG, IGS or STP drawings for the machining discussion.
Keep the zinc-alloy request distinct from alternatives
Select the zinc alloy needed for the ATM housing. The wider material scope includes ADC12, A380 and A383 aluminum, as well as magnesium/zinc alloys, so identify the alloy required for this particular ATM component. Agree the material and die-casting proposal together before comparing a finished housing with the intended mechanism geometry.
Review CNC and exterior acceptance together
The service combines die-casting equipment with a CNC machining center. Define which areas require CNC processing and how their dimensions are accepted for the housing. For the exterior, discuss mirror polishing or a specified paint, powder-coat, electroplated or anodized treatment, confirming its suitability for the chosen alloy. The GB5237.1-2008 High Precision Grade designation should be applied through an agreed drawing scope. Any required CE/RoHS documentation belongs to the relevant component approval discussion.