
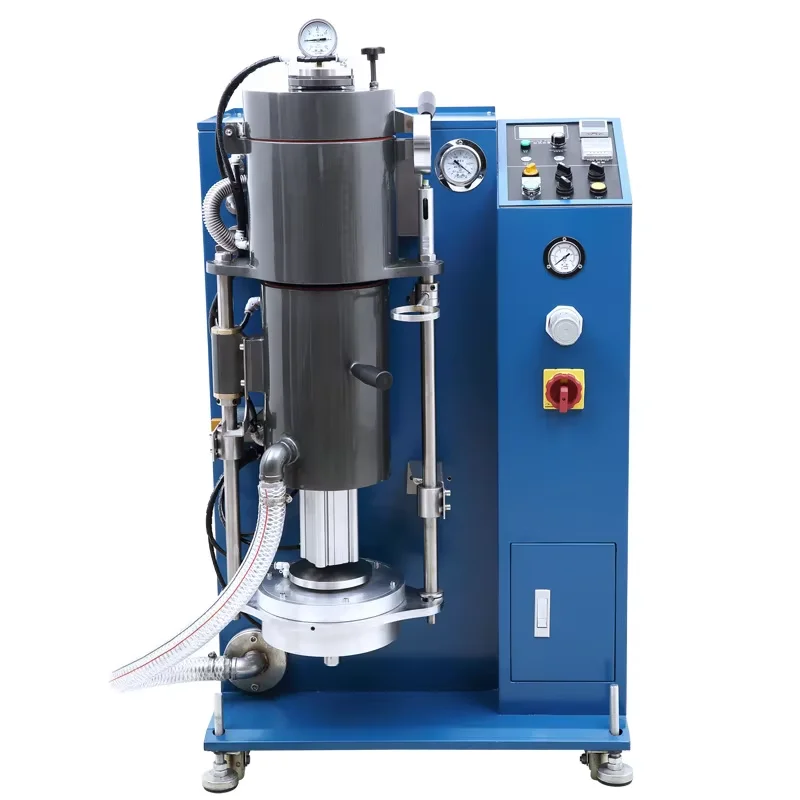
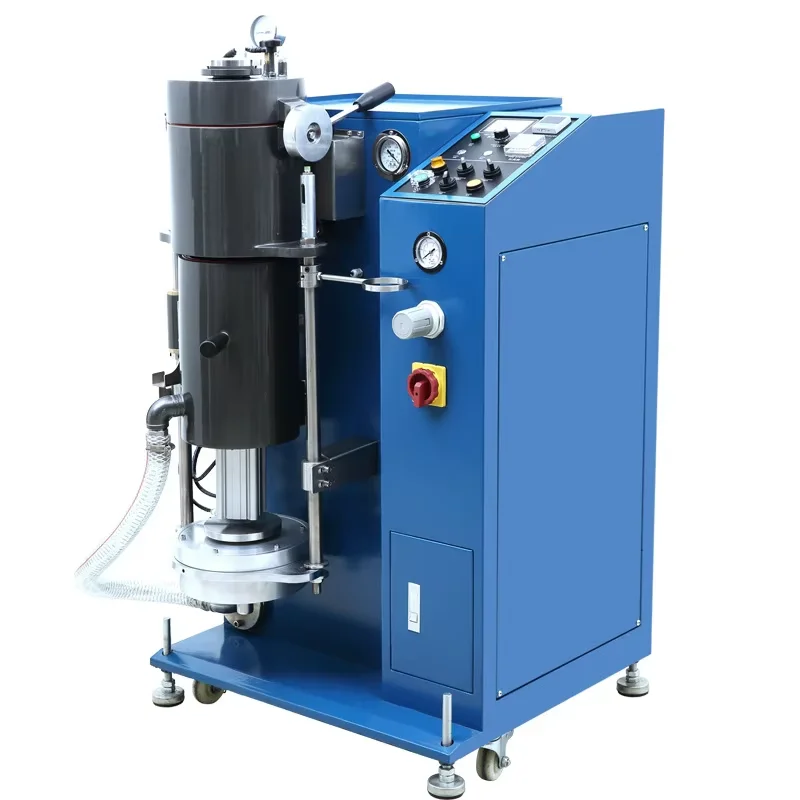
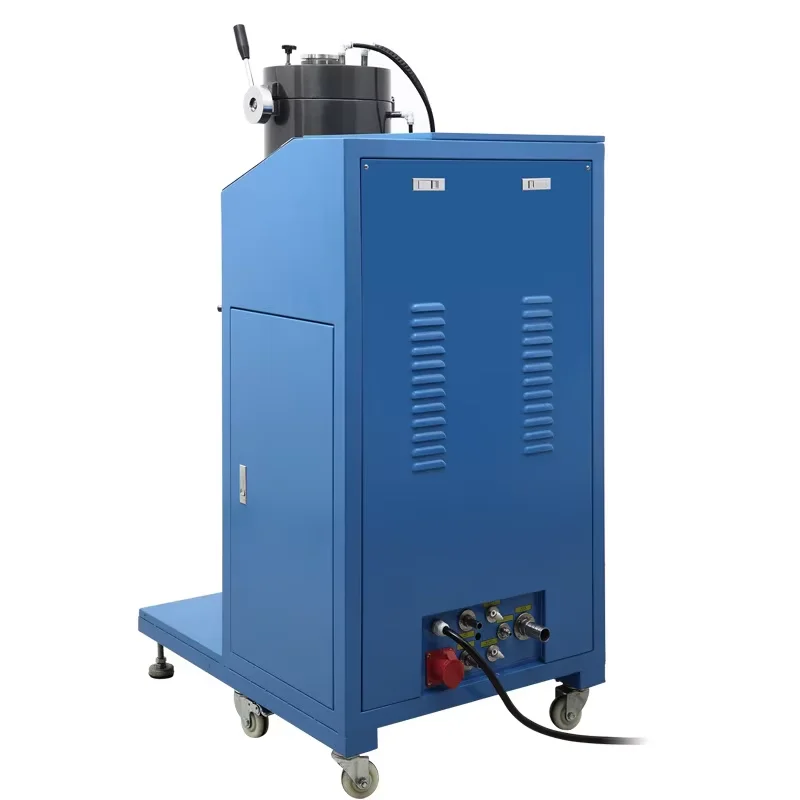
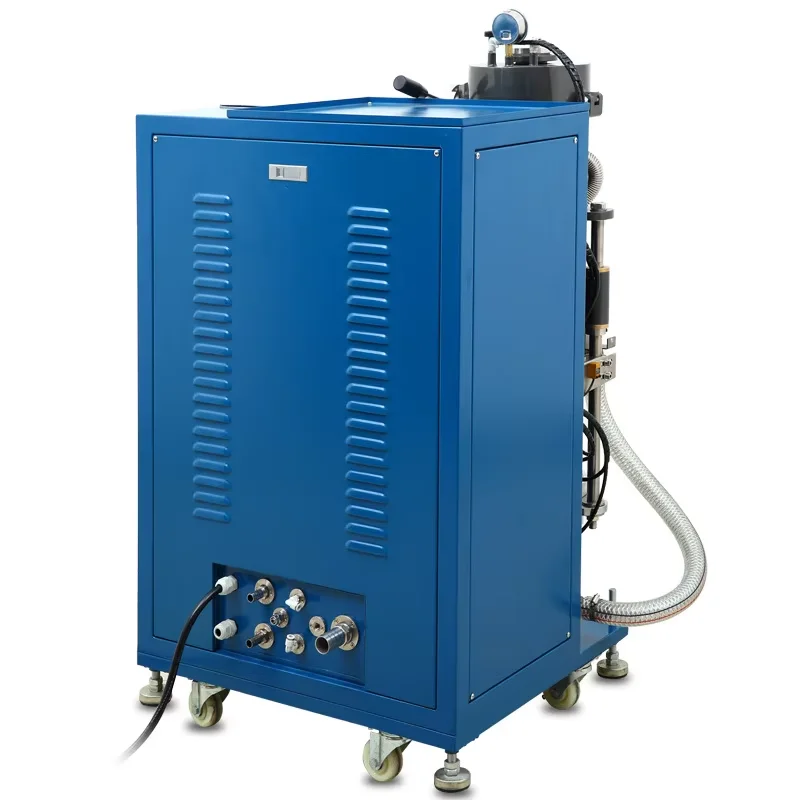
PLC Gold/Silver Jewelry Casting Machine | Precision-Temperature Vacuum/Pressure System, Lost-Wax and Induction Melting
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Equipment Supply Voltage380V
-
machine typevacuum casting machine, jewelry casting machinevideo outgoing-inspectionProvided
-
machinery test reportProvidedcore componentsPLC
-
voltage380v 60hzpower(w)15kw(20.12hp)
-
dimension(l*w*h)720x700x1150mm(28.35x27.56x45.28in)warranty2 Years
-
key selling pointsCompetitive Priceweight (kg)210
-
MaterialMetalMelting Capacity2kg, 1.5kg(18K gold),1kg Silver
-
Max. Vacuum Degree-0.1 MPaMax. Casting Pressure1.5 MPa
-
Temperature Control Accuracy±1°CMax. Working Temperature1600°C
-
Vacuum systemVacuum PumpMelting time3-5 mins
-
Suitable MetalGold, K-gold, Silver, Copper, etc.Protection gasNitrogen/argon selection
-
Cooling typeRunning water / Water chiller (Sold separately)
PLC-controlled vacuum-pressure jewelry equipment is directed to lost-wax casting and induction melting for gold, K-gold, silver and copper. A vacuum pump is part of the system direction. Electrical references are 380 V/60 Hz and 15 kW (20.12 hp), with the actual charge, mold and operating process to select.
Charge capacity and the actual metal
Melting-capacity references are 2kg with its metal/configuration to agree, 1.5kg for 18K gold and 1kg for silver. Select the actual metal and charge together with the mold and intended casting task. The separate metal-specific references should remain connected to that chosen process when defining the equipment's operating acceptance.
Vacuum, casting pressure and temperature control
The maximum vacuum-degree reference is -0.1 MPa and maximum casting pressure 1.5 MPa. Temperature-control accuracy is ±1°C, with a maximum working-temperature reference of 1600°C. Melting time is referenced at 3–5 minutes for the selected charge/process. Agree the actual operating sequence and measurement acceptance for the chosen jewelry work alongside those distinct control values.
Gas choice, cooling provision and installation
Protection-gas selection is nitrogen or argon, while cooling uses running water or a separately supplied water chiller. Define the actual gas/cooling arrangement and electrical installation for the selected configuration. Overall dimensions are 720 × 700 × 1150 mm (28.35 × 27.56 × 45.28 in). Use that envelope with the actual machine and supply arrangement when planning the process installation.
Provided inspection material for the configuration
Outgoing-inspection video and a machinery test report are provided. Relate the requested inspection and operating acceptance to the actual charge, mold, controls and supplies. This supports a configuration-specific jewelry-casting inquiry with the needed melting and finished-casting requirements clearly defined.








