
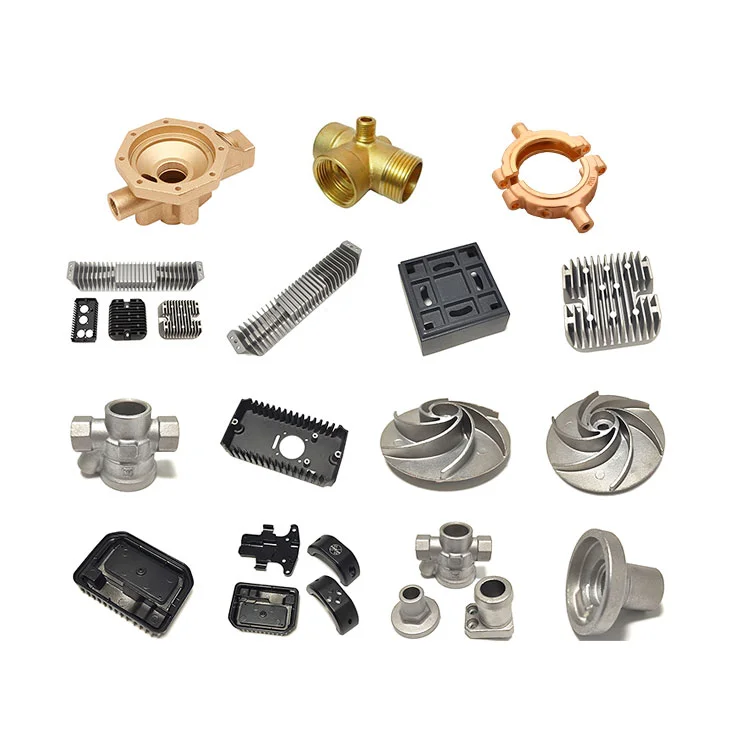
Custom Precision Zinc/Zamak Die and Investment Castings | ±0.02mm and Surface Finishing
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishPainted , Powder Coated
-
Sizecustom
-
Surface TreatmentChorme Plating Powder Coating Painting ElectrophorMaterialsAluminum Alloy
-
ProcessInvestment casting/Lost wax/die castingmaterialCarbon steel/Stainless steel/Aluminum alloys
-
DimensionCustomizedQuality Control100% Inspection
-
ApplicationIndustrial, commercial, Household, Automotive partsTolerance+/- 0.02 mm
-
RoughnessRa3.2-Ra6.3PackageWooden pallet
-
Export experienceMore than 10 yearsMOQ100 Pieces
Custom zinc-alloy and Zamak casting services offer die and investment/lost-wax process directions. Aluminum alloys, carbon steel and stainless steel are additional material choices. Customized dimensions support industrial, commercial, household and automotive components, with ±0.02mm and Ra3.2–Ra6.3 as technical references.
Zinc or another metal for the component
Define the actual zinc/Zamak, aluminum or steel grade and the part geometry. Agree the material-compatible casting route for that combination, keeping the desired dimensions and component role explicit. This gives the die or investment-casting request a specific material and shape to assess.
Four surface-finishing directions
The available finish directions are chrome plating, powder coating, painting and electrophoretic finishing. Choose the treatment around the selected metal and the surfaces that need it. Describe the required appearance and finished condition so the surface request has its own acceptance criteria.
Precision references and the inspection basis
Identify the controlled dimensions and confirm where the ±0.02mm tolerance reference applies in the chosen process. The Ra3.2–Ra6.3 reference should be assigned to the relevant surfaces, with its units and evaluation criteria agreed for the part. Inspection is provided at 100%, with the actual characteristics to be checked defined alongside those requirements.
For a zinc/Zamak casting project, connect the alloy, die or lost-wax route, custom geometry and finish selection. When considering an aluminum or steel alternative, review that material-route pairing and its acceptance requirements as the actual component configuration.








