
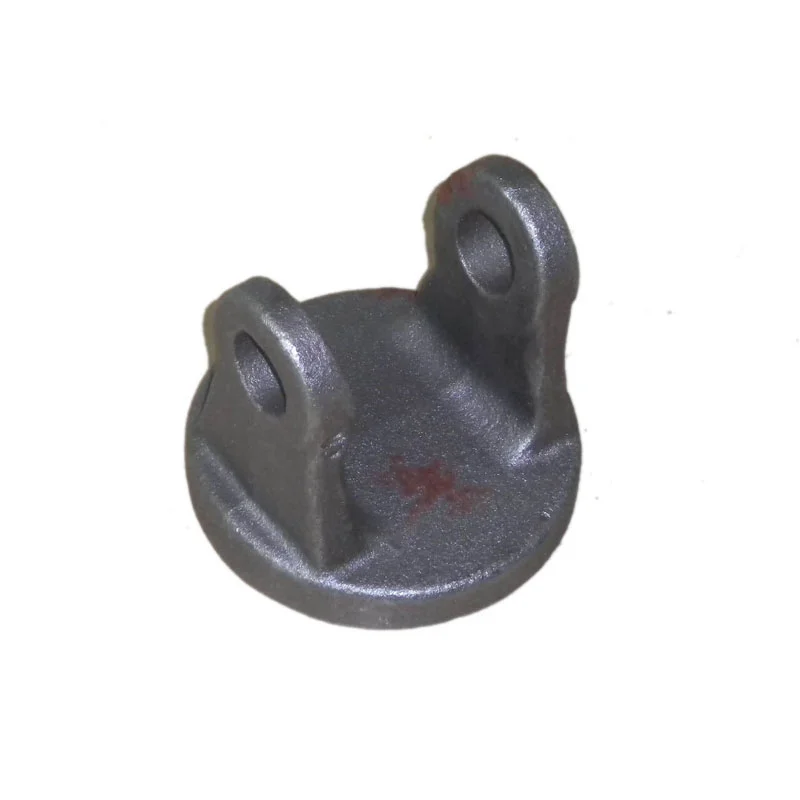
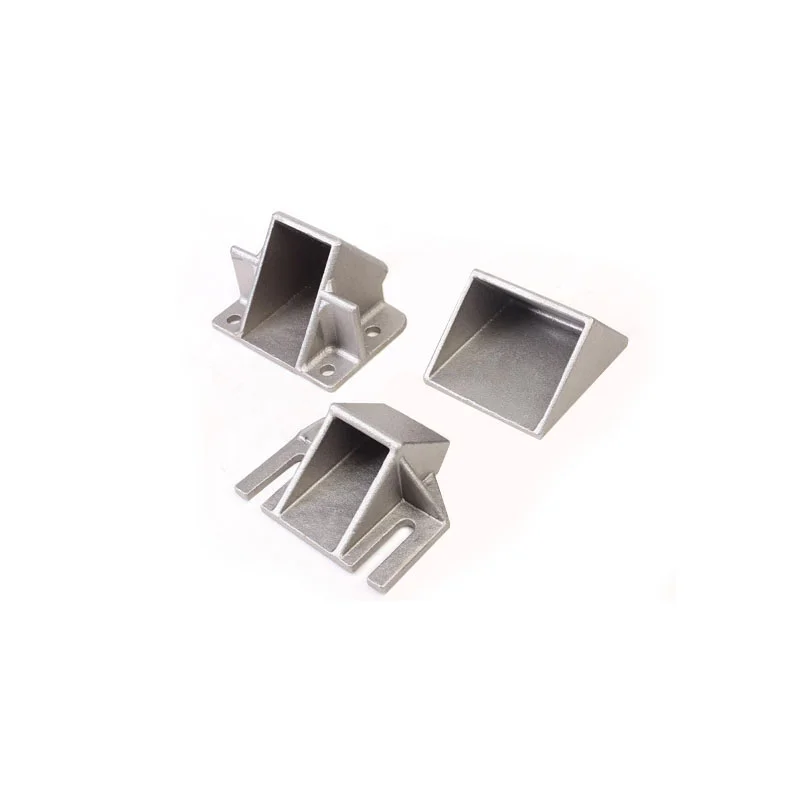
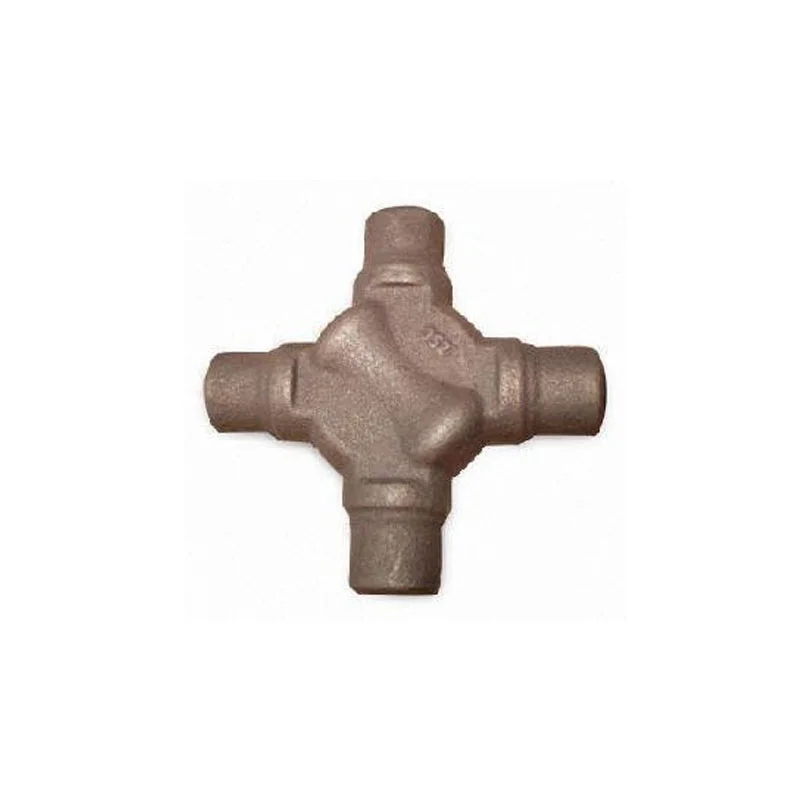
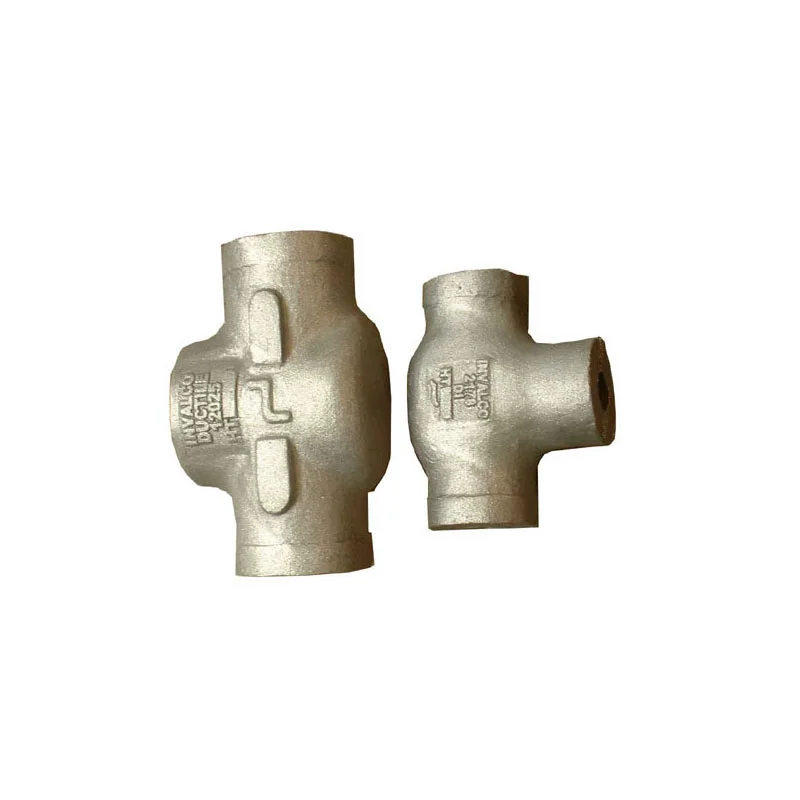
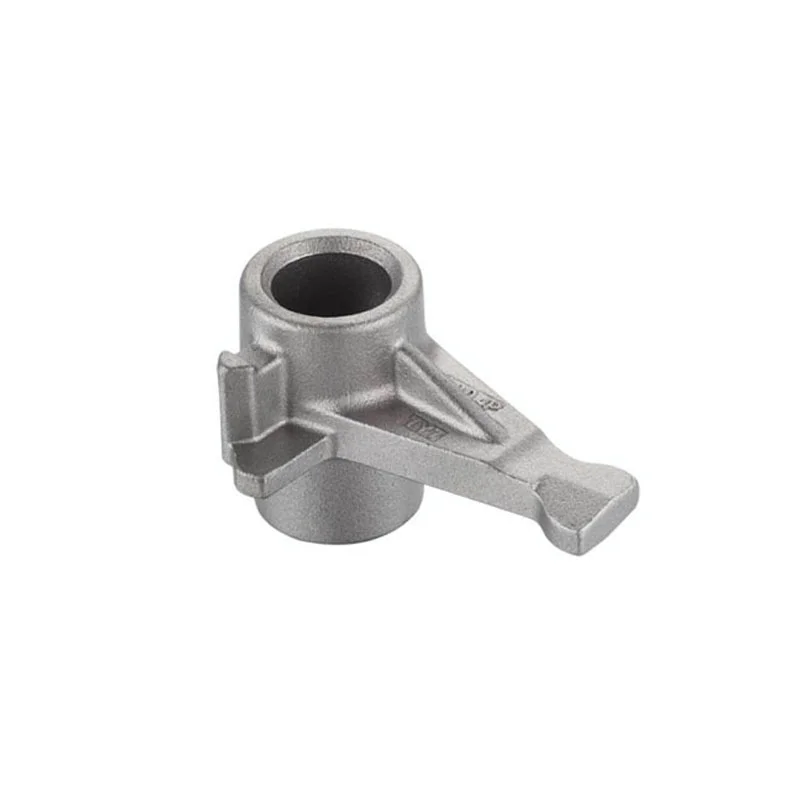
Custom Metal Hardware Investment Castings/CNC Parts, CT4–CT8 Casting and ±0.02mm Machining References with Five Finishes
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishSandblasted , Polished
-
MaterialStainless Steel,Steel,Brass,Copper,Aluminum,Iron,Plastic
-
TechnologyInvestment Casting,Sand Casting,Machining,Welding,ForgingMachiningBroaching,DRILLING,Milling,Turning,Tapping,Wire
-
ProcessMolds,Casting,Deburring,Machining,Surface Treatment,PackingWeightAvailable from 0.01 Kg-10T
-
StandardISO,GB,DIN,JIS,ANSI,BSW,ASTM,ASME,BS,API,ENCasting ToleranceCT4-CT8
-
Machining Tolerance+/-0.02mmSurface TreatmentPolishing, Passivating, Sandblasting, Zinc plating, Oxide black
-
CertificationIS09001: 2015,TUV
Custom precision metal-hardware fabrication includes investment casting and CNC machining, with CT4–CT8 casting and ±0.02mm machining references. Select the actual supplied material and hardware component before assigning these limits. Mold work, casting, deburring, machining and surface treatment are process directions to allocate within the selected work.
Hardware material and the chosen manufacturing route
Part-work material directions include stainless steel, steel, brass, copper, aluminum, iron and plastic. Define the actual supplied specification and geometry, then allocate investment casting, sand casting, machining, welding or forging as appropriate. Relate the selected route to the hardware's interfaces and required final condition.
Cast dimensions and CNC-finished hardware locations
Identify the cast dimensions covered by the selected casting grade and the machined locations requiring controlled limits. Broaching, drilling, milling, turning and tapping are available directions alongside CNC work. Clarify the exact Wire operation where requested. Set the actual feature, datum and measurement conditions represented by ±0.02mm, connecting the result to the hardware's mating requirements.
Five finish choices and the hardware acceptance documents
Finishes include polishing, passivating, sandblasting, zinc plating and black oxide, with actual treated areas and acceptance to agree. Identify the relevant ISO, GB, DIN, JIS, ANSI, BSW, ASTM, ASME, BS, API and EN documents and editions for the selected component. Clarify the exact IS09001: 2015 and TUV references and their current document/object/site scope where required. Agree inspected characteristics, methods and records for the hardware's dimensions, surface and working duty. Confirm quantity and manufacturing responsibility with those accepted drawing requirements.








