
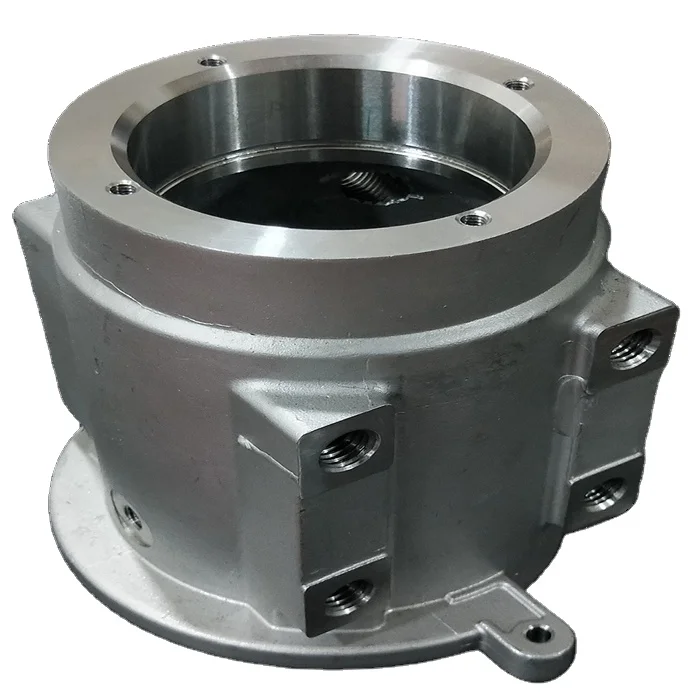
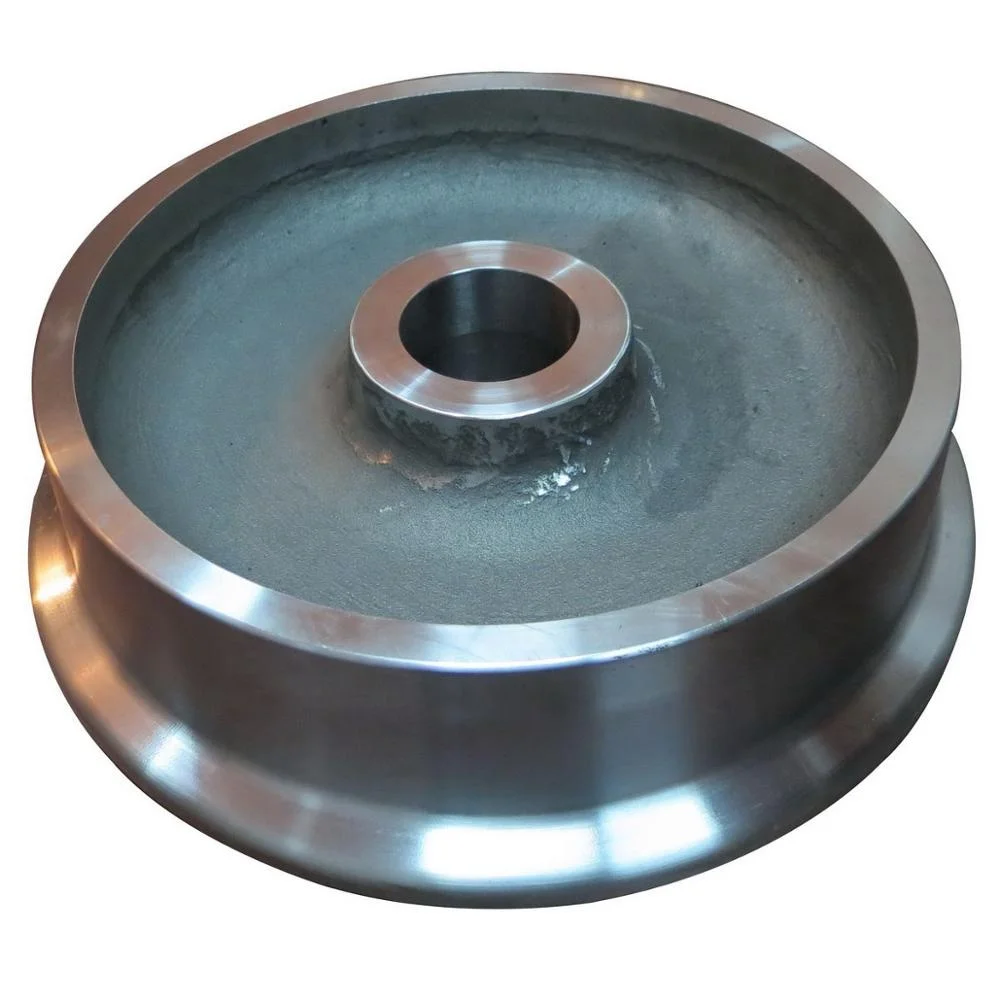
Custom Investment Casting Foundry Service for Machinery Parts with CNC Machining and Heat Treatment
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
Surface FinishShot Blasted
-
NameCustomized manufacturer investment casting foundry
-
Keywordsinvestment castingAppplicationmachinery
-
ProcessLost wax investment casting+CNC machinedHeat TreatmentQuench and temper by 2 set mesh belt furnaces
-
Surface TreatmentShot blasting+AssemblingMachining Facility50+ Machining centers,80+ CNC machines
-
InspectionMT/UT/RT/100% visual+100%gage/CMMStandardASTM. AISI. DIN. BS. JIS. NF. AS.
-
CertificationIATF16949/ISO14001
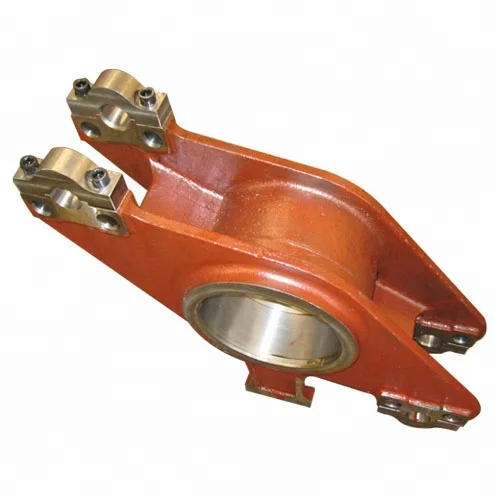
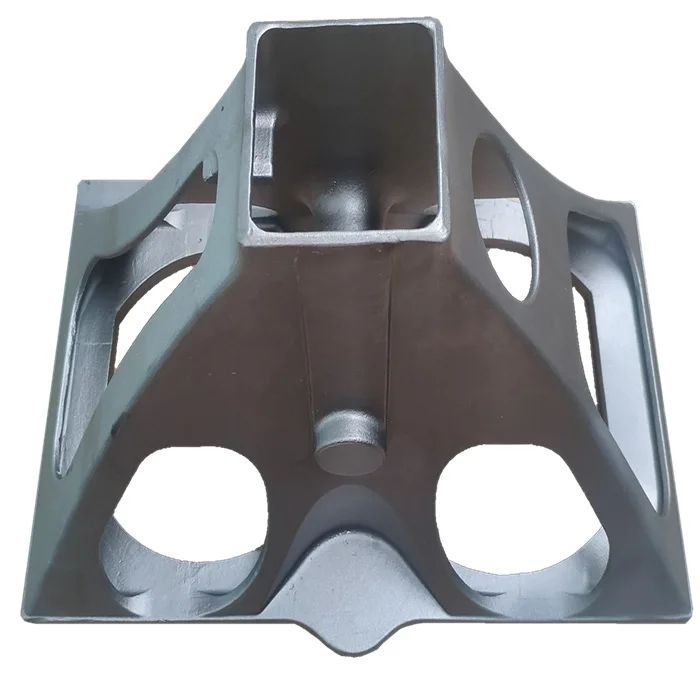
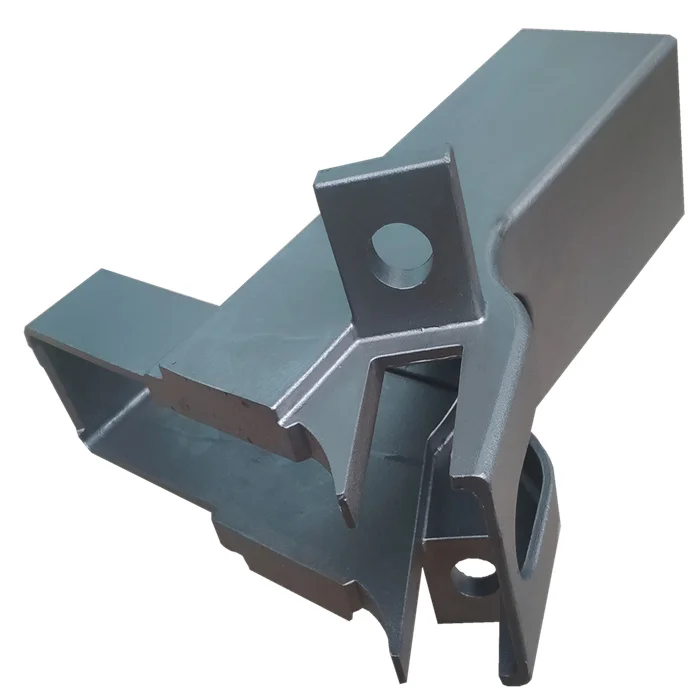
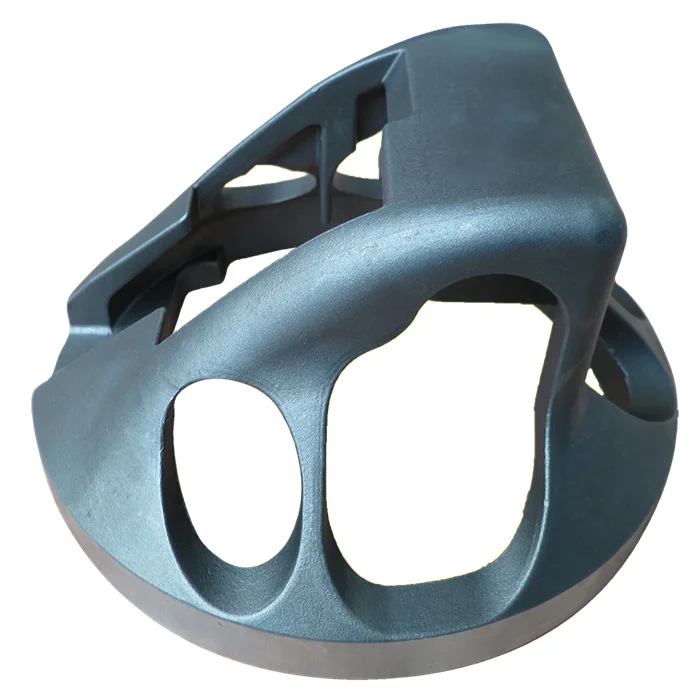
Custom machinery casting work can combine lost wax investment casting, CNC machining, heat treatment and assembly in the project proposal. The material and component drawing establish how those operations should be specified, with shot blasting and inspection addressed alongside the required finished condition.
Specify material before the heat-treatment proposal
State the material grade and the condition needed for the machinery component before selecting the heat-treatment requirements. Quenching and tempering is supported by two mesh belt furnaces, with the required outcome to be agreed for the actual part. Define the relevant material or hardness acceptance so the process review has a measurable objective.
Plan CNC work from the cast geometry
The machining resources include 50+ machining centers and 80+ CNC machines. Identify the dimensions and interfaces requiring CNC work after casting, including the drawing references used to accept the finished component. Connect those machining requirements to the approved casting geometry and any assembly interfaces that the part must meet.
Assign inspection methods to component checks
Visual and gage inspection each have 100% coverage commitments, alongside MT, UT, RT and CMM capability. Specify which characteristics require each method and agree the corresponding coverage and acceptance records. This allows dimensional, visual and other required checks to be reviewed against the relevant casting or finished feature.
Set the finish, assembly and documentation scope
Shot blasting and assembly should be defined by the treated surfaces and the parts or interfaces included in the supplied scope. Where ASTM, AISI, DIN, BS, JIS, NF or AS requirements apply, provide the exact designation and revision for the component. Orders requiring IATF16949 or ISO14001 documentation should also confirm current certificate holder, validity and covered activities before approval.








