
Custom Aluminum Investment/Lost Wax and Die Casting Enquiries | ±0.02mm and Ra3.2–Ra6.3 References
Let’s define your requirement
Send a product link, drawing or short brief. We’ll work through the details with you.
- Confirm the specificationGrade or model, size and intended use.
- Define your orderQuantity, finish or configuration, and samples.
- Agree the quotation scopeIncluded work, key checks and delivery needs.
-
ProcessInvestment casting/Lost wax
-
MaterialAluminum,stainless steel,carbon steelDimensionCustomized
-
Quality Control100% inspectionApplicationIndustrial, commercial, Household, Automotive parts
-
Tolerance+/- 0.02 mmRoughnessra3.2-ra6.3
-
PackageWooden palletExport experienceMore than 10 years
-
MOQ10 Pieces
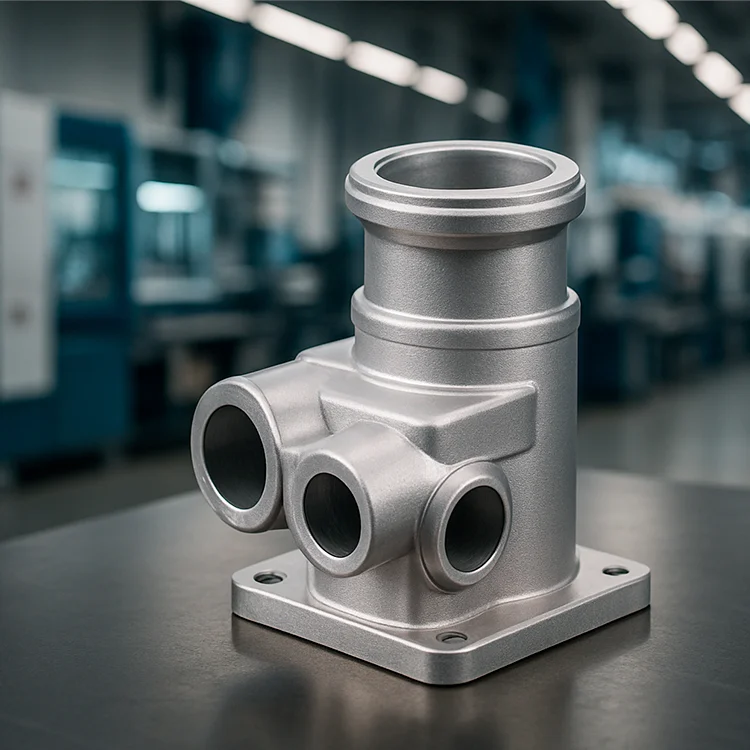
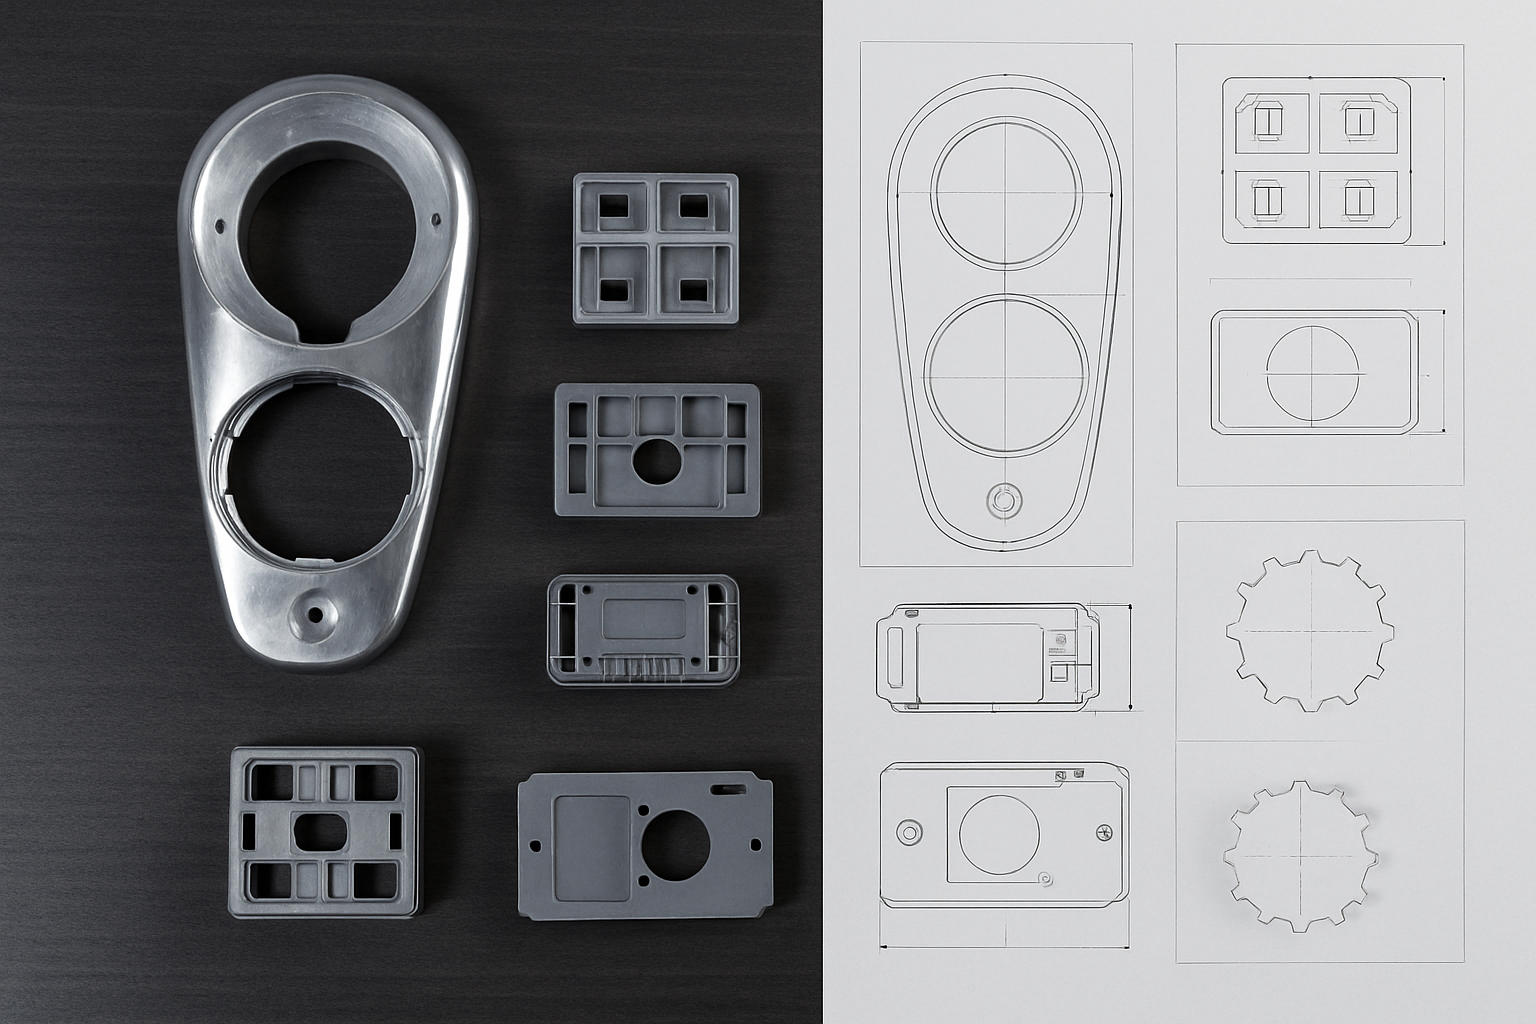
Custom aluminum casting enquiries include investment and lost-wax directions alongside die-casting requests. Stainless steel and carbon steel are further material directions. Choose the actual grade and casting route for the component, then define the customized dimensions and accepted finished result.
Component drawing and intended application
Industrial, commercial, household and automotive parts are named application directions. Identify the actual component and the working conditions it must meet. Define the geometry and dimensions controlled by the drawing. Agree which manufacturing route applies to that material and use.
Tolerance and roughness requirements
The tolerance reference is +/-0.02mm, with roughness at Ra3.2–Ra6.3. Agree the dimensions and manufacturing stage covered by the tolerance. Confirm the roughness unit and identify the surfaces requiring the selected condition. Define the measurement and acceptance criteria for the actual component geometry.
Inspection of the selected result
The quality-control direction is 100% inspection. Agree the characteristics to be inspected and the criteria used to accept the casting.
- Dimensional request
- Identify the grade, drawing revision, selected route and covered dimensions for the customized part.
- Surface and inspection request
- Define the required roughness scope and accepted surface result. Bring those requirements together with the working conditions and inspection criteria for the actual enquiry.








